
Green sand casting mold and casting production process
A casting mold, casting production technology, applied in the field of brake pad preparation equipment, can solve the problems of brake pad casting production only in small batches, high cost, low yield, etc., to achieve product structure and quality requirements, realize automation, Solve the effect of inability to form and product shrinkage
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2021-10-26
Smart Images
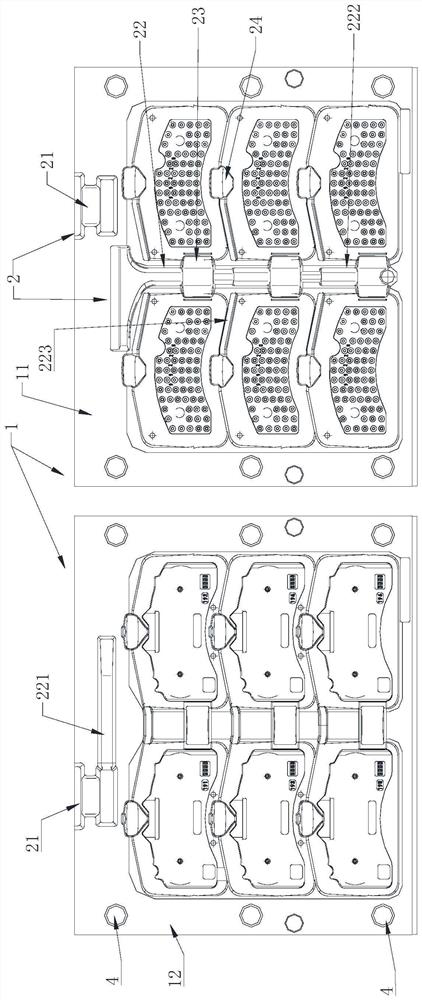
Figure 1 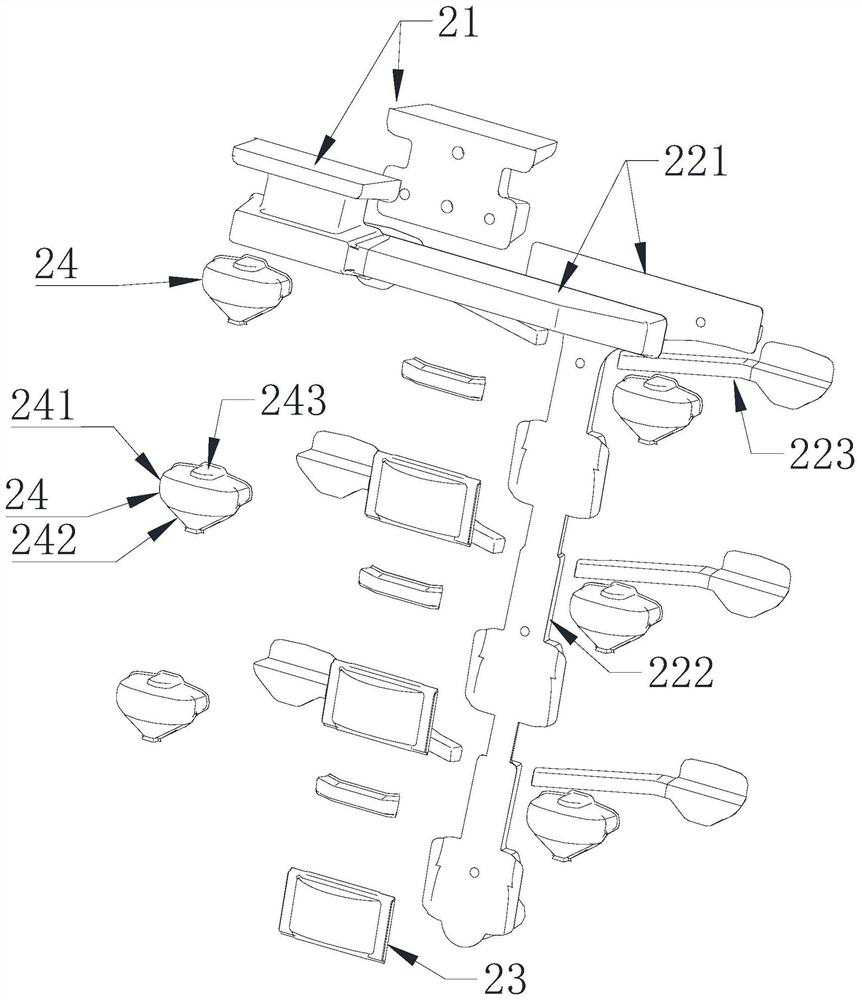
Figure 2 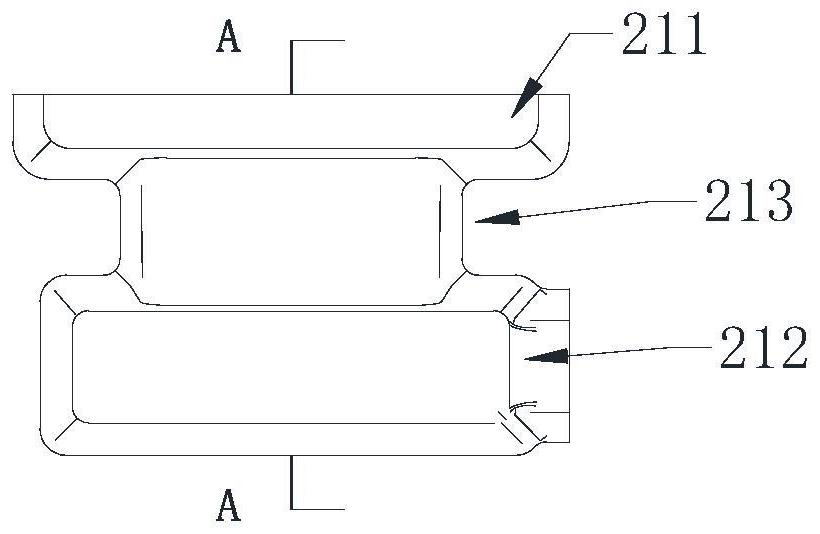
Figure 3
Abstract
Description
technical field
[0001] The invention relates to the technical field of brake pad preparation equipment, in particular to a green sand casting mold and a casting production process. Background technique
[0002] In the braking system of a car, the brake pads are the key safety parts. The effect of the braking system is largely determined by the brake pads, so good brake pads are the protectors of people and cars. Pads need to be guaranteed by advanced manufacturing technology, so the manufacturing technology of brake pads is very important.
[0003] The applicant finds that the prior art has at least the following technical problems:
[0004] At present, in the field of precision casting technology, there is no good production technology to realize large-scale mass production of brake pad casting, which can only be produced in small batches, and the production efficiency is low; and in the existing brake pad casting production, due to the special structure of brake pads The...
Examples
Embodiment 1
[0083] The invention provides a green sand casting mold required in the brake pad preparation process, which mainly includes a mold plate 1, a pouring system 2, a guide column 4, and a mold core 3: the mold plate 1 includes a positive pressure plate 11 and Counter pressure plate 12; gating system 2, including sprue cup 21, runner 22, ingate 23 and riser 24, furthermore, sprue cup 21 is designed as a square of 67x90x103mm, the reason why it is large up and down, narrow in the middle, This is because the molten iron enters more smoothly and will not splash back; the main body of the vertical runner 222 in the runner 22 is divided into three sections, the bottom of each section is provided with an ingate 23, and the top is provided with a constriction. The internal cross-sections are isosceles trapezoidal structures of 15x30x30mm, 12.5x25x25mm and 10x20x20mm respectively, and the ingate 23 is a rectangle with a cross-sectional area of 4x40mm;
[0084] The guide column 4, includ...
Embodiment 2
[0094] The invention provides a green sand casting mold required in the brake pad preparation process, which mainly includes a mold plate 1, a pouring system 2, a guide column 4, and a mold core 3: the mold plate 1 includes a positive pressure plate 11 and Counter pressure plate 12; pouring system 2, including sprue cup 21, runner 22, ingate 23 and riser 24, further, sprue cup 21 is designed as light-duty anti-splash No. 3; The main body of the runner 222 is divided into three sections. The bottom of each section is provided with an ingate 23, and the top is provided with a constriction. A rectangle with an area of 4x40mm;
[0095] The guide column 4, including the chamfering part and the column body part, is designed to be 12 pieces in total, and is installed on the mold plate 1. Furthermore, the chamfering part is designed to be 45°, and the height is 3mm. The design diameter of the column body part is 30mm, and the height is 80mm , a total of 12 pieces are designed, whic...