
Welding method for 12Cr1MoV and 07Cr19Ni 11Ti dissimilar steel
A technology of 07cr19ni11ti and welding method, which is applied in welding equipment, welding/welding/cutting items, arc welding equipment, etc., can solve the problems of reducing the reliability of welding structure and damage of fusion zone, so as to ensure the quality of installation welding and reduce the line energy , Accurately define the effect of welding steps
Patent Information
- Authority / Receiving Office
- CN · China
- Current Assignee / Owner
- Publication Date
- 2022-01-04
Smart Images
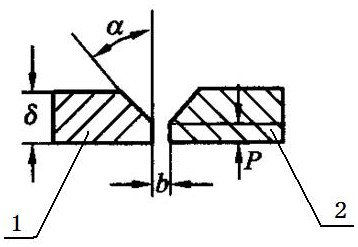
Figure 1 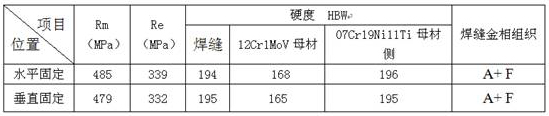
Figure 2
Abstract
Description
technical field
[0001] The invention relates to the field of welding technology, in particular to a welding method for 12Cr1MoV and 07Cr19Ni11Ti dissimilar steels. Background technique
[0002] It is austenitic stainless steel, 12Cr1MoV belongs to pearlitic steel, and the welded joint of 07Cr19Ni11Ti and 12Cr1MoV steel belongs to the welded joint of dissimilar steel, that is, the welding of austenitic and pearlitic steel. In addition, the difference in physical properties is large, and large-area welding defects are prone to occur. In many literatures, Inconel 82 (ERCrNi-3) welding wire is mostly used for welding austenitic and pearlitic steels, and the cost is high. It is not suitable for mass production, and the problems existing in the welding of 07Cr19Ni11Ti and 12Cr1MoV in the prior art:
[0003] (1) The dilution effect of the pearlitic steel base metal on the weld and the formation of the M transition layer in the fusion zone: 12Cr1MoV steel has a dilution effect on t...
Examples
Embodiment 1
[0029] A kind of 12Cr1MoV and 07Cr19Ni11Ti, its composition comprises: dissimilar steel A, dissimilar steel B, the matching gap b between the dissimilar steel A and the dissimilar steel B is 2.0-3.0mm, and the groove angle α is 30°-35° , the blunt edge Р is 1.5-2.0mm, the pipe thickness δ is 5mm, the welding wire is TGS-347 welding wire, the diameter of the welding wire is 2.4mm, the welding is assembled in a free state, and manual tungsten argon arc welding is used. Wire welding method, when the argon gas inside the pipeline is filled and stable, the root layer welding is performed, and the temperature between each layer is controlled to ≯350°C;
[0030] The welding method comprises the following steps: firstly, machining the grooves on the base metal side of dissimilar steel A and dissimilar steel B, and cleaning the groove surface and the outer walls within 10 mm on both sides of the base metal, i.e. oil, paint, rust, and dirt are cleaned until give off a metallic luster; ...