
Production method for high-performance special-shaped iron-cobalt soft magnetic alloy parts
A soft magnetic alloy, high-performance technology, applied in the direction of magnetic materials, magnetic objects, electrical components, etc., can solve the problems that affect the sintering performance and magnetic properties of materials, high saturation magnetic induction, low output rate of alloy powder, etc., and achieve improvement Microstructural structure, reduced manufacturing cost, and improved sintering activity
Patent Information
- Authority / Receiving Office
- CN · China
- Current Assignee / Owner
- Publication Date
- 2015-08-19
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
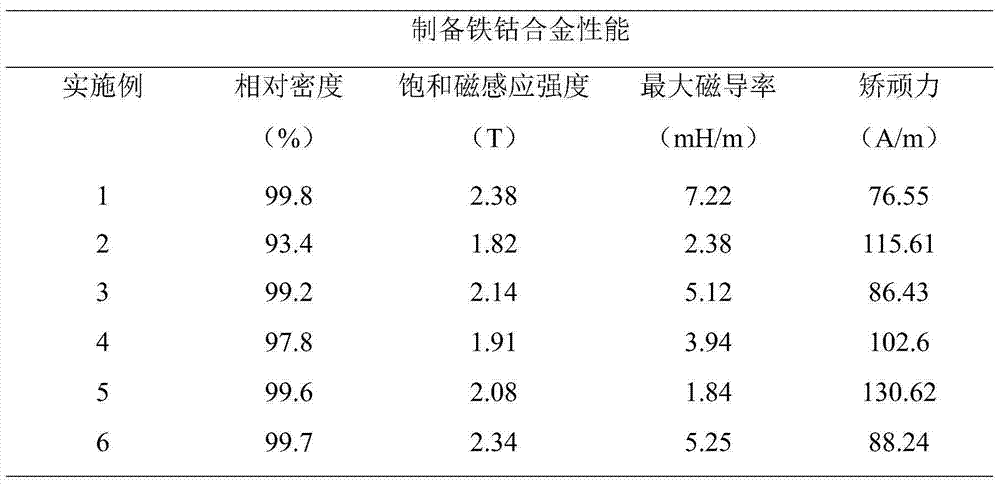
Figure 1
Abstract
Description
technical field
[0001] The invention belongs to the field of magnetic materials, and in particular provides a method for preparing high-performance special-shaped iron-cobalt series soft magnetic alloy parts. Background technique
[0002] Among metal soft magnetic materials, iron-cobalt soft magnetic alloys have extremely high saturation magnetic induction intensity Bs (2.4T), the largest magnetostriction coefficient λs (70~80╳10 -6 ) and the highest Curie temperature (980 ~ 1100 ℃), so it can be used as a ferromagnetic element that requires high Bs, high λs, low frequency and high temperature, and is suitable for making micro Special motors, electromagnet poles, relays, force rejecting motor rotors, power transformers, magnetostrictive transducer cores, etc. With the development of magnetic circuit components towards miniaturization and multi-function, the size of the soft magnetic alloy parts used is getting smaller and smaller, and the shape is more and more complex. Du...
Examples
Embodiment 1
[0019] Carbonyl iron powder, reduced cobalt powder, and vanadium iron powder are used as raw materials, and the ratio of iron: cobalt: vanadium is 49:49:2 by weight, and ball milled in a planetary ball mill for 20 hours under an argon atmosphere. It is 10:1. Select microcrystalline wax, high-density polyethylene, polypropylene and stearic acid as the forming agent, and by weight percentage microcrystalline wax: high-density polyethylene: polypropylene: stearic acid is 60:25:10:5 ingredients, each The organic substances were mixed for 2 hours at a temperature of 150° C. in a molten state. Ball mill powder and forming agent are kneaded in a kneader at 150°C for 3 hours at a volume ratio of powder to forming agent of 52:48. The mixture of powder and binder is formed on an injection molding machine, and injected into a mold under the conditions of a temperature of 160°C and an injection pressure of 100 MPa. After soaking the formed body in n-heptane at 20°C for 4 hours, the gree...
Embodiment 2
[0021] Using the same raw material powder and material composition ratio as in Example 1, various raw material powders will be mixed in a V-shaped mixer for 12 hours, and the raw material powders will not be processed by high-energy ball milling. Forming and degreasing process, after sintering at 1400°C for 3 hours, the magnetic properties of the material are tested directly, without hot isostatic pressing and subsequent heat treatment of the powder. The properties of the prepared soft magnetic material: the relative density is 93.4%, the saturation magnetic induction is 1.82T, the maximum magnetic permeability is 2.38mH / m, and the coercive force is 115.61A / m.
Embodiment 3
[0023] Using the same raw material powder and material composition ratio as in Example 1, various raw material powders will be mixed in a V-shaped mixer for 12 hours, and the raw material powder is not processed by high-energy ball milling. Others adopt the same molding as in Example 1, Sintering, hot isostatic pressing and heat treatment processes. The properties of the prepared soft magnetic material: the relative density is 99.2%, the saturation magnetic induction is 2.14T, the maximum magnetic permeability is 5.12mH / m, and the coercive force is 86.43A / m.