
High-carbon low-ferrite-content austenitic stainless steel plate and production method thereof
An austenitic stainless steel and production method technology, applied in the field of iron and steel materials, can solve the problems of high ferrite content, poor intergranular corrosion resistance, and increased production costs, and achieve good comprehensive performance, good mechanical properties, and optimized distribution Effect
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2021-10-26
Smart Images
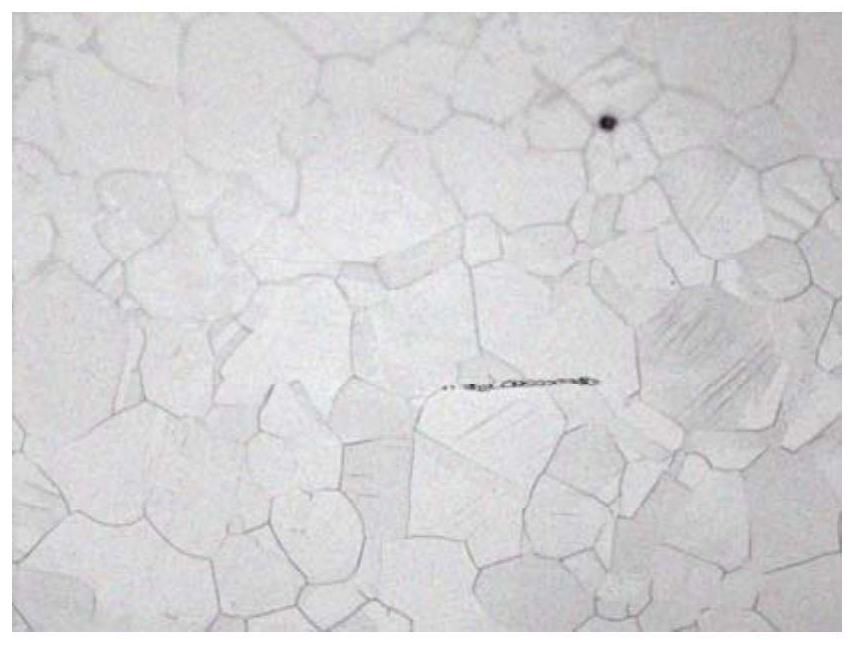
Figure 1 
Figure 2 
Figure 3
Abstract
Description
technical field
[0001] The invention belongs to the field of iron and steel materials, and in particular relates to a high-carbon low-ferrite content austenitic stainless steel plate and a production method thereof. Background technique
[0002] For 300 series austenitic stainless steel, in order to improve its resistance to high temperature stress corrosion between crystals, it is used in the production of key equipment for nuclear power. On the basis of adding a certain amount of Cr and Ni elements, a certain amount of Mo must be added to the steel. Elements, compared with other austenitic stainless steels, it is easier to form high-temperature δ-ferrite, and for medium and thick plates, due to the difference in cooling rate during the solidification of molten steel, serious segregation of Cr and Mo elements will occur, and more Conducive to the formation of high temperature δ-ferrite. In addition, the high-temperature δ-ferrite is very easy to gather in the loose center ...
Examples
Embodiment Construction
[0057] Below by embodiment the present invention will be further described.
[0058] In the embodiment of the present invention, according to the component ratio of the technical solution, electroslag remelting, heating, forging, homogenization heat treatment, rolling, and grain boundary engineering control are carried out;
[0059] (1) Electroslag remelting:
[0060] a) In the slag removal stage, the arc is automatically started, and the power supply parameter current and voltage are gradually increased from 6000-7000A, 74V to 16000-17000A, 86V, and the slag removal time is 105-115min; after that, enter the current and voltage raising stage, and the power supply parameters The current and voltage continue to increase step by step to 25000-26000A, 101V;
[0061] b) Remelting stage: the target melting speed is 1100kg / h~1300kg / h, the remelting time is 15~20 hours, and the power supply parameters current and voltage are gradually reduced from 25000-26000A and 101V to 19000-20000...