
Surface nanocrystallization manufacture method for improving oxidation resistance performance of heat resistant steel
An anti-oxidation, nano-technology, applied in the field of surface nano-ization, can solve the problems of unsatisfactory anti-oxidation performance, influence of workpiece size, accelerated material oxidation, etc. small damage effect
Patent Information
- Authority / Receiving Office
- CN · China
- Current Assignee / Owner
- Publication Date
- 2015-07-08
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
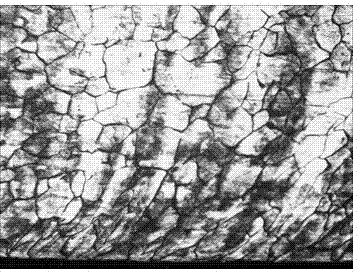
Figure 1 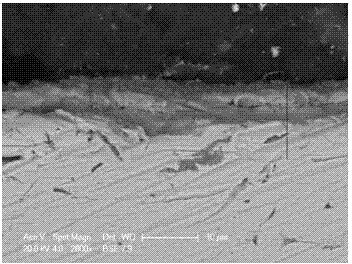
Figure 2 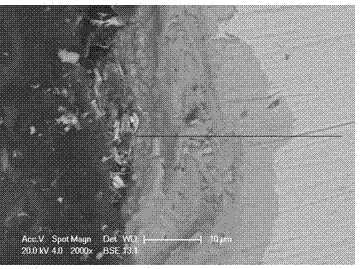
Figure 3
Abstract
Description
technical field
[0001] The invention relates to a surface nanometerization method, in particular to a method for improving the anti-oxidation performance of superheater and reheater steel pipes of super (super) critical boilers under high-temperature steam conditions. Background technique
[0002] At present, among the reasons for the failure of the high-temperature heating surface (superheater, reheater) tubes of ultra (super) critical units, the corrosion of the outer wall and the oxidation of water vapor on the inner wall occupy an important position, and they are also one of the essential causes of boiler explosion and leakage accidents. Austenitic heat-resistant steel is currently the material widely used in high-temperature heating surfaces (superheaters and reheaters) of super (super) critical units. Unplanned outages. Many properties of engineering metal materials, such as fatigue, corrosion and oxidation, are extremely sensitive to the surface structure and propert...
Examples
Embodiment 1
[0027] Provided is a preparation method for improving the oxidation resistance of heat-resistant steel by surface nanometerization:
[0028] refer to Image 6 , using a four-column spinning machine to transmit pressure through hydraulic oil. The material of the rolling indenter is GCr15, the sample to be processed is a high-chromium austenitic heat-resistant steel Super304H, the grinding pressure is 10MPa, the size of the grinding sample is 60*60mm, the grinding time is 30min, and the grinding speed is 2rpm.
[0029] Before the surface is mechanically ground, the cylinder body on the pressure plate 3 is first cleaned and inspected, and then installed on the pressure plate 3 . Set the process parameters such as the speed of the final shaft of the four-column spinning machine, conduct trial grinding on the sample, and determine that the grinding position is in the middle of the plate. The plate was ground from No. 200 to No. 3000 with sandpaper, and then polished to a mirror s...
Embodiment 2
[0036] Provided is a preparation method for improving the oxidation resistance of heat-resistant steel by surface nanometerization:
[0037] refer to Image 6 , using a four-column spinning machine to transmit pressure through hydraulic oil. The material of the rolling indenter is GCr15, the sample to be processed is a high-chromium austenitic heat-resistant steel Super304H, the grinding pressure is 8MPa, the size of the grinding sample is 60*60mm, the grinding time is 30min, and the grinding speed is 2rpm.
[0038]Before the surface is mechanically ground, the roller cylinder on the pressure plate 3 is first cleaned and inspected, and installed on the pressure plate 3. Set the process parameters such as the final shaft speed of the four-column spinning machine, conduct trial grinding on the sample, and make sure that the grinding position is in the middle of the plate. The plate is polished from No. 200 to No. 3000 with sandpaper, and then polished to a mirror surface. The ...