
Acidic-corrosion-resistant X65MS pipeline steel and preparation method thereof
A pipeline steel, acid-resistant technology, applied in the direction of manufacturing tools, metal rolling, heat treatment equipment, etc., can solve the problems of high Mn content in pipeline steel, affecting the HIC performance of pipeline steel, and high cost
Patent Information
- Authority / Receiving Office
- CN · China
- Current Assignee / Owner
- Publication Date
- 2018-07-10
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
Figure 1 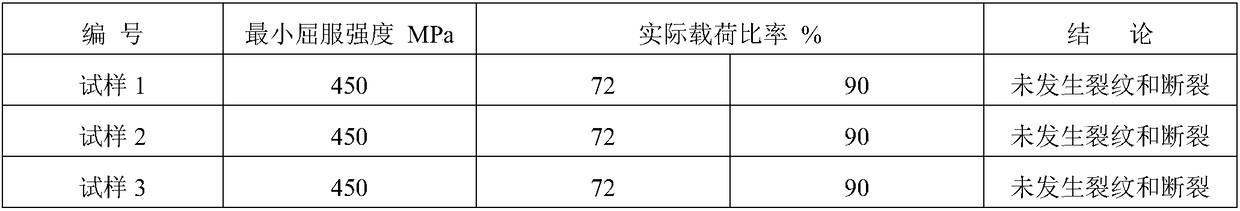
Figure 2
Abstract
Description
technical field
[0001] The invention relates to the technical field of iron and steel metallurgy, in particular to an acid corrosion-resistant X65MS pipeline steel and a preparation method thereof. Background technique
[0002] Oil and natural gas is an important strategy and reserve material of the national economy. With the rapid development of the national economy, the demand for energy such as oil and natural gas is increasing. The continuous growth of energy demand, structural adjustment and optimization have driven the oil and gas industry. comprehensive development. Pipeline transportation is an economical, safe and uninterrupted transportation method, which has the advantages of large transportation volume, low cost, high safety, convenience and high efficiency. In order to meet future oil and gas demand, H 2 Compared with the past, the development quantity of S oil and gas fields has increased greatly, and at the same time, the demand for pipeline steel for sour s...
Examples
Embodiment 1
[0081] Embodiment 1, preparation of acid corrosion resistant X65MS pipeline steel
[0082] Adopt KR method to desulfurize molten iron and high-quality steel scrap, LF refining and RH vacuum treatment to ensure the cleanliness of molten steel, LF refining uses a large amount of slag to make slag, RH vacuum treatment ensures the deep vacuum cycle time of molten steel, calcium treatment after vacuum treatment, Ar gas softening The blowing time is longer than 12 minutes, the slab is continuously cast with full protection pouring, and the dynamic soft reduction technology is adopted to reduce the center segregation of the continuous casting slab to obtain the slab;
[0083] The slab is heated to a heating temperature of 1173°C, and the total time in the furnace is 189 minutes, and then the first-stage rolling is carried out, that is, the rolling in the austenite recrystallization zone, the starting rolling temperature is 1160°C, and the reduction ratio of the first pass is > 10%, t...
Embodiment 2
[0084] Embodiment 2, preparation of acid corrosion resistant X65MS pipeline steel
[0085] Adopt KR method to desulfurize molten iron and high-quality steel scrap, LF refining and RH vacuum treatment to ensure the cleanliness of molten steel, LF refining uses a large amount of slag to make slag, RH vacuum treatment ensures the deep vacuum cycle time of molten steel, calcium treatment after vacuum treatment, Ar gas softening The blowing time is longer than 12 minutes, the slab is continuously cast with full protection pouring, and the dynamic soft reduction technology is adopted to reduce the center segregation of the continuous casting slab to obtain the slab;
[0086] The slab is heated to a heating temperature of 1172°C, and the total time in the furnace is 192 minutes, and then the first-stage rolling is carried out, that is, the rolling in the austenite recrystallization zone, the starting rolling temperature is 1158°C, and the reduction rate of the first pass is > 10%, th...
Embodiment 3
[0087] Embodiment 3, preparation of acid corrosion resistant X65MS pipeline steel
[0088] Adopt KR method to desulfurize molten iron and high-quality steel scrap, LF refining and RH vacuum treatment to ensure the cleanliness of molten steel, LF refining uses a large amount of slag to make slag, RH vacuum treatment ensures the deep vacuum cycle time of molten steel, calcium treatment after vacuum treatment, Ar gas softening The blowing time is longer than 12 minutes, the slab is continuously cast with full protection pouring, and the dynamic soft reduction technology is adopted to reduce the center segregation of the continuous casting slab to obtain the slab;
[0089] The slab is heated to a heating temperature of 1177°C, and the total time in the furnace is 183 minutes, and then the first-stage rolling is carried out, that is, the rolling in the austenite recrystallization zone, the starting rolling temperature is 1165°C, and the reduction rate of the first pass is > 10%, th...