
Preparation method for die graphite material used for electrical discharge machining
A graphite material and electric spark technology, which is applied in the field of mold graphite material preparation, can solve the problem that the product cannot meet the needs of users, and achieve the effect of strong practicability, full utilization of resources and cost saving.
Patent Information
- Authority / Receiving Office
- CN · China
- Current Assignee / Owner
- Publication Date
- 2013-01-30
Smart Images
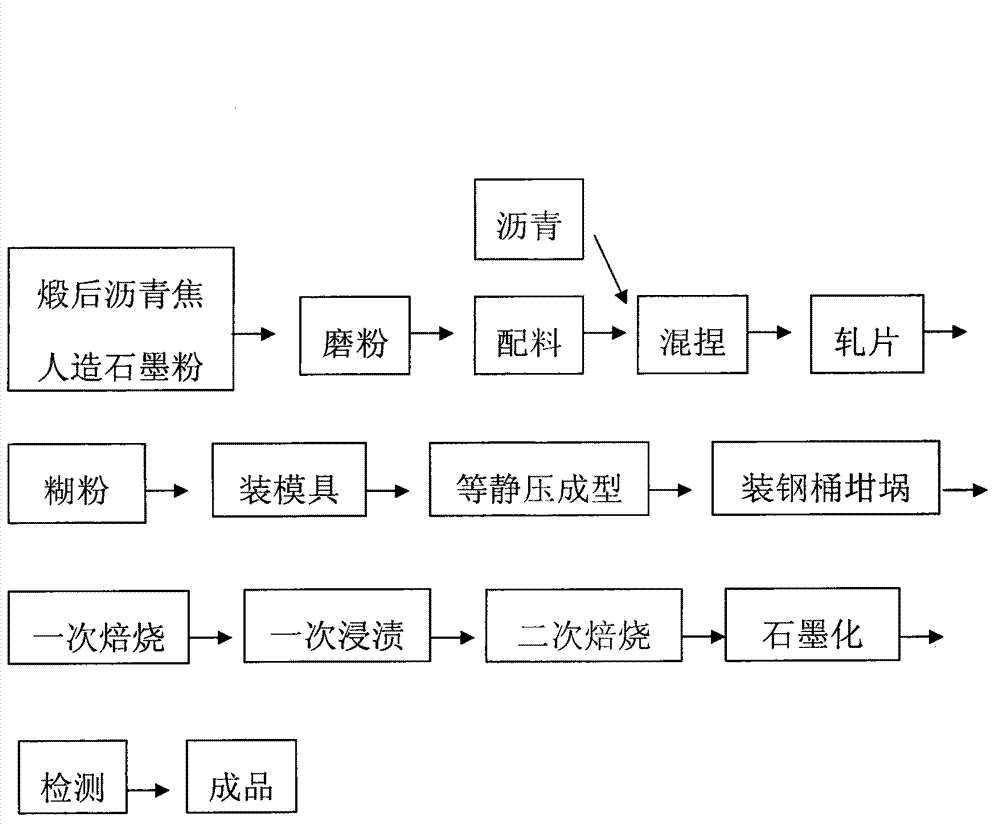
Figure 1
Abstract
Description
technical field
[0001] The invention relates to the technical field of mold graphite material preparation, in particular to a method for preparing mold graphite material used for electric discharge machining. Background technique
[0002] The large-scale mold electrode processed by high-strength graphite material is an indispensable basic material in the EDM precision machining of large-scale and special-shaped workpieces. Compared with traditional copper electrodes, graphite materials for EDM have the following advantages:
[0003] 1. Lower material cost: the price of graphite with the same volume is only 50% of copper electrode;
[0004] 2. Faster processing speed: the machining speed is 2 to 3 times that of copper electrodes, and there is no burr after processing; the discharge processing speed is 34% to 200% faster than copper electrodes;
[0005] 3. Smaller loss: the spark oil decomposes the carbide coating to compensate for the electrode loss;
[0006] 4. Lighter we...
Examples
Embodiment 1
[0029] Product preparation method:
[0030] 6.5 tons of calcined pitch coke powder (primary powder) with a particle size of D50=15 μm, 0.9 tons of artificial graphite powder of D50=15 μm, mixed with 2.4 tons of molten pitch, milled after rolling and cooling, and then used cold isostatic Pressed into a 370×750×1300mm square, roasted at 950°C for 700 hours, impregnated with 2 tons of molten pitch for 5 hours, baked again at 850°C for 350 hours, and finally purified and graphitized at 2500°C for 210 hours, high-purity Graphite electrode output is 10.2 tons.
[0031] Product physical and chemical indicators:
[0032] Standard sizes 320×700×1200mm Bulk density 1.78g / cm 3 Resistivity 13.2μΩm Flexural strength 45MPa Compressive strength 83 MPa Shore hardness 55
Embodiment 2
[0034] Product preparation method:
[0035] 6.2 tons of calcined pitch coke fine powder (primary powder) with a particle size of D50=10 μm, 0.9 tons of artificial graphite powder of D50=10 μm, mixed with 2.6 tons of molten pitch, milled after rolling and cooling, and then used cold isostatic Pressed into 250×750×1300mm squares, roasted at 950°C for 700 hours, impregnated with 2 tons of molten pitch for 5 hours, baked at 850°C for 350 hours, and finally purified and graphitized at 2500°C for 210 hours, high-purity The output of graphite electrodes is 10 tons.
[0036] Product physical and chemical indicators:
[0037] Standard sizes 220×700×1200mm Bulk density 1.78g / cm 3 Resistivity 13.2μΩm Flexural strength 51MPa Compressive strength 92MPa Shore hardness 59
Embodiment 3
[0039] Product preparation method:
[0040] 6 tons of calcined pitch coke powder (primary powder) with a particle size of D50=5 μm, 0.8 tons of artificial graphite powder of D50=5 μm, mixed with 3.2 tons of molten pitch, milled after rolling, cooling, and then using cold isostatic Pressed into a 250×750×1300mm square, roasted at 950°C for 700 hours, then impregnated with 2.4 tons of molten pitch for 5 hours, baked again at 850°C for 350 hours, and finally purified and graphitized at 2500°C for 220 hours, high-purity The output of graphite electrodes was 9.9 tons.
[0041] Product physical and chemical indicators:
[0042] Standard sizes 220×700×1200mm Bulk density 1.80g / cm 3 Resistivity 15.8μΩm Flexural strength 60MPa Compressive strength 110MPa Shore hardness 65