
Electro-chemical machining technology of inner hole wall turbulence structure of metal parts
A technology of electrochemical processing and metal parts, which is applied in the direction of electrochemical processing equipment, metal processing equipment, manufacturing tools, etc., can solve the problems of inability to process small-sized apertures, difficulties in making electrodes, and difficulty in realization, achieving small investment and shielding The influence of electric field and the effect of reducing the production cycle
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2010-12-08
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
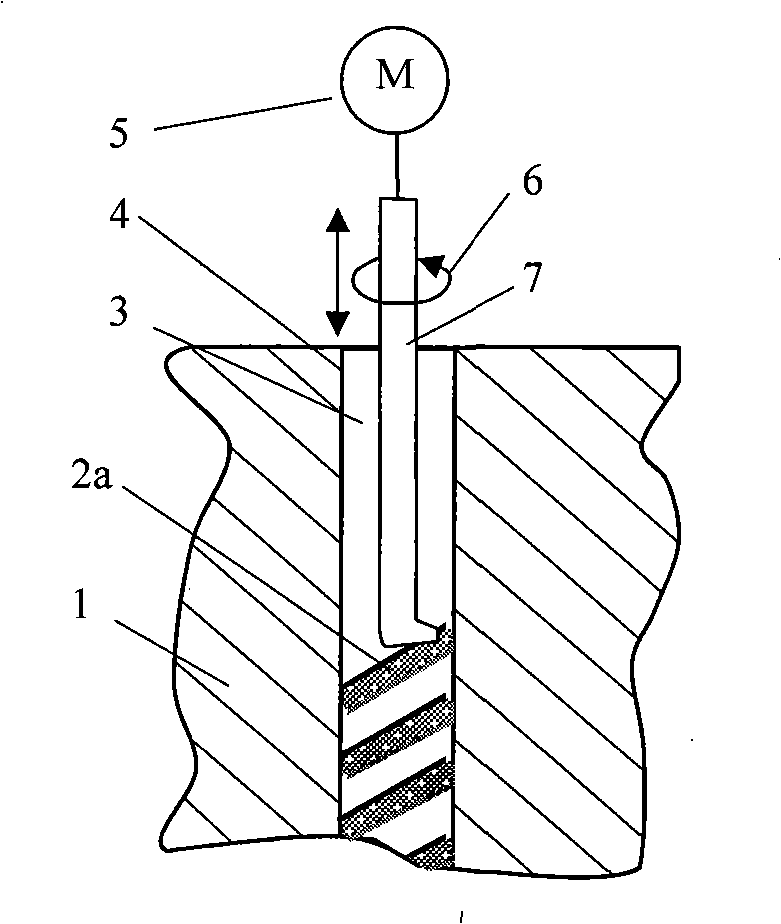
Figure 1 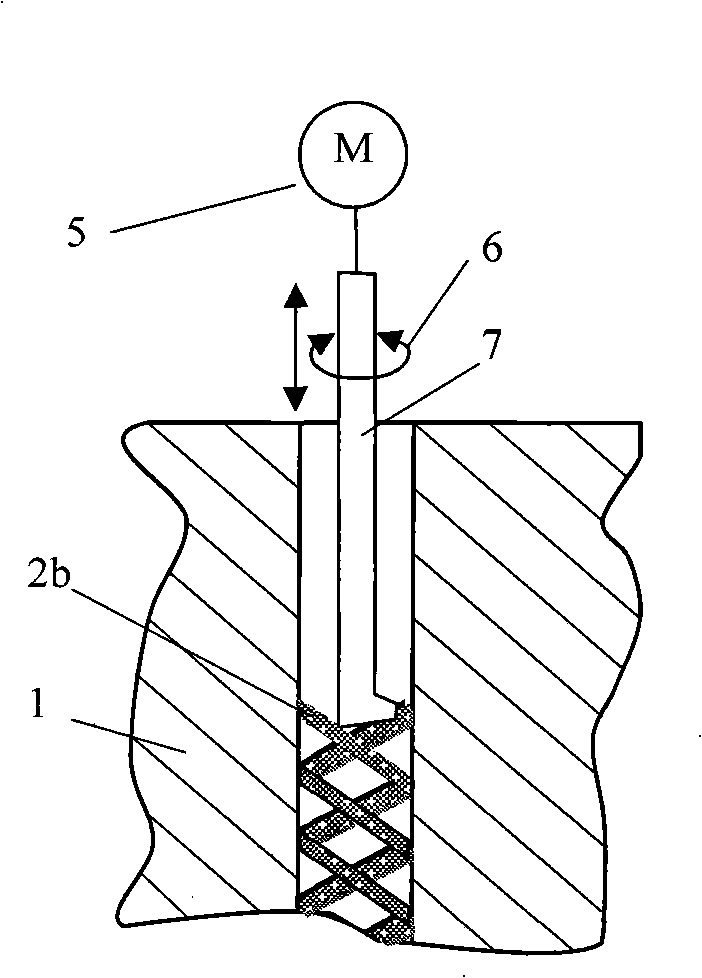
Figure 2 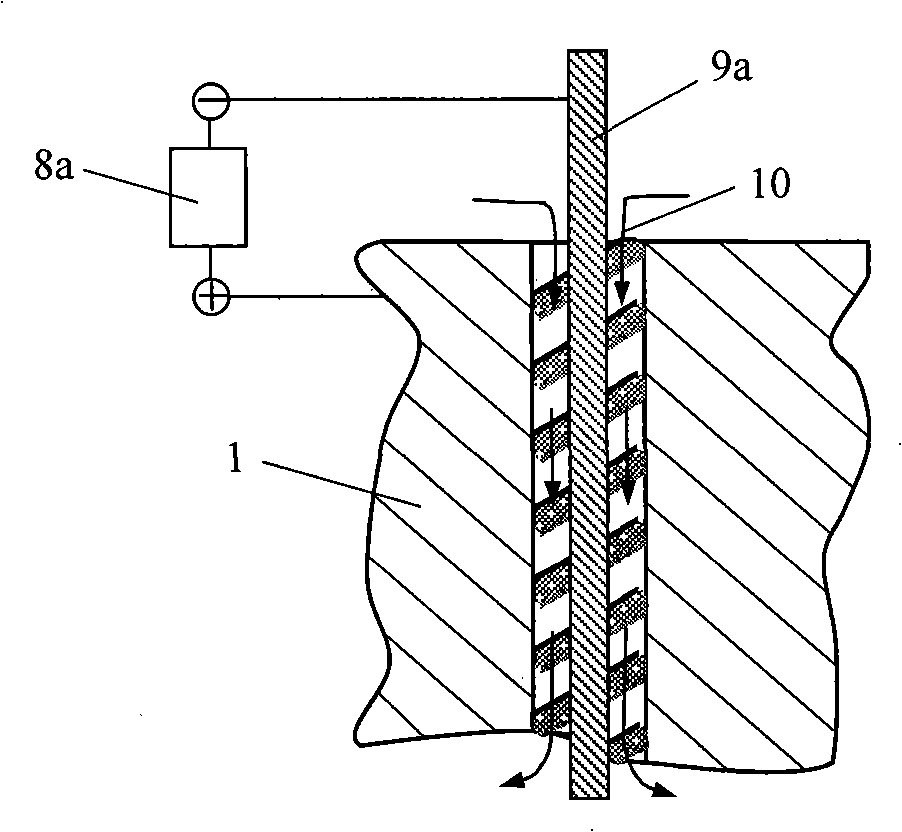
Figure 3
Abstract
Description
(1) Technical field
[0001] The invention relates to an electrochemical machining process for a turbulent flow structure on the inner hole wall of a metal part, and belongs to the technical field of special machining. (2) Background technology
[0002] In order to reduce energy consumption, the "Eleventh Five-Year" national policy proposes to reduce energy consumption by 20%, so it is particularly important to develop efficient and energy-saving energy-consuming equipment, such as used in aerospace, microelectronic cooling, energy and chemical industry, waste heat High-efficiency energy-saving heat exchangers, condensers, preheaters, etc. in the fields of recycling, air conditioning and refrigeration, and solar energy. In order to improve the heat transfer performance of the equipment and reduce energy consumption, the researchers have proved through analysis that processing several cooling channels in the heat transfer components (such as processing smooth and smooth straigh...
Examples
Embodiment 1
[0041] Embodiment 1 (groove shape turbulent flow structure):
[0042] A smooth circular hole 3 with an aperture of 3 mm is processed in advance on the metal part 1 by the electric discharge method. Next, if figure 1 As shown, the gluing spray head 7 is clamped on the machine tool spindle and penetrates into the smooth circular hole 3. The gluing spray head 7 can realize different forms of motion (such as circumferential and radial feed 6) driven by the machine tool motor 4. , The speed of the glue sprayed by the glue nozzle is controlled by an external pressure pump. The insulating glue 2 is made of 352AUV epoxy resin glue, and the curing agent is triethylenetetramine. For every 100 parts of resin, 10 parts of curing agent are used: 3 at 100°C hours to cure.
[0043] After the insulating glue 2 is cured, the metal part 1 is installed on the electrolytic processing machine tool, the workpiece is connected to the positive electrode of the electrolytic processing power supply ...
Embodiment 2
[0045] Embodiment 2 (boss-shaped turbulent flow structure):
[0046] A smooth round hole 3 with a diameter of 2 mm is pre-machined on the metal part 1 by electric discharge machining, and then a layer of insulating glue 2 is applied on the inner wall of the smooth round hole 3 by the same glue coating method as in Example 1. After the insulating glue 2 is cured, coat the outer surface 12 of the metal part with a layer of insulating glue and put it into the electrolyte tank filled with electroforming liquid, and the metal wire 13 for electroforming passes through the central axis of the smooth circular hole on the metal part 1 , the moving speed of the wire 13 for electroforming is controlled by the pay-off wheel and the take-up wheel, as the wire 13 for electroforming moves axially in the hole, the electroforming liquid is brought into the smooth circular hole 3, and a suitable The type of electrolyte is compatible with the metal to be deposited. When the workpiece is connecte...