
An ultra-low hydrogen high toughness welding rod for welding penstocks in hydropower stations
A pressure steel pipe, ultra-low hydrogen technology, applied in the direction of welding medium, welding equipment, welding/cutting medium/material, etc., can solve the problem of limited moisture absorption performance of electrode coating, many inclusions in deposited metal, and inability to stabilize impact toughness To achieve the effect of improving dehydrogenation capacity, improving refining effect and reducing hydrogen partial pressure
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2016-04-13
Smart Images
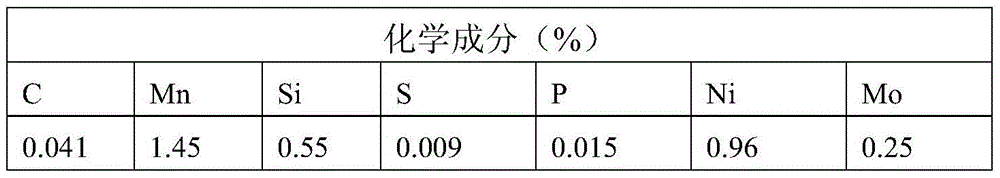
Figure 1 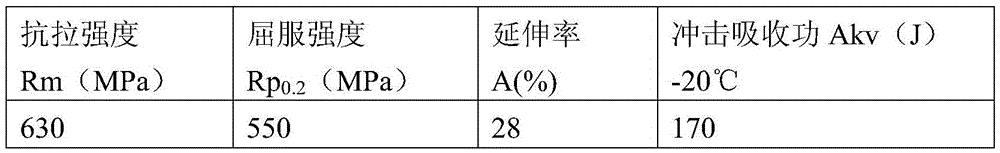
Figure 2 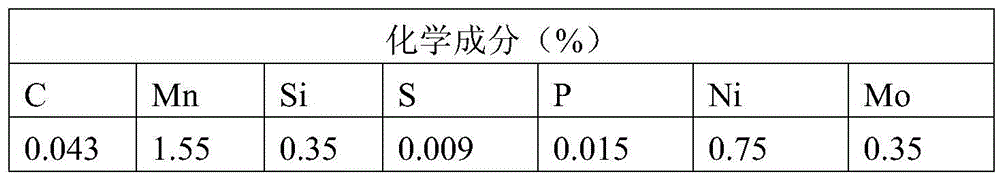
Figure 3
Abstract
Description
technical field
[0001] The invention relates to an ultra-low-hydrogen high-toughness welding rod for welding a water diversion pressure steel pipe of a hydropower station, and belongs to the field of welding materials. Background technique
[0002] The welding of penstock steel pipes for water diversion in hydropower stations is the most important link in the fabrication and installation of metal structures in hydropower stations. The steel pipe base material generally adopts low-alloy high-strength quenched and tempered steel plates with a tensile strength of 610MPa, SUMIPEN610F and NK-HITEN610U2, which are manufactured by Sumitomo and NKK in Japan, respectively. This type of steel has a very reasonable alloy element design, very low C content and S, P impurity content, and a very stable structure. With its good comprehensive mechanical properties and process properties, it has won most of the domestic hydropower penstock market. For example, in the 26 generating units of ...
Examples
Embodiment 1
[0024] Embodiment 1: the percentage by weight of each component in the drug skin is shown in the following table:
[0025] Raw material name
weight percentage
Raw material name
weight percentage
marble
40
Electrolytic manganese
5
4
Atomized ferrosilicon
6
18
Light Rare Earth Ferrosilicon
1
3
ferro-titanium
9
Dehydrated feldspar
3
0.5
Zircon sand
3
3
4
0.5
[0026] The deposited metal composition of the electrode prepared according to the above ratio is shown in the following table:
[0027]
[0028] The mechanical properties of the deposited metal of the electrode prepared according to the above ratio are shown in the following table:
[0029]
[0030] The hydrogen content of the deposited metal of the electrode prepared...
Embodiment 2
[0032] Embodiment 2: the percentage by weight of each component in the drug skin is shown in the following table:
[0033] Raw material name
weight percentage
Raw material name
weight percentage
marble
45
Electrolytic manganese
6
2
Atomized ferrosilicon
3
23
Light Rare Earth Ferrosilicon
2
2
ferro-titanium
7
Dehydrated feldspar
1
1
Zircon sand
2
2
3
1
[0034] The deposited metal composition of the electrode prepared according to the above ratio is shown in the following table:
[0035]
[0036] The mechanical properties of the deposited metal of the electrode prepared according to the above ratio are shown in the following table:
[0037]
[0038] The hydrogen content of the deposited metal of the electrode prepared acc...
Embodiment 3
[0040] Embodiment 3: the percentage by weight of each component in the drug skin is shown in the following table:
[0041] Raw material name
weight percentage
Raw material name
weight percentage
marble
50
Electrolytic manganese
4
dolomite
2
Atomized ferrosilicon
4
18
Light Rare Earth Ferrosilicon
3
quartz
2
ferro-titanium
8
Dehydrated feldspar
1
0.5
Zircon sand
1
nickel powder
4
Potassium titanate
2
Rare earth fluoride
0.5
[0042] The deposited metal composition of the electrode prepared according to the above ratio is shown in the following table:
[0043]
[0044] The mechanical properties of the deposited metal of the electrode prepared according to the above ratio are shown in the following table:
[0045]
[0046] The hydrogen content of the deposited metal of the electrode prepared...