
A kind of rubber compound of hourglass spring and preparation method thereof
A technology of rubber compound and hourglass spring, applied in the field of polymer materials, can solve the problem that the rubber compound fails to meet the requirements of combustion performance standards.
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2021-07-27
Smart Images
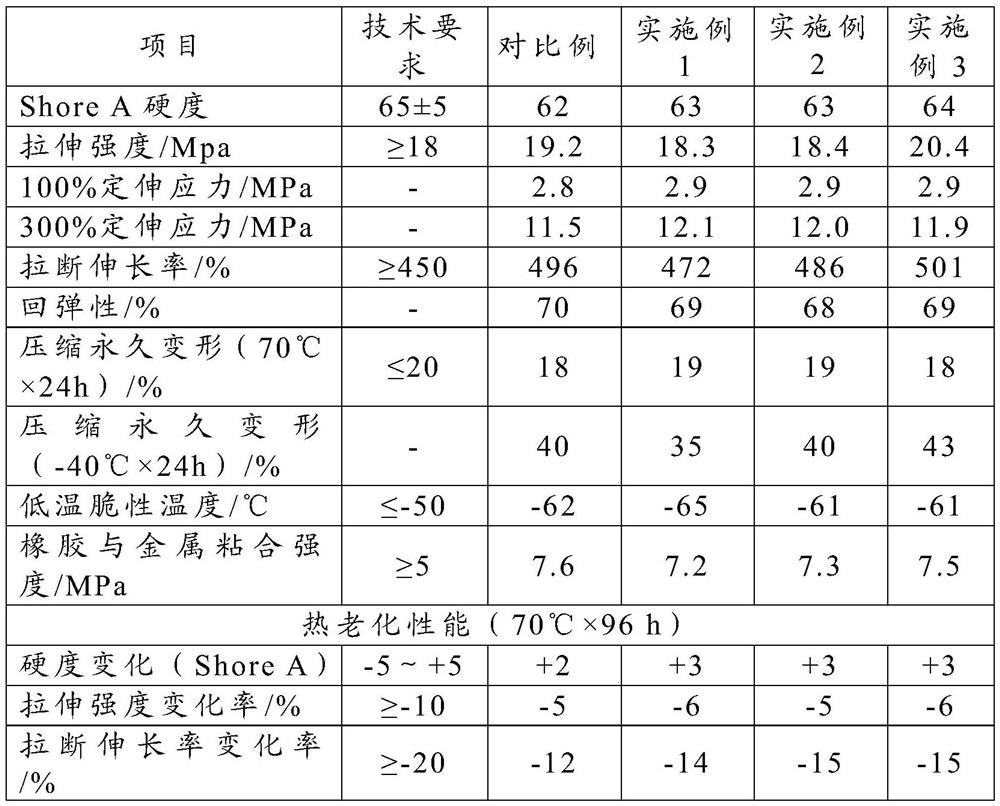
Figure 1 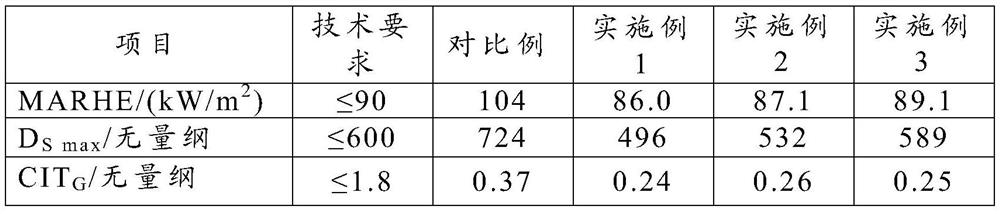
Figure 2 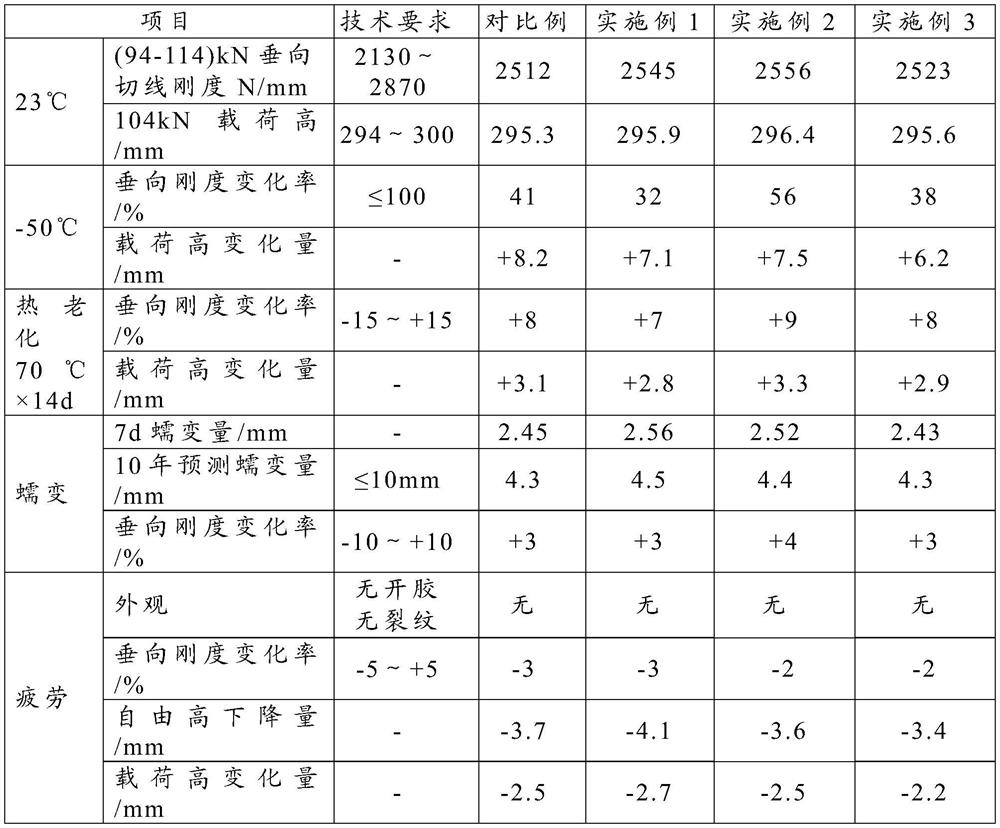
Figure 3
Abstract
Description
technical field
[0001] The invention belongs to the field of polymer materials, and in particular relates to a rubber material for an hourglass spring and a preparation method thereof. Background technique
[0002] Modern railway vehicles use a large number of rubber elastic components in the suspension system, equipment installation system, connection, limit and other parts. However, these rubber components are combustible or flammable materials. Once a fire breaks out, the rubber compound will burn and emit a lot of heat and smoke, and the smoke is often toxic to a certain extent, which is not conducive to the evacuation of personnel when the vehicle is on fire. and escape, which increases the fire safety hazard in the event of a fire.
[0003] At present, many countries have begun to adopt the standard EN45545-2 to regulate the fire performance requirements of materials and components used in railway vehicles. The EN45545-2 standard puts forward clear combustion perform...
Examples
Embodiment 1
[0050] A rubber compound for an hourglass spring, the rubber compound component comprises, in parts by mass:
[0051] 55 parts of natural rubber, 30 parts of low-cis polybutadiene rubber, 15 parts of solution polystyrene butadiene rubber, 5 parts of zinc oxide, 2 parts of stearic acid, 1.7 parts of sulfur, 0.6 parts of accelerator TBTD, 1.5 parts of accelerator CBS , 25 parts of white carbon black, 25 parts of carbon black, 2 parts of anti-aging agent 4010NA, 1 part of anti-aging agent RD, 2 parts of paraffin, 2.5 parts of modifier, 3 parts of toluene diphenyl phosphate, 6 parts of naphthenic oil, high molecular weight 8 parts of crystal form-II ammonium polyphosphate.
[0052] Concrete preparation steps are as follows:
[0053] Manufacturing equipment and key process parameters: intermeshing type internal mixer with nominal volume (90-250) L, temperature control unit temperature setting within 30-40 °C, upper jacking bolt pressure 0.45-0.6 MPa. The internal mixer rotor spee...
Embodiment 2
[0062] A rubber compound for an hourglass spring, the rubber compound component comprises, in parts by mass:
[0063] 60 parts of natural rubber, 20 parts of low-cis polybutadiene rubber, 20 parts of solution polystyrene butadiene rubber, 7 parts of zinc oxide, 4 parts of stearic acid, 3 parts of sulfur, 1.6 parts of accelerator TBTD, 2.8 parts of accelerator CBS 25 parts of white carbon black, 25 parts of carbon black, 4 parts of antioxidant 4010NA, 2 parts of antioxidant RD, 2 parts of paraffin, 3.5 parts of modifier, 3 parts of toluene diphenyl phosphate, 6 parts of naphthenic oil, high molecular weight 4 parts of crystal form-II ammonium polyphosphate.
[0064] Concrete preparation steps are as follows:
[0065] Manufacturing equipment and key process parameters: intermeshing type internal mixer with nominal volume (90-250) L, temperature control unit temperature setting within 30-40 °C, upper jacking bolt pressure 0.45-0.6 MPa. The internal mixer rotor speed of the foll...
Embodiment 3
[0074] A rubber compound for an hourglass spring, the rubber compound component comprises, in parts by mass:
[0075] 70 parts of natural rubber, 20 parts of low-cis polybutadiene rubber, 10 parts of solution polystyrene butadiene rubber, 5 parts of zinc oxide, 2 parts of stearic acid, 1.7 parts of sulfur, 1 part of accelerator TBTD, 2.5 parts of accelerator CBS , 25 parts of white carbon black, 25 parts of carbon black, 1 part of anti-aging agent 4010NA, 0.5 part of anti-aging agent RD, 2 parts of paraffin, 2.5 parts of modifier, 2 parts of toluene diphenyl phosphate, 4 parts of naphthenic oil, high molecular weight crystal Type-II ammonium polyphosphate 10 parts.
[0076] Concrete preparation steps are as follows:
[0077] Manufacturing equipment and key process parameters: intermeshing type internal mixer with nominal volume (90-250) L, temperature control unit temperature setting within 30-40 °C, upper jacking bolt pressure 0.45-0.6 MPa. The internal mixer rotor speed of...