
Composite explosion-proof board capable of shielding high speed broken sheets and high strength blasting impact, and manufacturing method thereof
An explosive impact and high-strength technology, applied in chemical instruments and methods, blasting, protective clothing, etc., can solve problems such as short boards in usability, inconvenient disassembly and transportation, secondary damage, etc., and achieve strong impact performance and convenient production , the effect of simple structure
Patent Information
- Authority / Receiving Office
- CN · China
- Current Assignee / Owner
- Publication Date
- 2019-09-06
Smart Images
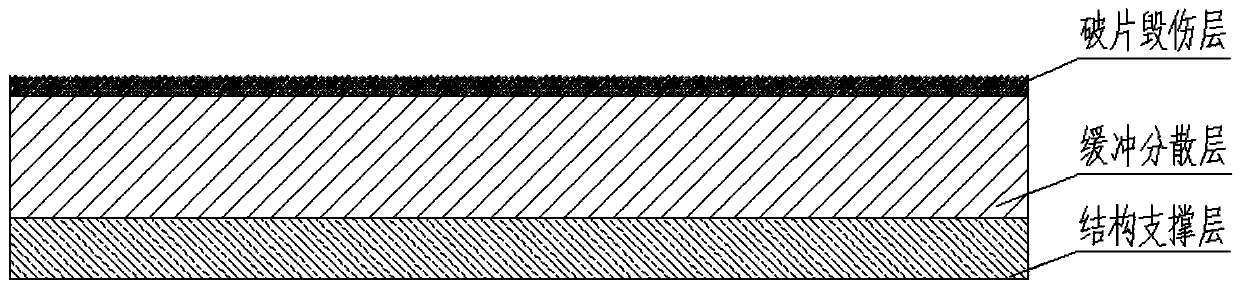
Figure 1 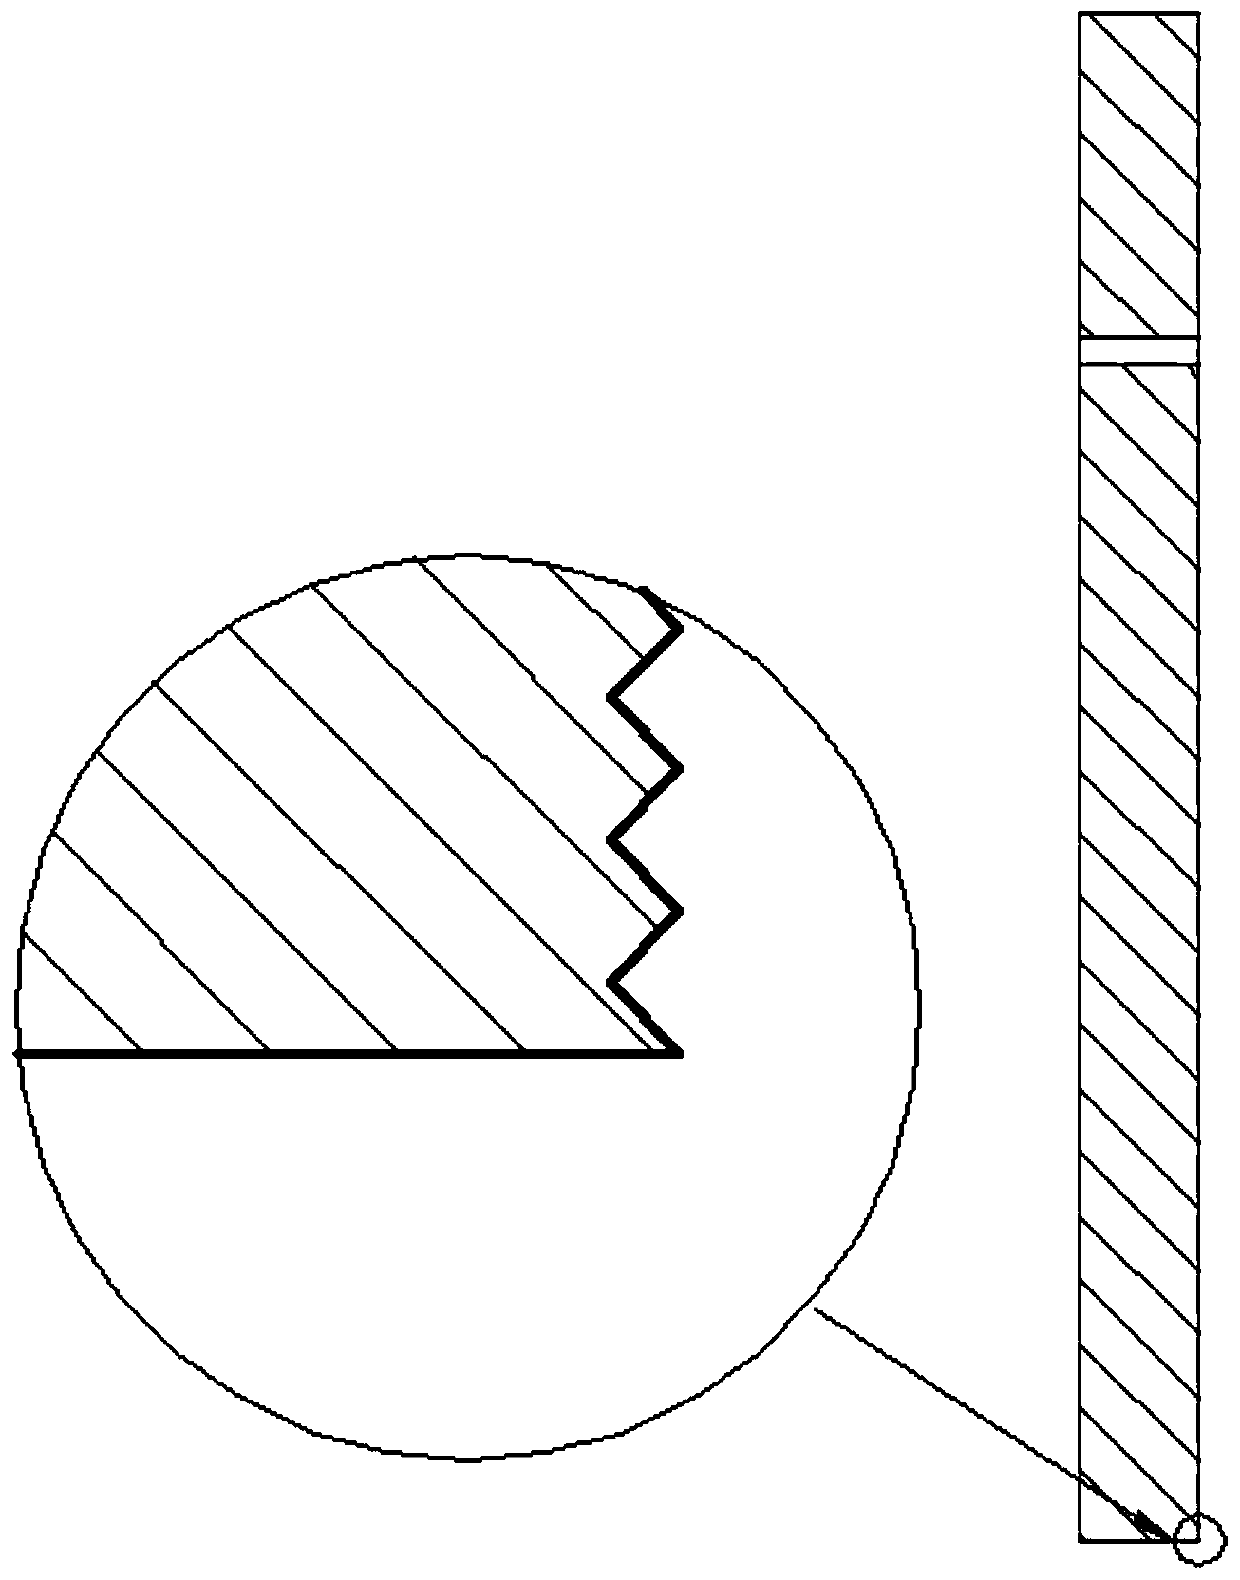
Figure 2
Abstract
Description
technical field
[0001] The invention relates to a composite explosion-proof plate and a manufacturing method for resisting high-speed fragments and high-intensity explosion impacts, and relates to a composite explosion-proof plate capable of protecting against ultra-high-intensity explosion shock waves (≤0.15MPa) and ultra-high-speed fragment damage (≤1700m / s) Plates and manufacturing methods. Background technique
[0002] The field combat training and field testing of the missile force are routine and necessary training items. During the training process, it is necessary to protect the personnel, equipment and related materials in the designated area. Traditional plate protection materials include steel plates, sand, concrete, etc., but a single material has different degrees of "short boards" in terms of usability. For example: steel plates are heat-resistant but not fire-resistant, and have poor corrosion resistance; the amount of sand required to resist high-strength ex...
Examples
example
[0028] Example: A composite explosion-proof plate and its manufacturing method
[0029] The composite explosion-proof plate formed by the present invention has a length of 1050 mm, a width of 750 mm and a thickness of 35 mm. The specific preparation process is as follows:
[0030] The first step is to pass the high-strength structural steel plate through the planer, and process the sharp-edged structure damaged by fragments on one side;
[0031] In the second step, the surface of ultra-high molecular polyethylene is frosted.
[0032] The third step is to weave the high-strength fiber fabric according to the designed weaving method;
[0033] The fourth step is to make the woven fabric into prepreg;
[0034] The fifth step is to cut the prepreg according to the designed layup size and method;
[0035] In the sixth step, the structural support layer is laid and hot-pressed. The molding temperature is 160°C, the molding pressure is 45MPa, and the heating and curing time is 6h...