
Design method of large-diameter thick-walled tube casting and extrusion compound forming mold cavity
A composite forming and design method technology, applied in the direction of metal extrusion die, metal extrusion mandrel, etc., can solve the problem of uneven microstructure of formed parts, and achieve uniform and compact internal structure, good plasticity and toughness, and excellent overall performance Effect
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2018-12-28
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
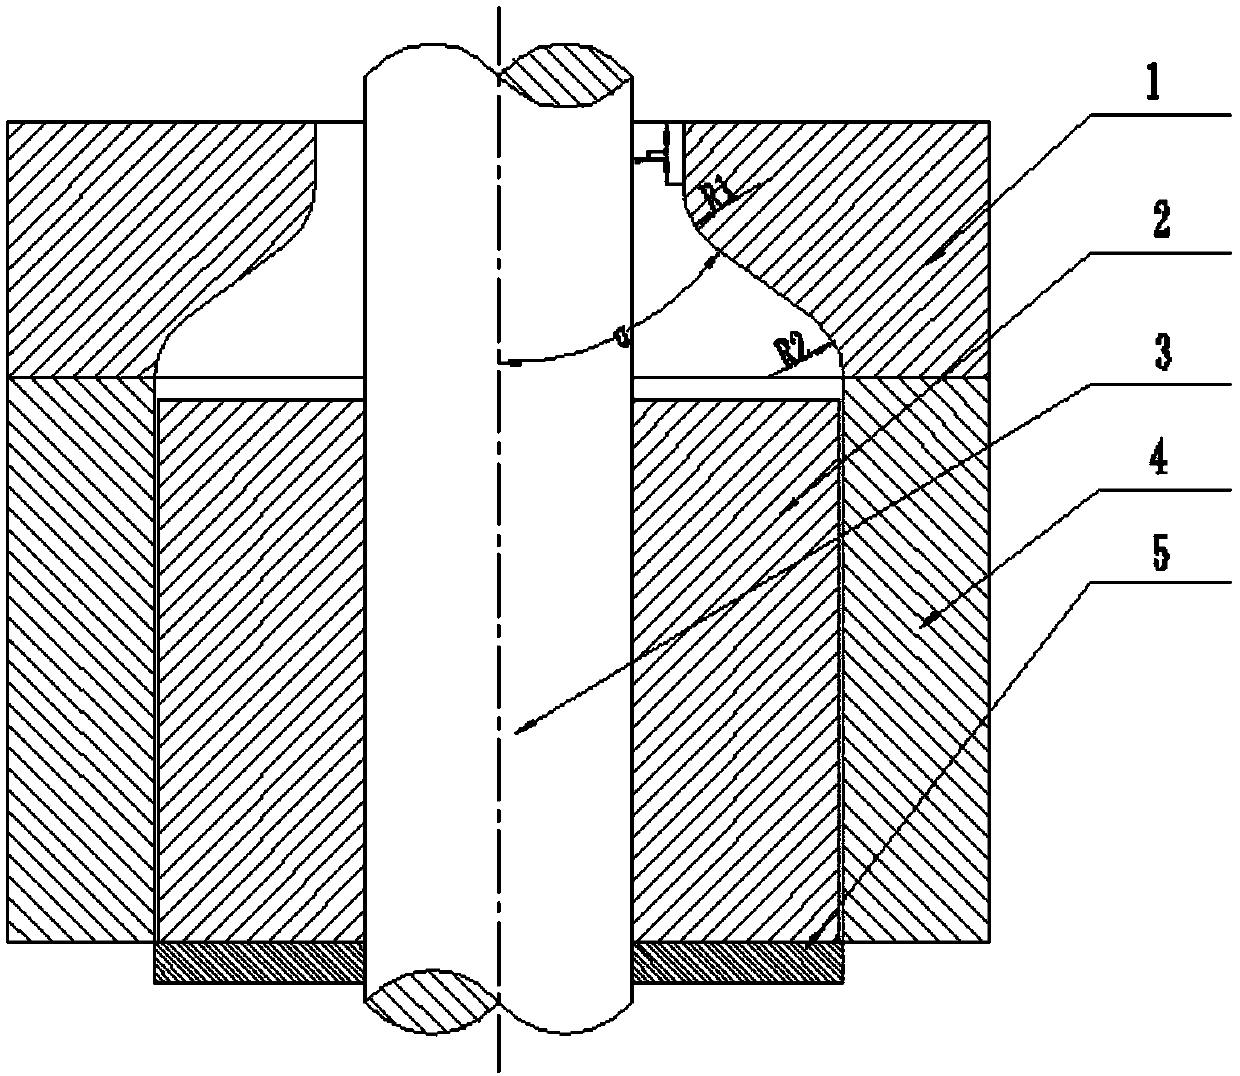
Figure 1 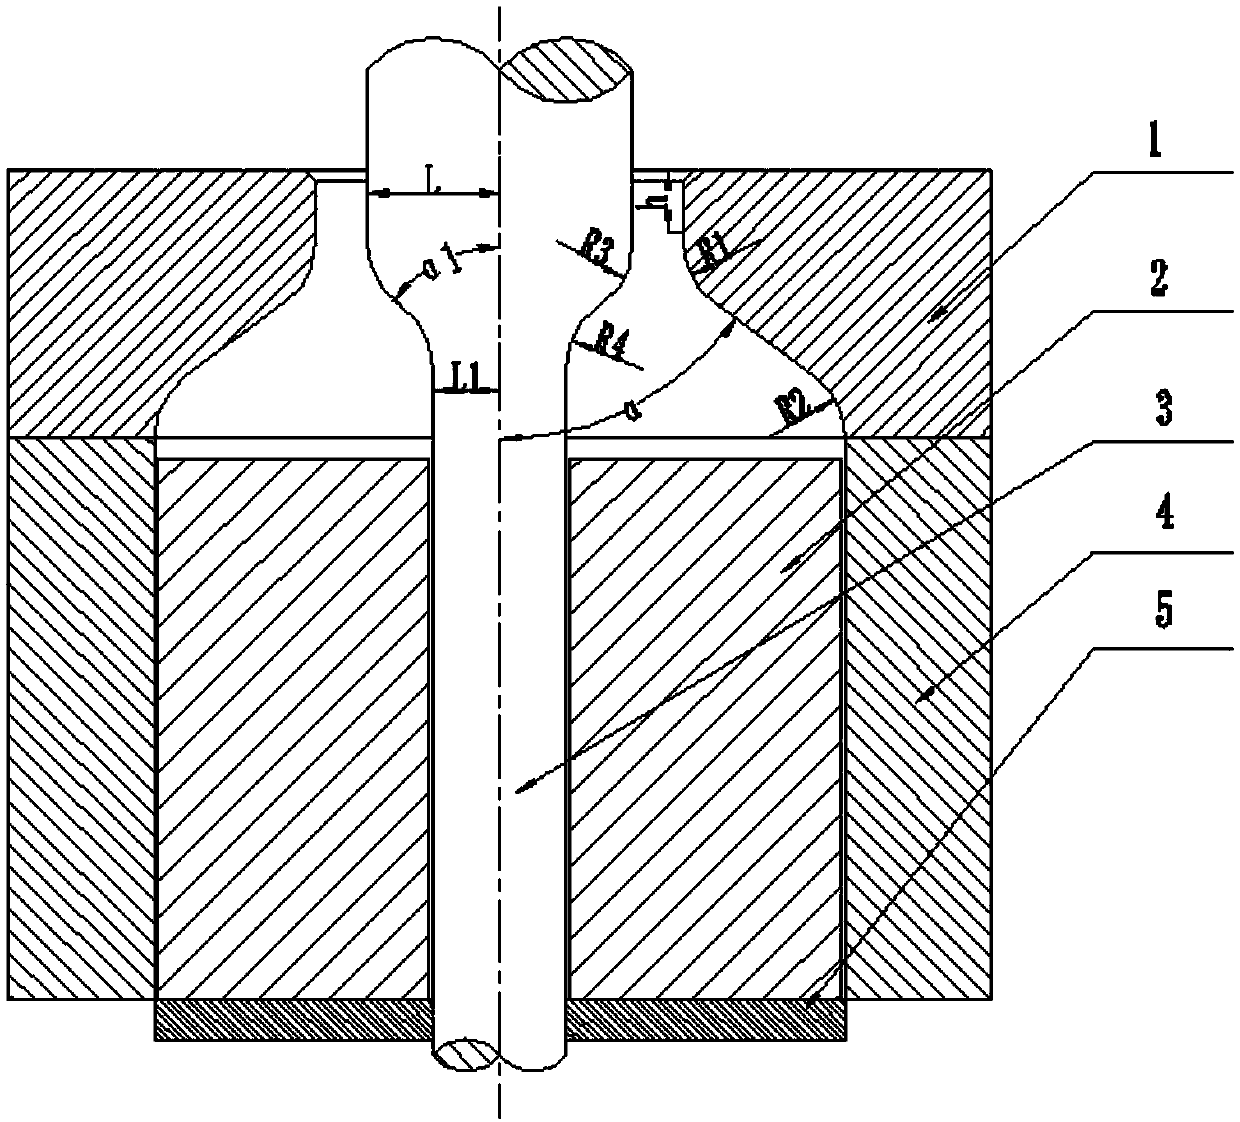
Figure 2
Abstract
Description
technical field
[0001] The invention belongs to the technical field of large-diameter thick-walled pipe casting-extrusion composite forming, and in particular relates to a design method for a mold cavity of large-diameter thick-walled pipe casting-extrusion composite forming. Background technique
[0002] Large-diameter thick-walled seamless pipe is an important large-scale component in thermal power, nuclear power, national defense and shipbuilding industries. With the rapid development of my country's large-scale supercritical thermal power units, nuclear power units, petrochemical, aerospace, shipbuilding, high-speed rail and military industries, the demand for large-diameter thick-walled pipes is increasing.
[0003] When using traditional hot extrusion dies to produce large-diameter thick-walled pipes in combination with casting and extrusion, due to the small amount of deformation of the pipe wall, especially the inner wall, during the forming process, and the large di...
Examples
Embodiment 1
[0017] Such as figure 1 and figure 2 As shown, the figure includes extrusion die 1, billet 2, mandrel 3, extrusion cylinder 4 and punch 5. Taking the formed pipe fitting size φ720mm×100mm (wall thickness) as an example, a large-diameter thick-walled pipe casting The design method of the mold cavity of extrusion composite molding comprises the following steps:
[0018] 1) Determine the parameters of the extrusion model cavity, including: the half-angle angle α of the extrusion die cone surface is 54°, the length h of the sizing belt is 85mm, and the transition fillet radius R1 between the extrusion die cone surface and the sizing belt is 150mm , The radius R2 of the transition fillet between the extrusion die cone surface and the extrusion barrel wall is 160mm;
[0019] 2) Determine the transition position of the mandrel section to ensure that the inner and outer walls of the pipe end the plastic deformation at the same time;
[0020] 3) Determine the dimensional parameters...
Embodiment 2
[0022] Such as figure 1 and figure 2 As shown, the figure includes extrusion die 1, billet 2, mandrel 3, extrusion cylinder 4 and punch 5. Taking the formed pipe fitting size φ1067mm×52mm (wall thickness) as an example, a large-diameter thick-walled pipe casting The design method of the mold cavity of extrusion composite molding comprises the following steps:
[0023] 1) Determine the parameters of the extrusion model cavity, including: the half-angle angle α of the extrusion die cone surface is 53°, the length h of the sizing belt is 128mm, and the transition fillet radius R1 between the extrusion die cone surface and the sizing belt is 160mm , The radius R2 of the transition fillet between the extrusion die cone surface and the extrusion barrel wall is 160mm;
[0024] 2) Determine the transition position of the mandrel section to ensure that the inner and outer walls of the pipe end the plastic deformation at the same time;
[0025] 3) Determine the dimensional parameter...
Embodiment 3
[0027] Such as figure 1 and figure 2 As shown, the figure includes extrusion die 1, billet 2, mandrel 3, extrusion cylinder 4 and punch 5. Taking the formed pipe fitting size φ1300mm×85mm (wall thickness) as an example, a large-diameter thick-walled pipe casting The design method of the mold cavity of extrusion composite molding comprises the following steps:
[0028] 1) Determine the parameters of the extrusion model cavity, including: the half-angle angle α of the extrusion die cone surface is 55°, the length h of the sizing belt is 140mm, and the transition fillet radius R1 between the extrusion die cone surface and the sizing belt is 170mm , The radius R2 of the transition fillet between the extrusion die cone surface and the extrusion barrel wall is 160mm;
[0029] 2) Determine the transition position of the mandrel section to ensure that the inner and outer walls of the pipe end the plastic deformation at the same time;
[0030] 3) Determine the dimensional parameter...