
Patents
Literature
48 results about "Ceramic forming techniques" patented technology
Efficacy Topic
Property
Owner
Technical Advancement
Application Domain
Technology Topic
Technology Field Word
Patent Country/Region
Patent Type
Patent Status
Application Year
Inventor
Ceramic forming techniques are ways of forming ceramics, which are used to make everyday tableware from teapots, to engineering ceramics such as computer parts. Pottery techniques include the potter's wheel, slipcasting, and many others.
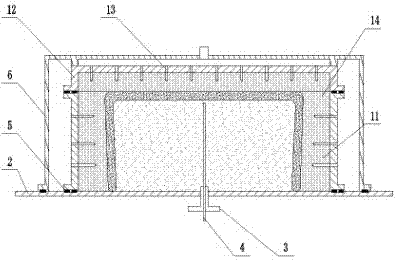
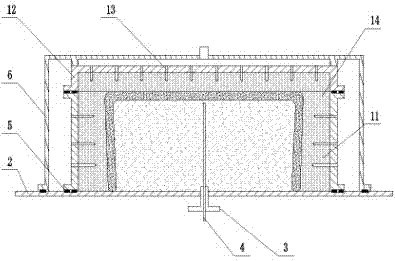
Special mold for ceramic blank high-pressure slip casting process
The invention belongs to the technical field of ceramic forming and particularly relates to a bathroom ceramic blank forming mold, which comprises an outer mold and a support plate, wherein the support plate seals the outer mold. The bathroom ceramic blank forming mold is characterized in that the outer mold comprises a water-absorption ventilation K gypsum mold and a steel sleeve, the steel sleeve is arranged on the outer wall of the K gypsum mold, ventilation holes are arranged on the steel sleeve, and a slip casting opening and an air injection opening are arranged on the support plate. When a special mold for the ceramic blank high-pressure slip casting process disclosed by the invention is adopted, the intensity is high, the high-pressure damage is avoided, and in addition, water penetration and ventilation can be realized.
Owner:重庆国之四维卫浴有限公司
High pressure grouting forming process for ceramic billet
ActiveCN102528898ANot fragileEasy to separateCeramic shaping apparatusSlurryCeramic forming techniques
The invention belongs to the technical field of ceramic forming, in particular relates to a forming process for a bathroom ceramic billet, which comprises the steps: (1) allocating forming materials according to ratio and mixing the forming materials into even slurry; (2) pressing the slurry into a high strength permeable mold, enabling the pressure of the slurry in the permeable mold to be kept at 0.3-1.6MPa for 0.5-5minutes, and enabling the slurry to crust and form the ceramic billet; (3) discharging the slurry left in the high strength permeable mold; (4) blowing compressed air into the high strength permeable mold, and keeping the pressure of the compressed air in the high strength mold at 0.1-0.25MPa for 0.1-1minute; (5) enabling the inside and the outside of the ceramic billet to form pressure difference of 100-1000Pa by increasing the outside pressure of the high strength permeable mold, keeping the pressure difference at no less than 0.1 second, and enabling the ceramic billet to be separated from the high strength permeable mold; and (6) separating the high strength permeable mold to obtain the ceramic billet. By means of the high pressure grouting forming process for the ceramic billet of the technical scheme, required number of the mold is small, and manufacture efficiency and compact evenness of the billet are high.
Owner:重庆国之四维卫浴有限公司
Preparation method of ceramic micro-bead grinding medium
InactiveCN107266025APerformance is not affectedWith strengthOther chemical processesClaywaresLoss rateCeramic molding
The invention relates to a preparation method of a ceramic microbead grinding medium, belonging to the technical field of ceramic molding. The present invention firstly uses kaolin, silicon carbide, lime clay etc. as raw materials, and ball mills after mixing to obtain a mixed powder; then mixes the mixed powder and water to obtain a slurry; adds egg white and sucrose respectively to the slurry, After mixing, stir to obtain a foamy slurry; ballize the foamy slurry and fire to obtain hollow ceramic microspheres, and grind the hollow ceramic microspheres to obtain hollow microspheres with a rough surface; then use Fe, Mn, Mo, etc. as The raw materials are heated and melted to obtain a mixed metal liquid, the hollow microspheres with rough surfaces are soaked in the mixed metal liquid, taken out, naturally cooled to room temperature, dried and polished. The ceramic microbead grinding medium prepared by the invention has high hardness, low wear resistance rate and good wear resistance.
Owner:周荣
Novel vacuum degassing method for gelcasting ceramic slurry
The present invention discloses vacuum bubble-eliminating method for injected ceramic slurry via adding polymerization retarder to ensure no curing during vacuum pumping, and belongs to the field of ceramic forming technology. Into slurry, initiator, catalyst and polymerization retarder comprising phenothiazine and catechol are added through stirring; and the slurry is then pumped to eliminate bubble for 10-15 min to obtain slurry with excellent flowability and no bubble for injection directly. Adding polymerization retarder in certain amount can delay the cure of the slurry to ensure vacuum deairing effect without affecting the normal curing of the slurry in subsequent step.
Owner:TSINGHUA UNIV
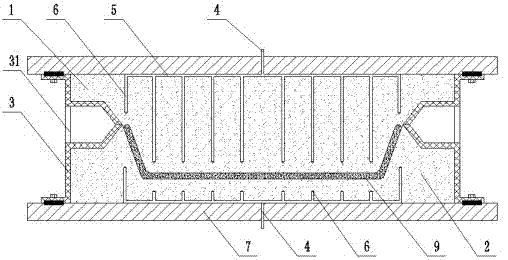
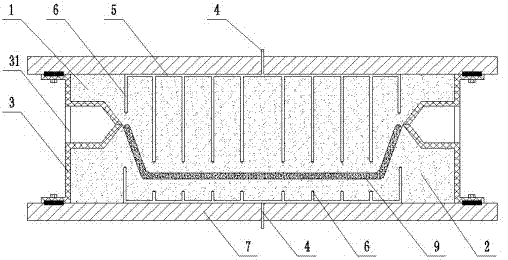
Mold special for direct-pressing forming of bathroom ceramic blank
InactiveCN102398301AReduce stickingImprove water absorptionMouldsCeramic forming techniquesMold removal
The invention belongs to the technical field of ceramic forming and in particular relates to a forming mold of a bathroom ceramic blank. The forming mold comprises a male die and a female die, which are matched with each other. The forming mold is characterized in that: the male die and the female die consist of water-absorbable and air-permeable K gypsum; steel mold sleeves are arranged on side walls of the male die and the female die and restrain the deformation of the side walls; and air inlets which are communicated with compressed air are arranged on the steel mold sleeves. By adoption of the technical scheme of the invention, the mold for direct-pressing forming of the bathroom ceramic blank is high in intensity, water-absorbable and air-permeable, and facilitates de-molding of the blank.
Owner:CHONGQING SWELL SANITARY WARE GRP
Method for preparing uranium dioxide microspheres at normal temperature
ActiveCN111039326AOvercomes the disadvantage of needing to freezeLow thermal conductivityUranium dioxideUranium oxideHexamethylenetetramine
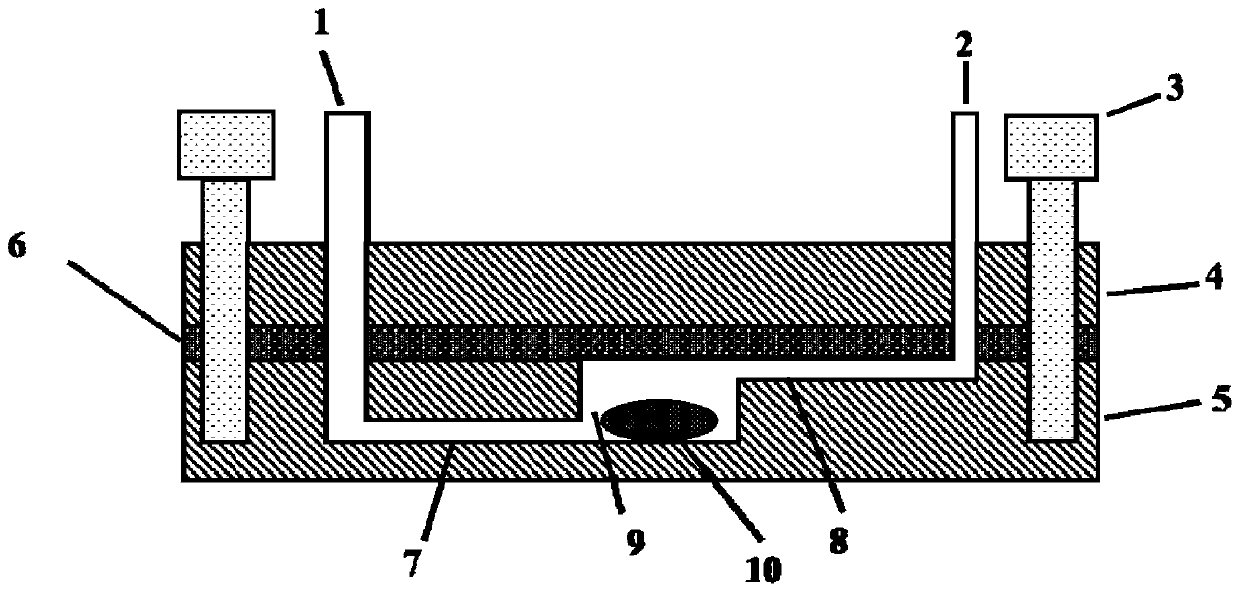
The invention relates to a method for preparing uranium dioxide microspheres at normal temperature, and belongs to the technical field of ceramic forming. According to the method, components in an internal gel solution are divided into a uranyl nitrate solution (ADUN) stable at normal temperature and a mixed solution (HMUR) of urea and hexamethylenetetramine; the two solutions are rapidly mixed inan automatic mixing device to form an unstable uranium glue solution; the mixed uranium glue solution rapidly enters silicone oil, and is shear into liquid drops with uniform sizes by the silicone oil; the liquid drops and the silicone oil are cured into gel microspheres by a microwave heating device; and the gel microspheres are washed, dried and sintered to obtain monodisperse UO2 sintered microspheres with uniform sizes and good sphericity. According to the invention, microfluidic control is adopted in the whole process of the method, so that the UO2 microspheres are prepared at normal temperature through an internal gel method without human interference, and the automation degree is high.
Owner:TSINGHUA UNIV
Vertical compression forming process for ceramic blanks for bathrooms
InactiveCN102441935AReduce moisture contentLow input costCeramic extrusion diesCeramic forming techniquesForming processes
The invention belongs to the technical field of ceramic forming, and particularly relates to forming process for ceramic blanks for bathrooms. The forming process comprises steps that 1, forming materials are prepared according to proportion and mixed uniformly, 2, forming mud of a blank is refined and uniformly mixed, and moisture content of the mud is controlled below 30%, 3, forming mud in corresponding weight is taken according to the weight of the formed blank, 4, the forming mud is placed in a forming mold, and the mold is squeezed so that the blank is formed, and 5, by the aid of the forming mold, air is blown into a combined part of the forming mold and the blank, so that the blank is separated from the forming mold and is produced. The vertical compression forming process for ceramic blanks for bathroom is fast in forming speed, high in manufacturing efficiency, low in mold cost and small in occupied area, and the blank is compact sufficiently.
Owner:CHONGQING SWELL SANITARY WARE GRP
Liquid phase pretreatment method for gelcasting ceramic blank before binder burning out
The present invention belongs to the field of ceramic forming technology, and is the new liquid phase pre-treatment method of degrading organic matter in biscuit to prevent cracking during eliminating glue. The ceramic biscuit after gel injection molding is liquid phase pre-treated inside water solution o ammonium persulfate or potassium persulfate before eliminating glue. Under the action of peroxide, the polymer inside the ceramic biscuit is chain breaking degraded, the netted macro molecule becomes small molecule and internal stress in the biscuit is released. The biscuit thus treated will not crack and will have no fault during overheat defatting and glue eliminating. The present invention is simple in technological process, low in cost and suitable for industrial production.
Owner:TSINGHUA UNIV
Cermic Sizing material fast and controllable solidfying colloied state shaping method and device
InactiveCN1246255CQuality improvementShort curing timeCeramic shaping apparatusCement mixing apparatusSlurryHigh pressure
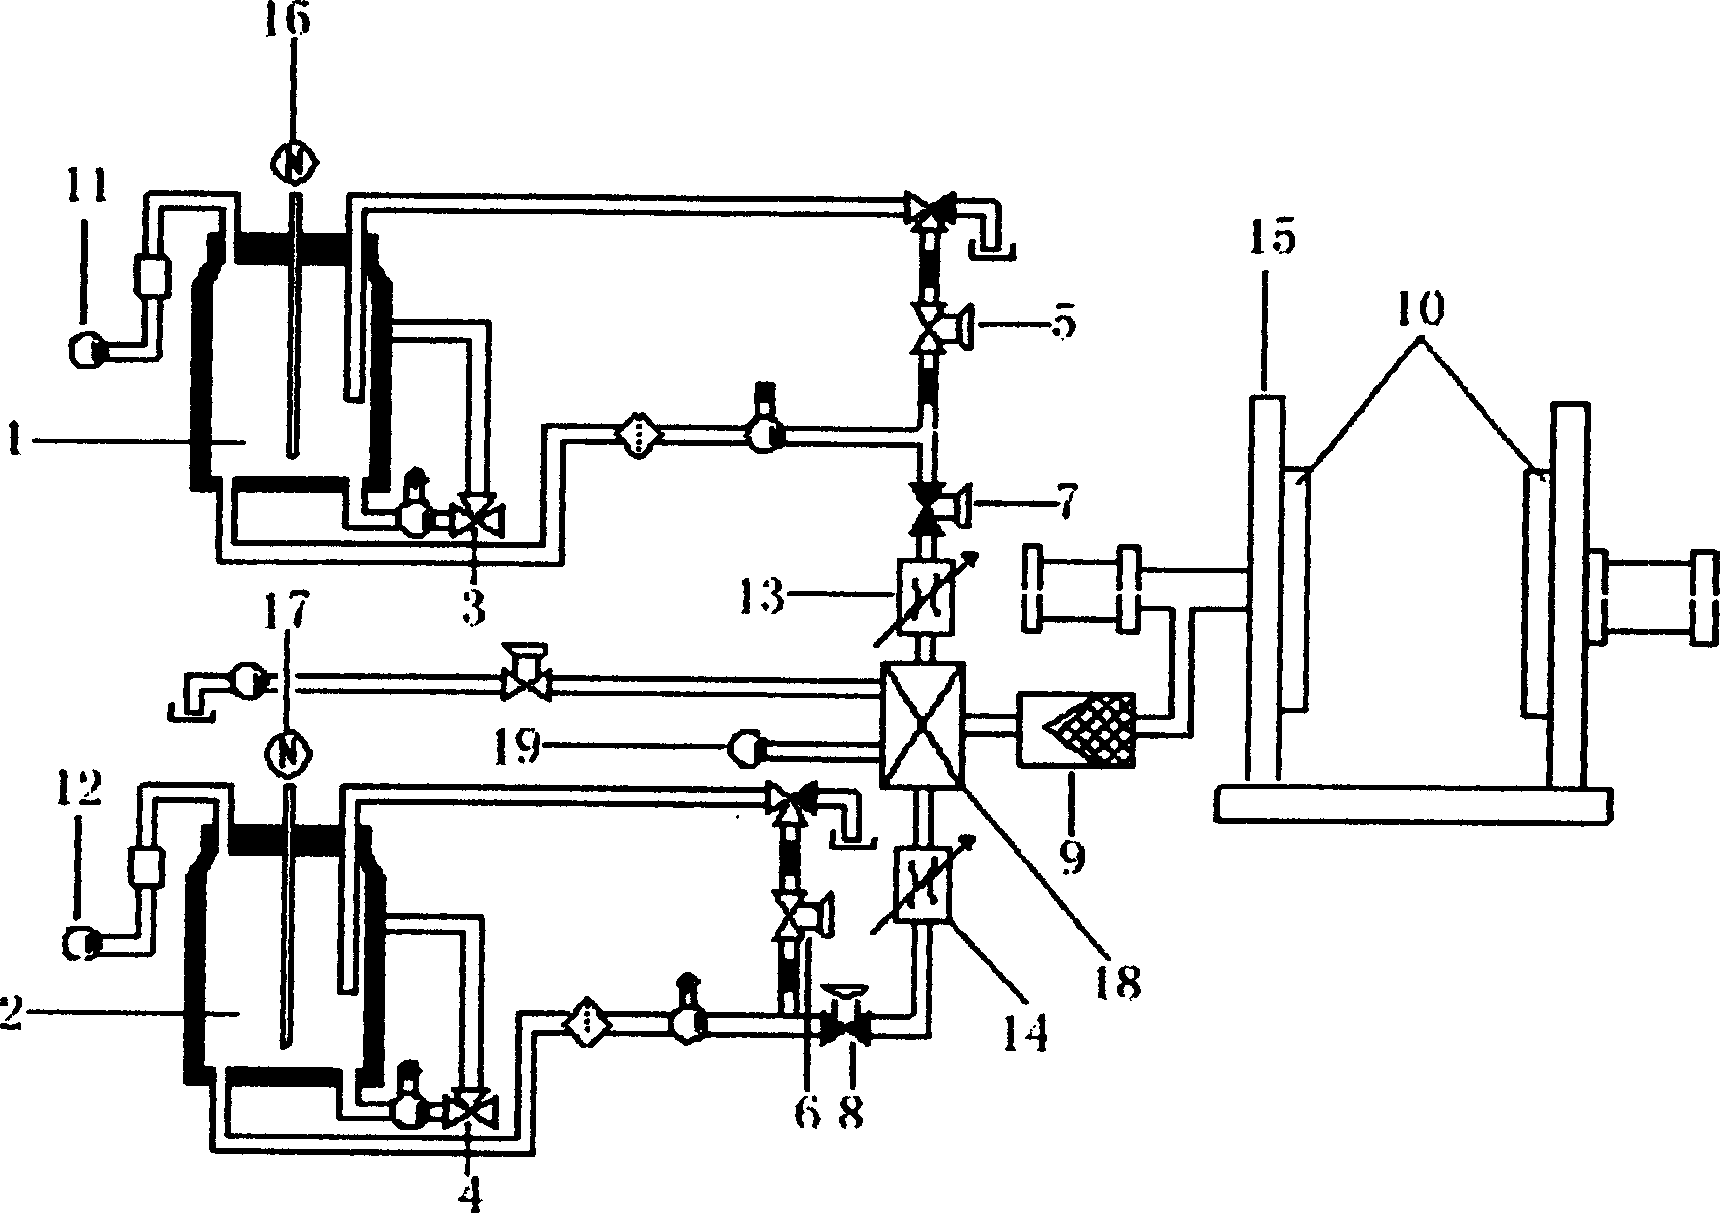
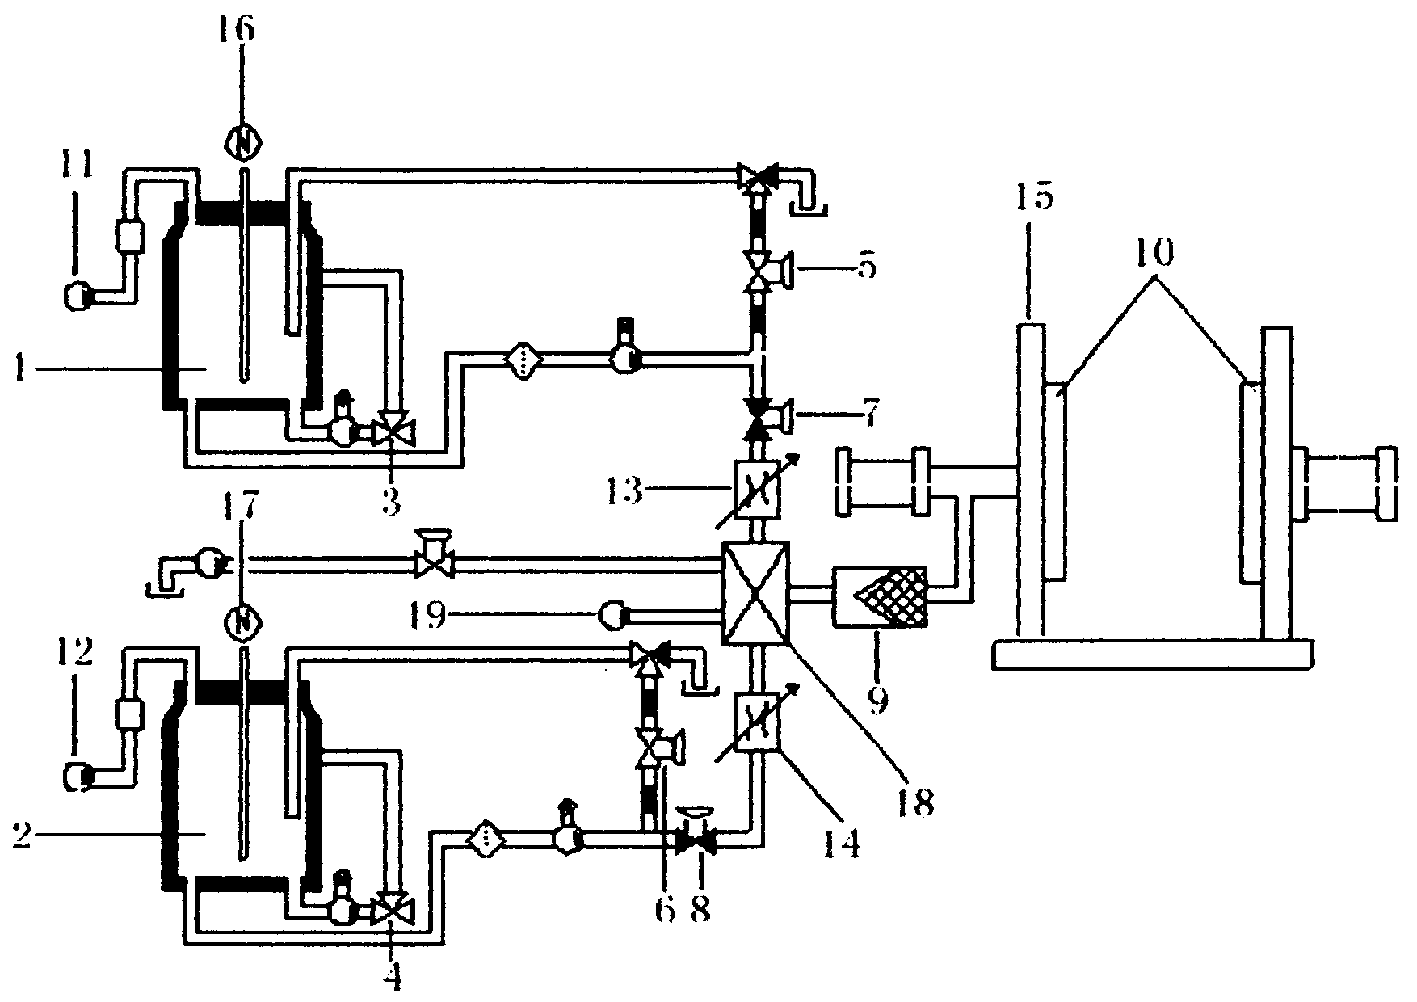
A process and apparatus for controllable fast solidification of shaped colloidal ceramics are disclosed. Said apparatus is composed of two vacuum storage tanks for different ceramic slurries, mixing system, diaphragm-type metering unit, high-pressure opposite jetting mixer, static mier, and mould. Said process includes stirring two ceramics slurries in vacuum state respectively, fostly injecting them in static mixer, high-pressure opposite jetting mixing, injecting in vacuum mould, and fast reaction and solidification. Its advantages are uniform solidifying and no internal stress.
Owner:TSINGHUA UNIV
Device for preparing large-size monodisperse uranium dioxide microspheres
InactiveCN111167387ALittle effect of gravityGood sphericityNuclear energy generationGel preparationUranium oxideMicrosphere
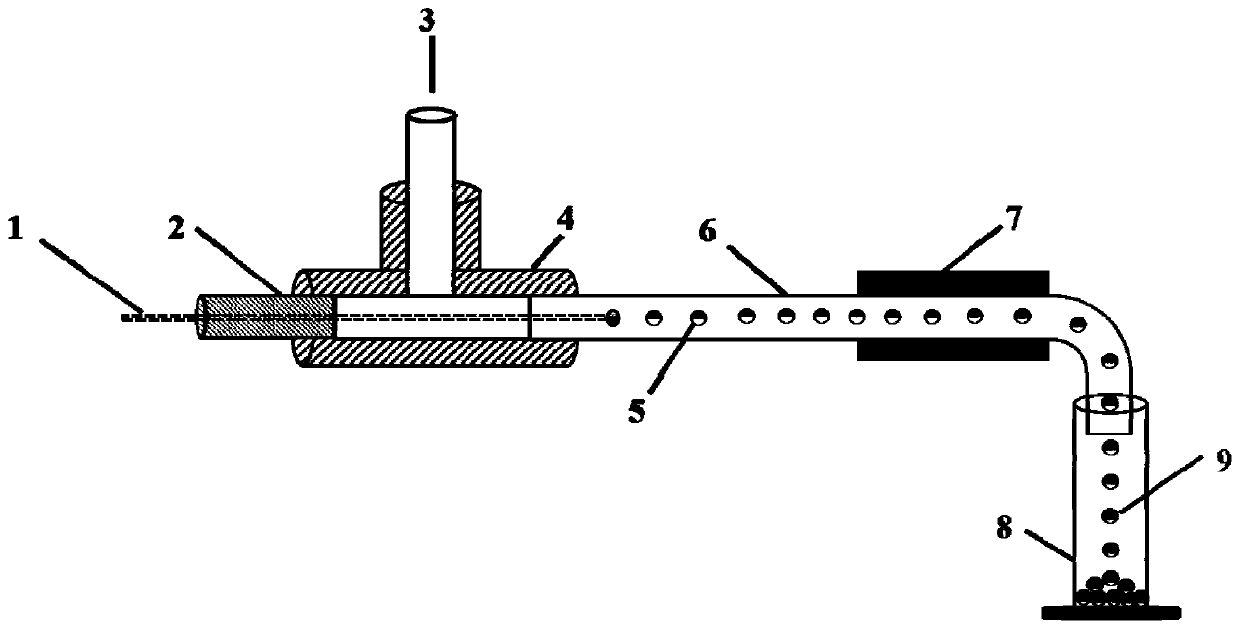
The invention relates to a device for preparing large-size monodisperse uranium dioxide microspheres, and belongs to the technical field of ceramic forming. The preparation device comprises a dispersion phase fluid inlet pipe, a continuous phase fluid inlet pipe, an outlet pipe, a T-shaped tee joint and a water bath tank;adispersionphase fluid uranium glue solution and acontinuous phase fluid silicone oil are respectivelyintroduced into the T-shaped tee joint through the dispersionphase fluid inlet pipe and the continuous phase fluid inlet pipe, and the silicone oil is adopted for shearing theuranium glue solution at the tail ends of capillary tubes, so that the uranium glue solution is crushed into liquid drops with uniform sizes one by one. The size of the outlet pipe in the T-shaped tee joint can be flexibly replaced, and therefore large-size liquid drops can be flexibly prepared by adjusting the flow of uranium glue solution and silicone oil and the size of the outlet pipe. The large liquid drops may be insufficiently cured, the outlet pipe can be placed in a temperature-controllable water bath to be pre-cured, and energy is provided for curing of the large liquid drops, so that the large-size gel microspheres with good sphericity and uniform size are obtained.
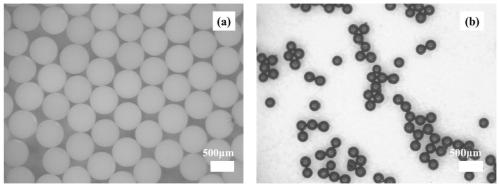
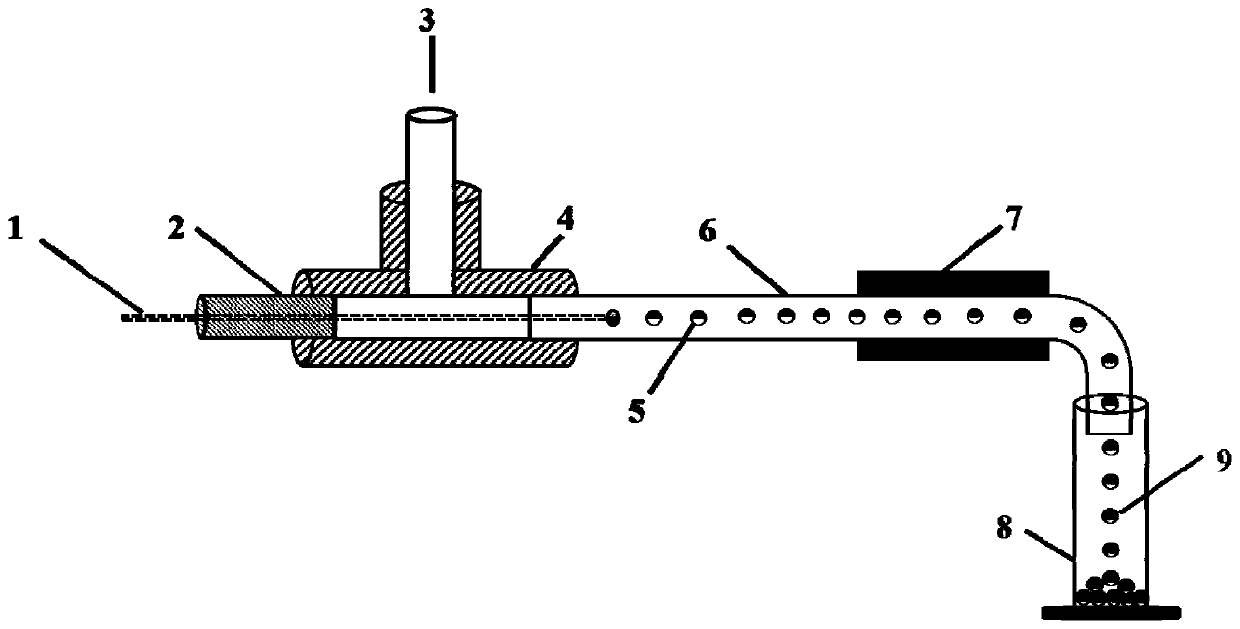
Owner:TSINGHUA UNIV
Sheet-shaped-ceramic forming device and use method thereof
ActiveCN106182337AUniform bulk densityEnsure consistent qualityMould auxillary partsAuxillary shaping apparatusAcute angleSlurry
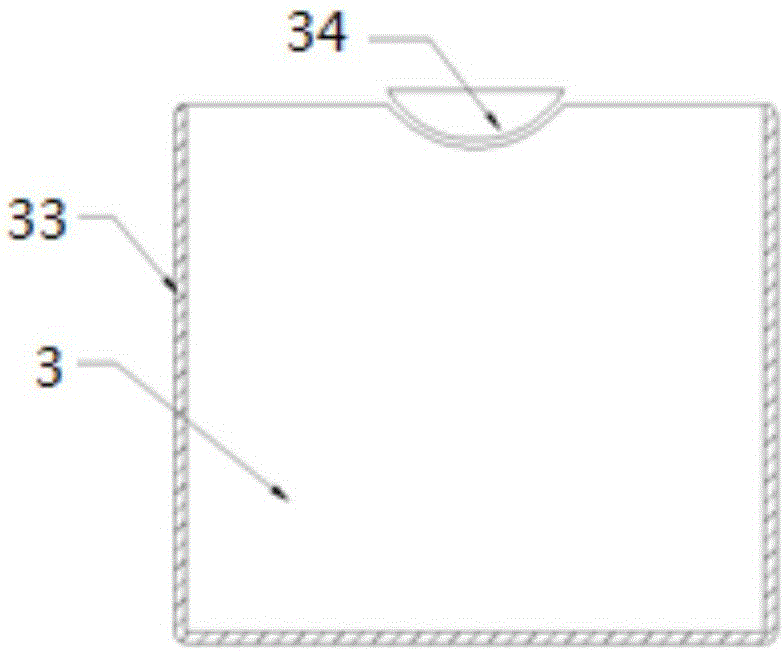
The invention discloses a sheet-shaped-ceramic forming device and a use method of the sheet-shaped-ceramic forming device and relates to the technical field of forming of sheet-shaped ceramics. The sheet-shaped-ceramic forming device and the use method of the sheet-shaped-ceramic forming device achieve the effects of guaranteeing the quality consistency of products and improving production efficiency. According to the technical scheme, the sheet-shaped-ceramic forming device comprises a base, a platform and a forming mold. The base is provided with a first end face. The platform is arranged on the base in an inclined manner. The platform is provided with a second end face and a third end face opposite to the second end face. The second end face is opposite to the first end face. An included angle between the third end face and the first end face is an acute angle. The forming mold is of a platy structure and is laid on the third end face, and ceramic slurry is poured into the forming mold in an inclined manner.
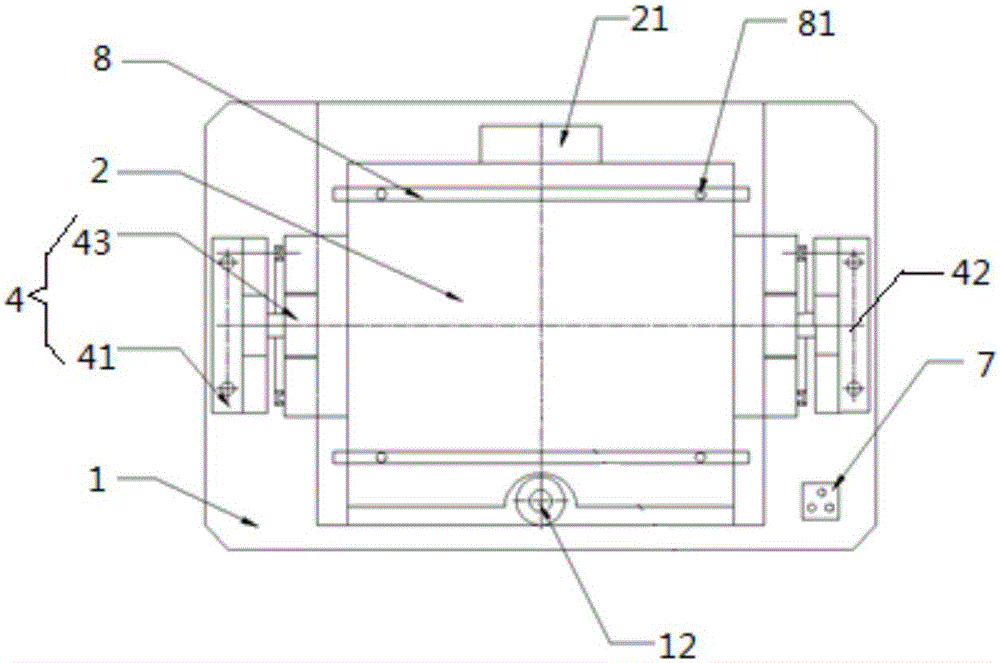
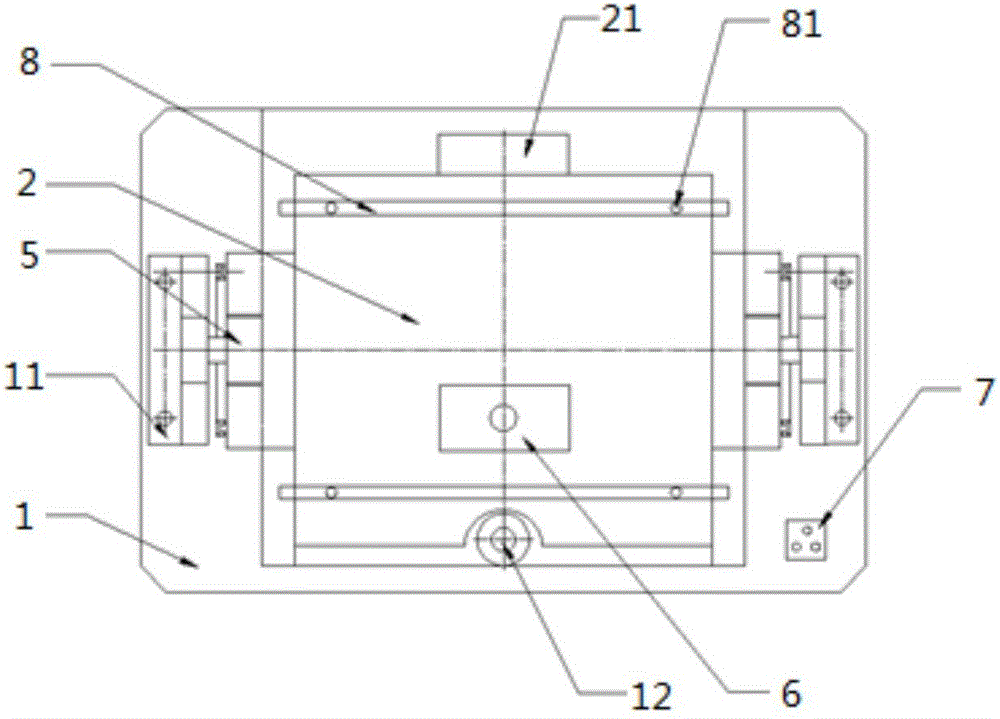
Owner:CHINA BUILDING MATERIALS ACAD
Ceramic filler forming equipment
The invention relates to the technical field of ceramic forming, in particular to ceramic filler forming equipment. Comprising a machine table, a mold plate, a supporting plate, a supporting frame, a first hydraulic cylinder, a mold cavity formed in the middle of the mold plate, a jacking column arranged below the mold cavity, a second hydraulic cylinder, a pressing block arranged at the bottom of the first hydraulic cylinder and matched with the mold cavity in shape, and a material cleaning mechanism arranged on the left side of the machine table. Wherein a second motor drives a reversing wheel to intermittently rotate by 60 degrees through a driving tooth and a convex column, so that a rotating shaft sequentially switches a material conveying block and an inner pressing plate to the position above a mold cavity, two times of filling and two times of middle compaction are achieved, ceramic powder is evenly distributed, before forming, the ceramic powder is added twice, and the ceramic powder is pressed twice in the middle of the mold cavity to form a ceramic blank; the density of the ceramic powder in the die cavity is more uniform and compact, and the problem that the middle part of a workpiece with a wide upper part and a narrow lower part is non-uniformly filled with the ceramic powder, so that the density is non-uniform, and the workpiece is layered and micro-cracked during sintering is solved.

Owner:HUAQIAO UNIVERSITY +1
Differential centrifugal ceramic forming machine
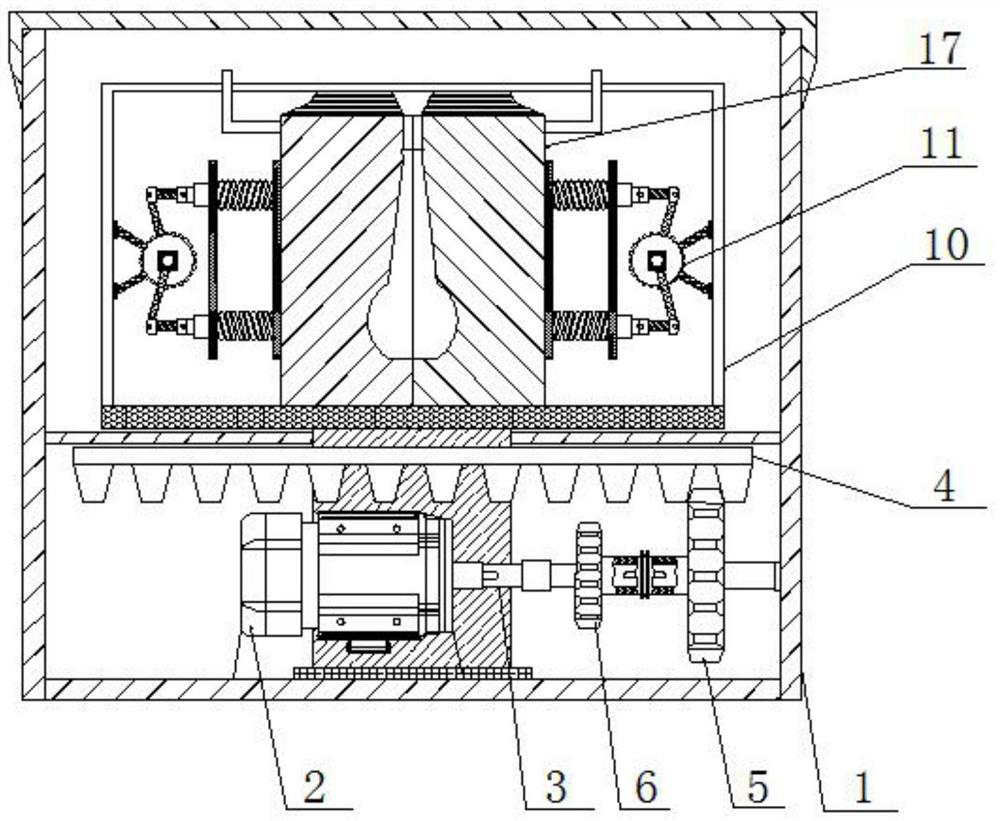
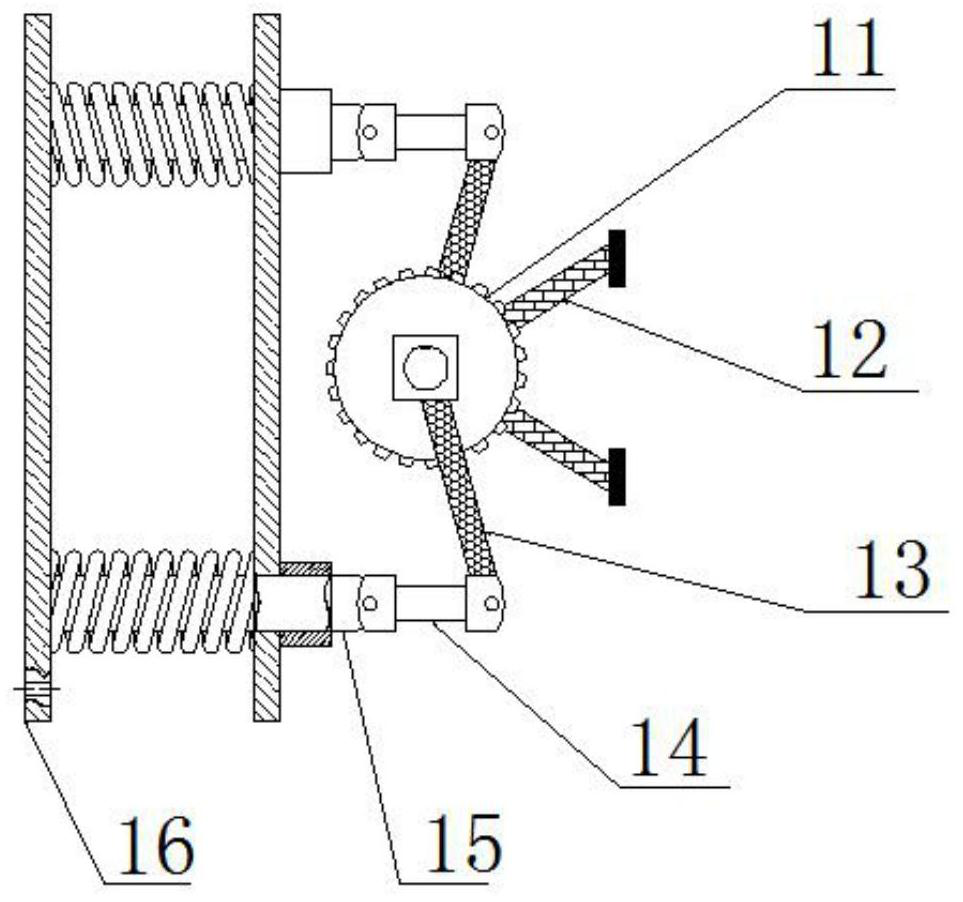
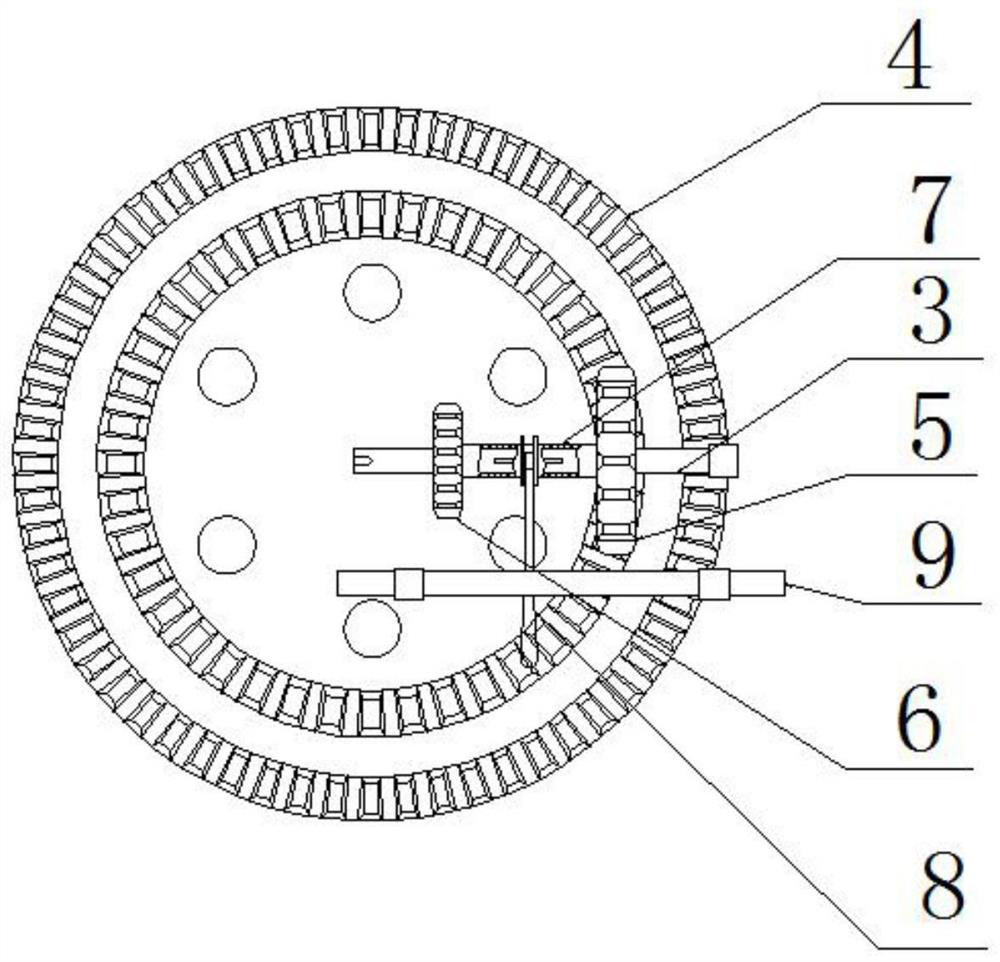
The invention relates to the technical field of ceramic forming, and discloses a differential centrifugal ceramic forming machine. The machine comprises a rack, a motor is movably connected to the inner bottom of the rack, and a driving shaft is movably connected to the right side of the motor. A shaft sleeve is movably connected to the upper surface of the driving shaft, and a high-speed gear ismovably connected to the right side of the shaft sleeve. The left side of the shaft sleeve is movably connected with a low-speed gear, and the middle of the shaft sleeve is movably connected with a paddle shift. Slurry is made to abut against the mold wall to form a compact blank through centrifugal force generated by rotation driven by a gear disc, bubbles are concentrated in the middle and finally broken out, and generation of bubbles and pinholes in a product is avoided. The slurry suction speed and the product quality are improved, few large particles can be concentrated on the surface ofthe blank due to differential centrifugation, and inconsistent shrinkage caused by uneven tissue is avoided. During mold opening, a clamping gear rotates reversely, clamping plates move outwards to pull a mold open, and the product can be taken out conveniently through mold opening under the displacement and extrusion effect of compressed air.
Owner:李慧
Manufacturing process for ceramic forming aluminum alloy mold and use method thereof
The invention belongs to the technical field of ceramic forming and particularly discloses a manufacturing process for a ceramic forming aluminum alloy mold and a use method thereof. The surface of the aluminum alloy mold is subjected to special treatment to enable contact performance between the surface of the mold and a clay blank to be similar to that of a gypsum mold. The mold can replace the gypsum mold and is used for ceramic forming, pollution of ceramic waste to the environment is reduced, forming labor intensity can be relieved, production cost is reduced, the blank forming quality is improved, and special-shaped product development and new product development and upgrading are facilitated.
Owner:醴陵市湘成陶瓷制造有限公司
Open ceramic product dry pressing forming device with automatic demolding function
InactiveCN112847740AWith automatic demoulding functionAchieve the effect of automatic demouldingDischarging arrangementRotational axisDrive wheel
The invention relates to the technical field of ceramic forming, and discloses an open ceramic product dry pressing forming device with an automatic demolding function. The open ceramic product dry pressing forming device comprises a machine frame, a motor support is fixedly connected in the machine frame, a lifting mold is connected to the outer side of the motor support in a sliding mode, and a rotating motor is fixedly connected to the upper surface of the interior of the machine frame. According to the open ceramic product dry pressing forming device with the automatic demolding function, a rotating shaft drives a connecting rod to rotate, the connecting rod drives a planet wheel to rotate, the planet wheel drives an eccentric sliding block to rotate, the eccentric sliding block drives a lifting sliding rail to move, the lifting sliding rail drives a lifting mold to move, a rotating motor drives a driving wheel to rotate, and the driving wheel drives a driven wheel to rotate. The driven wheel drives the lower bottom plate to rotate, a transmission assembly drives a lifting rotating shaft to rotate, the lifting rotating shaft drives a rotating crank to rotate, the rotating crank drives a sliding sleeve to rotate, the sliding sleeve drives a pressing block to move, and then by using the lifting mold and other mechanisms in cooperation, the effects of automatic pressing forming and rotating demolding are achieved.
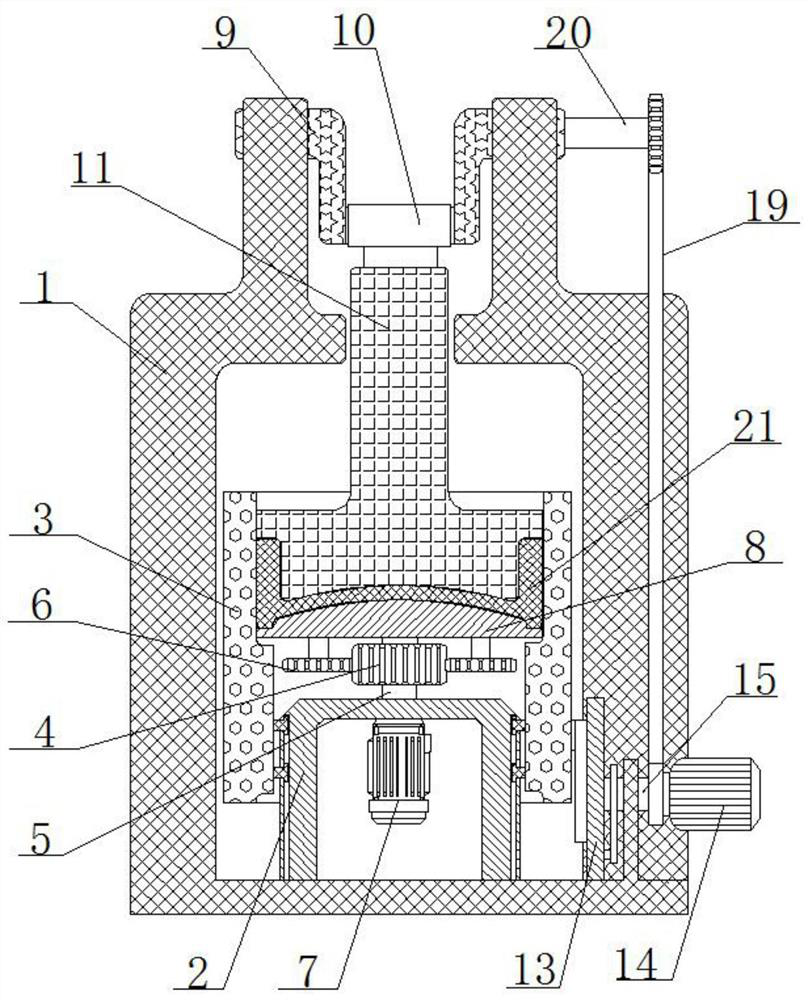
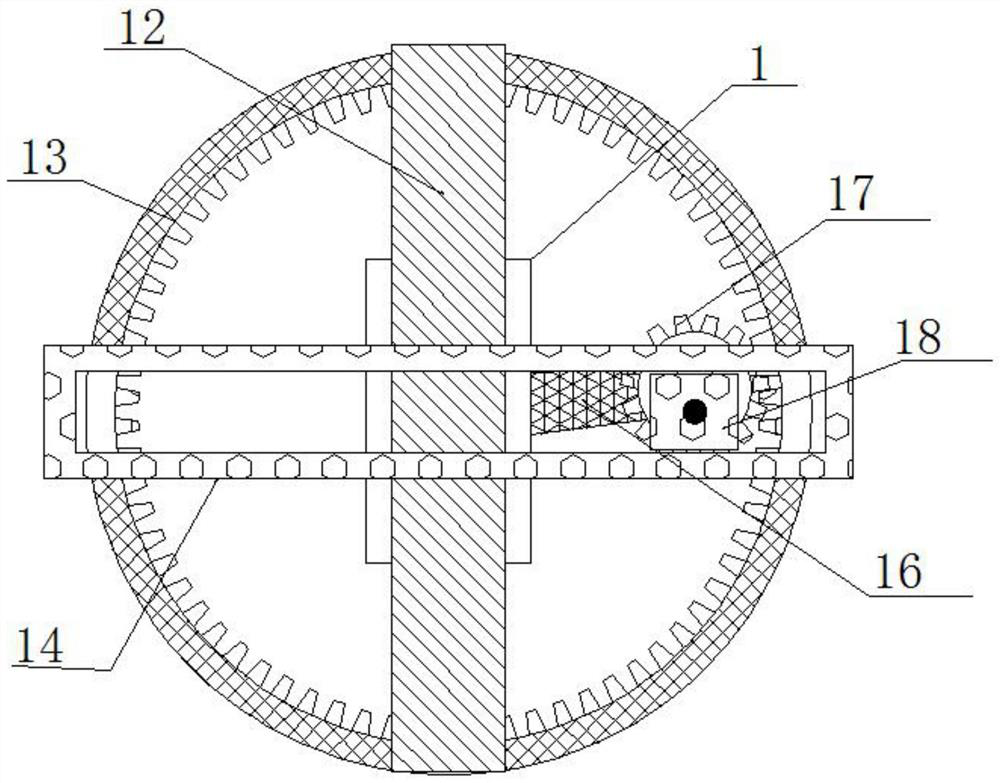
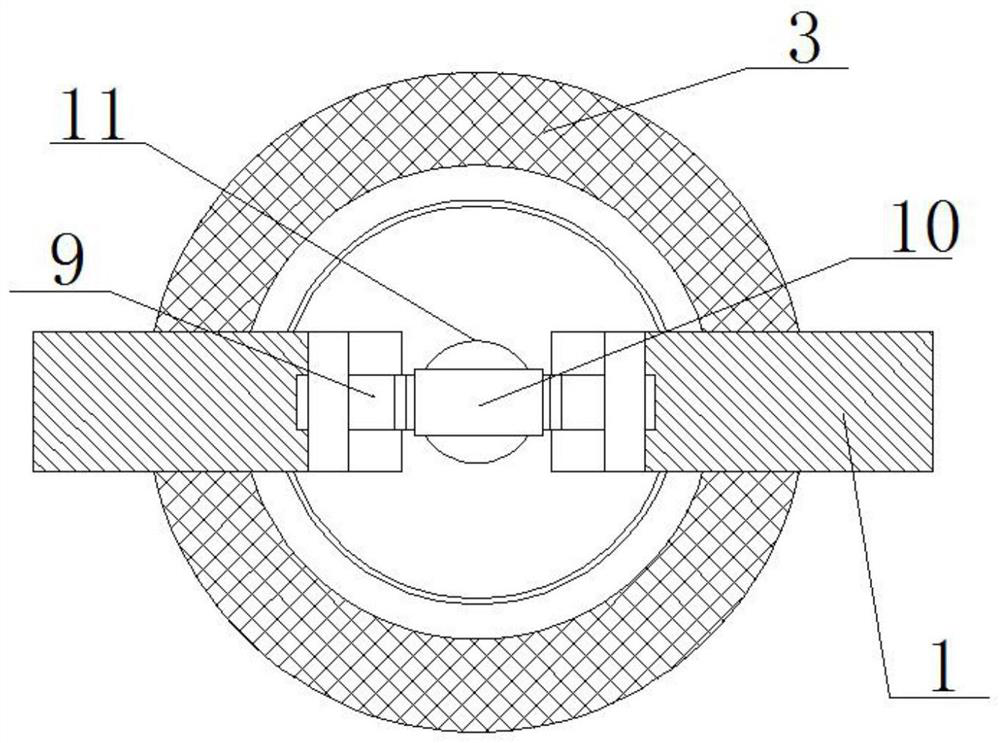
Owner:吴小冰
Ceramic production and processing device
The utility model relates to a kind of ceramic production processing device, belong to ceramic forming technical field, to solve the problem that after making blank ends, need to be taken off from the formed blank body on turntable manually, it is easy to cause blank body deformation, and after blank body is taken off, operator still need to clean up the waste material remaining on turntable manually, forming mechanism in the application includes base, waste box is inlaid and slidably arranged on base, a pair of supports is fixedly arranged on base, the top surface of two supports is commonly fixedly arranged with mud shield, drive motor is also inlaid and fixedly arranged on base, pottery wheel is fixedly connected on the output shaft of drive motor, mud shield's circumferential outer wall is fixedly provided with electric cylinder, mud shield is provided with mud scraping subassembly, and the output end of electric cylinder is fixedly connected with mud scraping subassembly.

Owner:TAICANG XIANGRUI ENVIRONMENTAL PROTECTION TECH CO LTD
Liquid phase pretreatment method for gel-casting ceramic blank before binder burning out
The present invention belongs to the field of ceramic forming technology, and is the new liquid phase pre-treatment method of degrading organic matter in biscuit to prevent cracking during eliminating glue. The ceramic biscuit after gel injection molding is liquid phase pre-treated inside water solution o ammonium persulfate or potassium persulfate before eliminating glue. Under the action of peroxide, the polymer inside the ceramic biscuit is chain breaking degraded, the netted macro molecule becomes small molecule and internal stress in the biscuit is released. The biscuit thus treated will not crack and will have no fault during overheat defatting and glue eliminating. The present invention is simple in technological process, low in cost and suitable for industrial production.
Owner:TSINGHUA UNIV
Sizing manufacturing device and method for ceramic processing
ActiveCN120516818ADischarging arrangementAuxillary shaping apparatusMechanical engineeringCeramic forming techniques
The invention relates to a shaping manufacturing device and method for ceramic machining, and relates to the technical field of ceramic molding.The shaping manufacturing device comprises a blank input system, a rack, a multi-station rotation system, a feeding system, a spray lubrication system, a rotation extrusion system and a trowelling system; the multi-station rotation system is provided with a plurality of mold rotation installation positions used for installing forming molds, the feeding system, the spray lubrication system, the rotation extrusion system and the trowelling system are installed on the machine frame in the rotation direction of the multi-station rotation system, and the blank input system is installed on the machine frame. The feeding system is installed on the side edge of the blank input system, the feeding system clamps blanks conveyed by the blank input system to a mold rotation installation position, the rotation extrusion system is provided with a spherical forming head matched with a forming mold, and a convergent container can be formed.

Owner:DEHUA HONGPENG PORCELAIN DEV CO LTD
Device and method for preparing fly ash-based foamed ceramic thermal insulation material
The invention discloses a device and method for preparing a fly ash-based foamed ceramic thermal insulation material, and relates to the technical field of foamed ceramic molding, the device comprises a roller conveyor, a mold, and a gradient material distribution assembly and a compaction assembly which are sequentially arranged along the conveying direction; the gradient material distribution assembly is arranged on the upstream portion of the roller type conveyor and comprises a material bin with two independent cavities, a reciprocating driving mechanism and a discharging control mechanism. The compaction assembly comprises a pressure oil cylinder and a jacking oil cylinder which are coaxially and vertically arranged, the pressure oil cylinder is connected with a pressing template through an angle control mechanism, the jacking oil cylinder is connected with a supporting frame through an angle control mechanism, and the pressing template is always parallel to the supporting frame; during pressing, the angle control mechanism can change the inclination angle of the pressing template and the support frame. According to the device, vertical pressing is carried out, inclined pressing is carried out by changing the angle of the pressing template, the arch bridge effect among particles is effectively destroyed, and the density uniformity of a green body is improved.


Owner:TAIYUAN UNIVERSITY OF TECHNOLOGY
Ceramic processing blank trimming device
The invention belongs to the technical field of ceramic forming, and discloses a ceramic machining blank trimming device which comprises a machining table, a backrest plate is fixedly connected to the edge of the machining table, transverse and longitudinal sliding rails are mounted on the backrest plate, and mounting plates are slidably connected to the sliding rails. The first hose plays a role in main collection, the hard pipe serves as auxiliary collection to suck a small part of dust which is not adsorbed in time and then gathers the dust into the material suction pipe, and in the high-speed rotation process of the elbow pipe, air in the material suction pipe can be discharged out of the elbow pipe in a continuously accelerated mode, so that a strong air pressure difference is formed inside and outside the material suction pipe, and the material suction efficiency is improved. Therefore, the air inlet rate of the bottom of the material suction pipe is greatly increased, the suction effect is achieved, dust pollution is effectively reduced, the pressure difference is generated through the elbow pipe, negative pressure is generated inside and outside the pipe through rapid air flowing, a fan does not need to be used for exhausting air, and the operation stability of the device is improved.

Owner:GUANGZHOU COLLEGE OF COMMERCE
Testing method of ceramic suspended matter gelating point and device
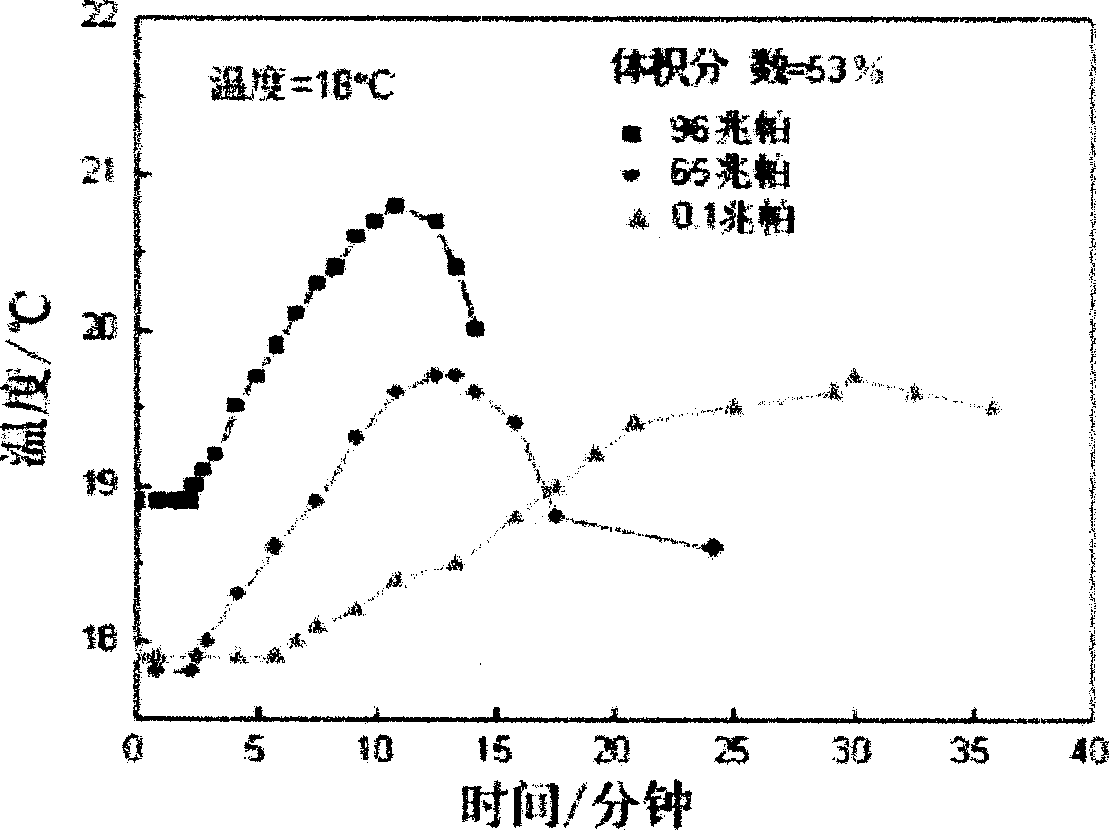
A method and apparatus for measuring the coagulating point of ceramic suspension are based on the principle that the coagulation in situ of ceramic suspension can be induced by heat releasing and external pressure. Said method includes preparing the slurry of ceramic suspension, loading the slurry in mould, putting the pressure applying head and temp sensor in said slurry while attaching pressure sensor to bottom of mould, applying pressure to the slurry, acquiring the data, processing the data by computer program, drawing the relation curve between pressure, temp and coagulating point, and determining the initial coagulating point.
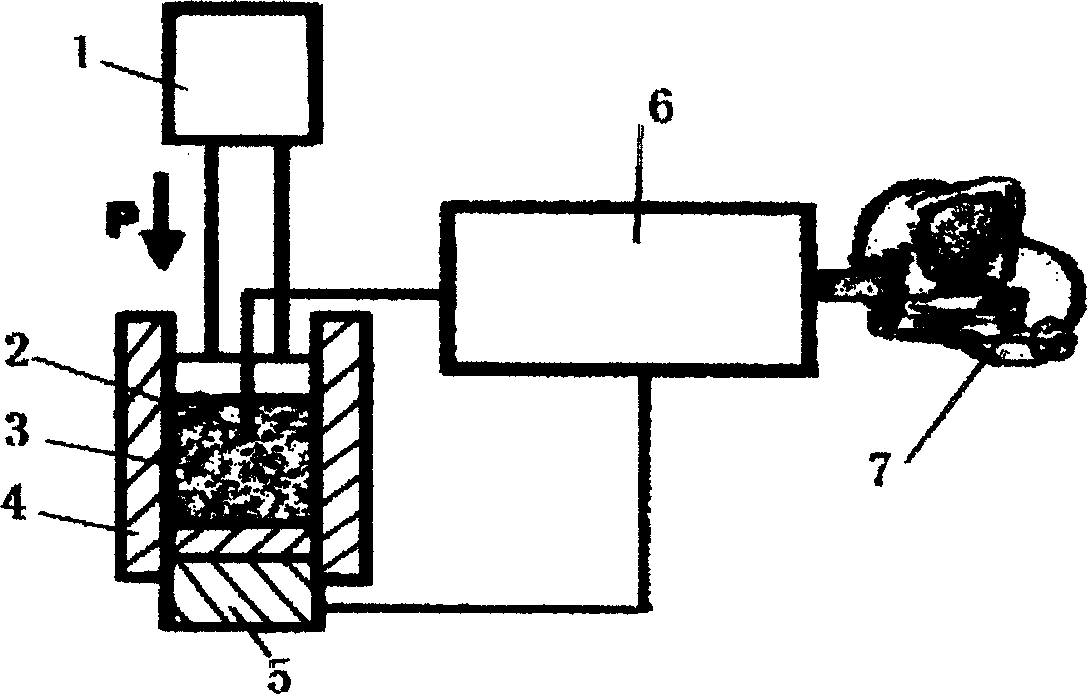
Owner:TSINGHUA UNIV
Novel vacuum degassing method for gelcasting ceramic slurry
Owner:TSINGHUA UNIV
Porous ceramic, preparation method thereof and atomizing core
The invention belongs to the technical field of porous ceramic forming, and relates to porous ceramic, a preparation method thereof and an atomizing core. The preparation method of the porous ceramic comprises the following steps: uniformly mixing magnesium oxide, aluminum hydroxide, silicon dioxide aerogel, graphite powder, glass powder and boric oxide to obtain mixed powder; uniformly mixing the mixed powder with a dispersing agent, a plasticizer, a binder and deionized water to obtain slurry; forming the slurry into a ceramic green body by adopting a tape casting method; the ceramic green body is dried, degummed and sintered, and the porous ceramic is obtained. The porous ceramic prepared by the invention is flat in surface, uniform in pore size distribution and beneficial to taste reduction; the characteristics of relatively high breaking strength, low thermal expansion coefficient and low thermal conductivity are realized; in addition, the through hole ratio and the porosity are effectively improved.

Owner:SHENZHEN JIJIA NEW MATERIAL TECH CO LTD
Special mold for ceramic blank high-pressure slip casting process
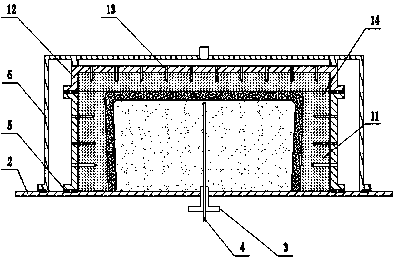
The invention belongs to the technical field of ceramic molding, and in particular relates to a molding mold for sanitary ceramic blanks; it includes an outer mold and a support plate for sealing the outer mold, and is characterized in that: the outer mold includes a water-absorbing and air-permeable K plaster mold and is arranged on K The steel sleeve of the outer wall of the plaster mold, the steel sleeve is provided with air vents, and the support plate is provided with a grouting port and an air injection port; the special mold for the high-pressure grouting molding process of ceramic blanks adopting the technical solution of the present invention, the strength High is not easy to be damaged by high pressure, and can be permeable and breathable.
Owner:重庆国之四维卫浴有限公司
Grouting process
PendingCN113815091AHigh densityQuality improvementCeramic shaping apparatusSlurryCeramic forming techniques
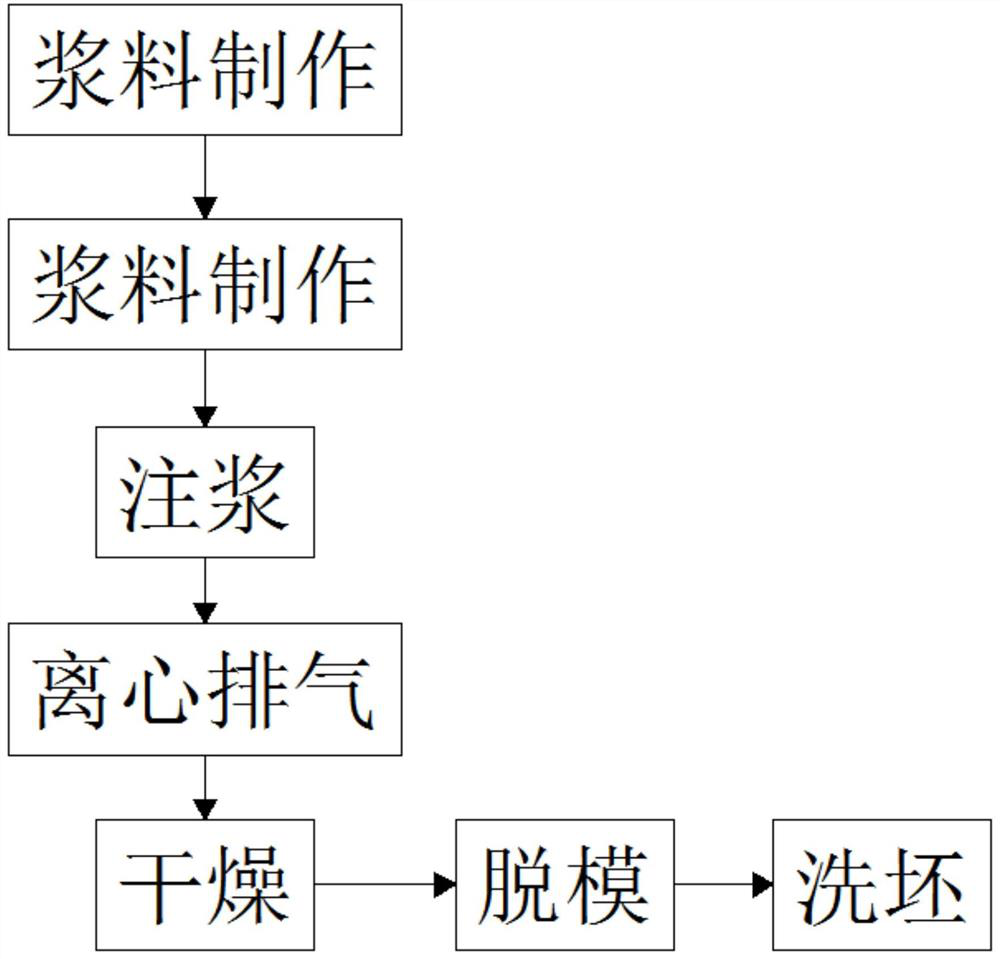
The invention relates to the technical field of ceramic forming, and discloses a grouting process. The process comprises the following steps: step 1, slurry preparation: uniformly mixing and stirring various raw materials according to a ratio to prepare raw material slurry; step 2, mold assembling: selecting a corresponding mold, closing the mold, and then integrally mounting and fixing the mold on a turntable of a centrifugal machine; step 3, grouting, injecting the raw material slurry prepared in the step 1 into a mold cavity of the mold in the step 2 through compressed air pressurization equipment; and 4, centrifugal exhausting: separating a grouting opening of the mold from the compressed air pressurization equipment, and sealing the grouting opening of the mold. According to the grouting process, through the manner of combining pressure grouting and centrifugation, the compactness of a blank can be greatly improved, bubbles and air holes in the blank can be reduced, and the quality of the prepared blank is effectively improved.
Owner:ANHUI PROVINCIAL HANSHAN MINSHENG PORCELAIN
A shaping device and method for ceramic processing
ActiveCN120516818BDischarging arrangementAuxillary shaping apparatusMechanical engineeringCeramic forming techniques
The present invention relates to a shaping production device and method for ceramic processing, and relates to the field of ceramic forming technology. The device comprises a blank input system, a frame, a multi-station rotary system, a feeding system, a spray lubrication system, a rotary extrusion system and a smoothing system. The multi-station rotary system is rotatably installed on the frame. The multi-station rotary system has a plurality of mold rotary mounting positions for mounting forming molds. The feeding system, the spray lubrication system, the rotary extrusion system and the smoothing system are installed on the frame along the rotation direction of the multi-station rotary system. The blank input system is installed on the frame. The feeding system is installed on the side of the blank input system. The feeding system clamps the blank conveyed by the blank input system to the mold rotary mounting position. The rotary extrusion system has a spherical forming head adapted to the forming mold, and can realize the forming of a narrow-mouthed container.

Owner:DEHUA HONGPENG PORCELAIN DEV CO LTD
A kind of sheet ceramic forming device and using method thereof
ActiveCN106182337BUniform bulk densityEnsure consistent qualityMould auxillary partsAuxillary shaping apparatusCeramic moldingAcute angle
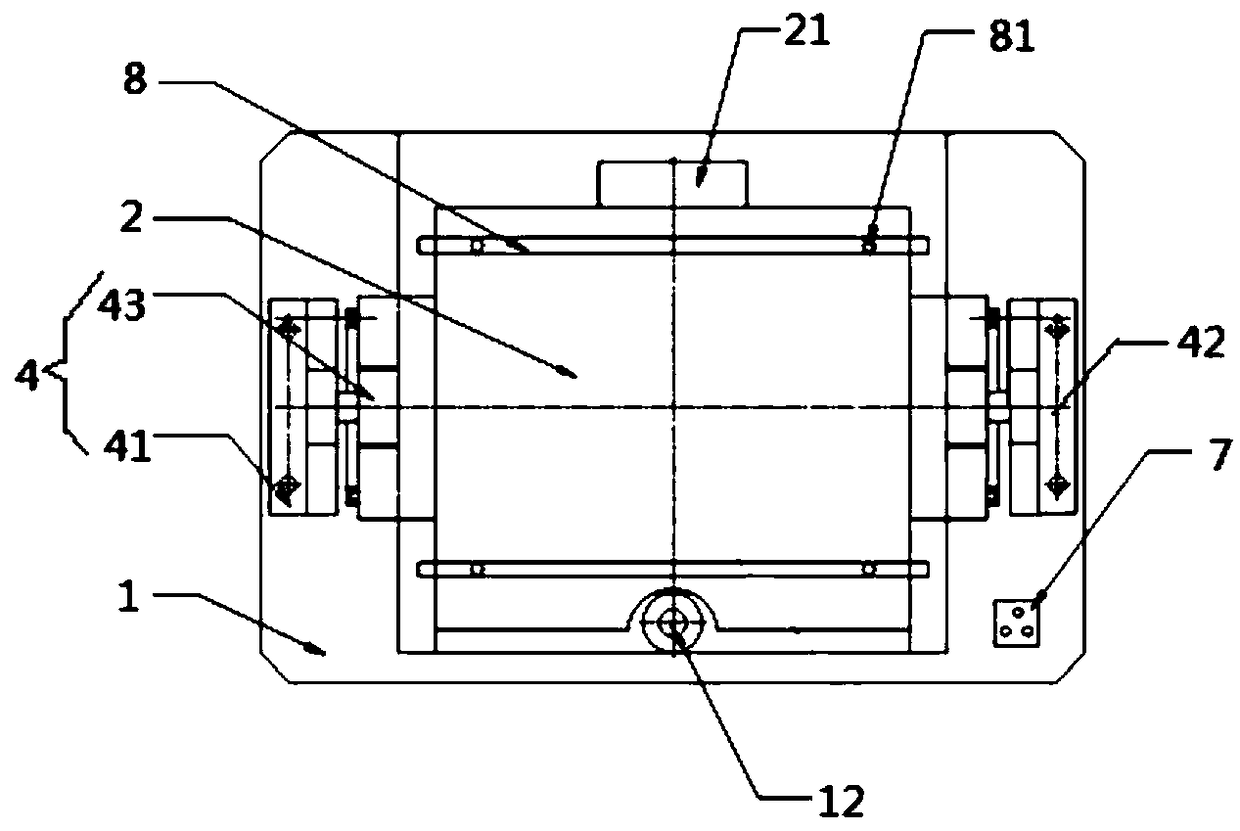
The invention discloses a sheet-shaped-ceramic forming device and a use method of the sheet-shaped-ceramic forming device and relates to the technical field of forming of sheet-shaped ceramics. The sheet-shaped-ceramic forming device and the use method of the sheet-shaped-ceramic forming device achieve the effects of guaranteeing the quality consistency of products and improving production efficiency. According to the technical scheme, the sheet-shaped-ceramic forming device comprises a base, a platform and a forming mold. The base is provided with a first end face. The platform is arranged on the base in an inclined manner. The platform is provided with a second end face and a third end face opposite to the second end face. The second end face is opposite to the first end face. An included angle between the third end face and the first end face is an acute angle. The forming mold is of a platy structure and is laid on the third end face, and ceramic slurry is poured into the forming mold in an inclined manner.
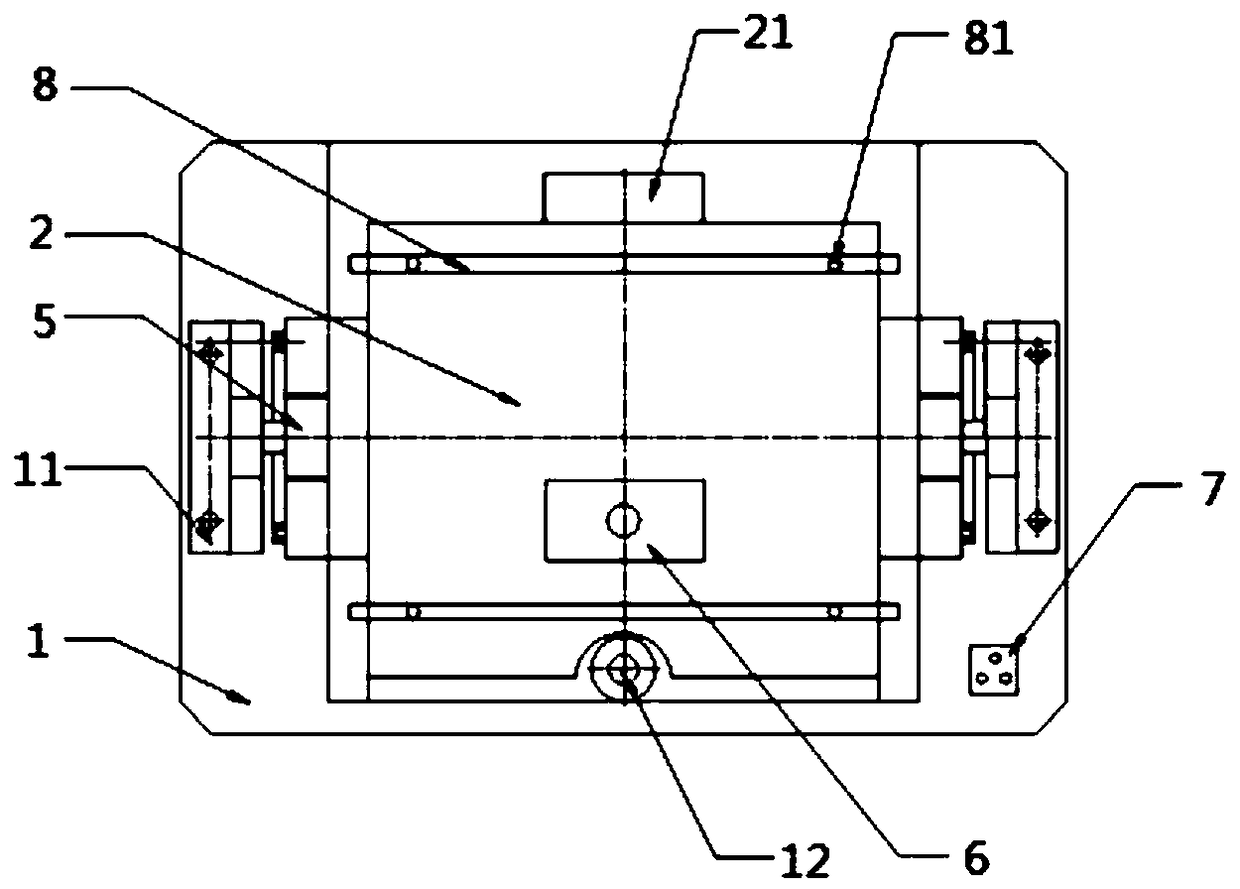
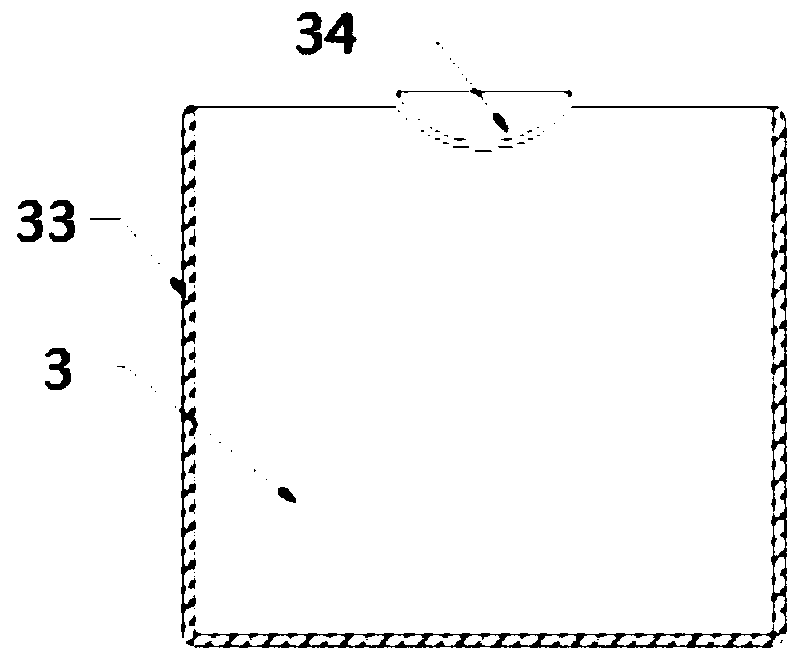
Owner:CHINA BUILDING MATERIALS ACAD
Blank turning machine and blank production line
PendingCN111823384AGuaranteed integrityIncrease productivityCeramic shaping plantsAuxillary shaping apparatusProduction lineCeramic molding
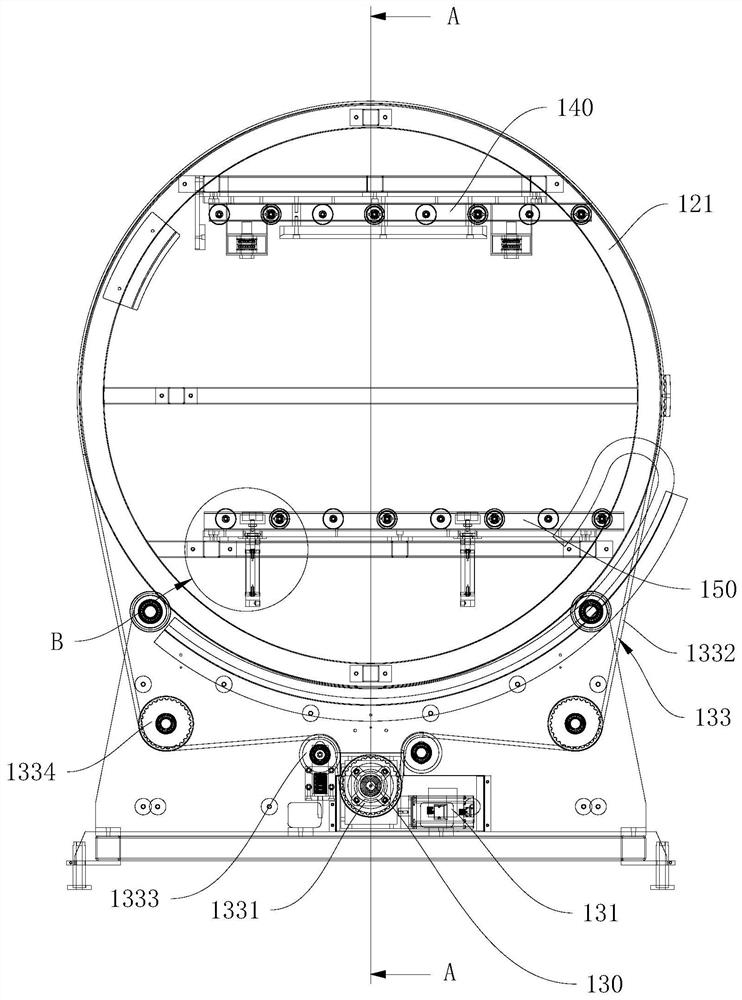
The invention relates to a blank turning machine and a blank production line, and belongs to the technical field of ceramic molding. The invention proposes a blank turning machine, and the blank turning machine comprises a base, a rotating stand, a rotating drive device, a first conveying line, a second conveying line and a compression device, wherein the rotating stand is rotationally supported on the base; the rotating drive device is installed on the base, and the rotating drive device can drive the rotating stand to rotate; the first conveying line and the second conveying line are parallel to each other and arranged in the rotating stand up and down at intervals; the compression device is installed in the rotating stand, the compression device is used to match with the first conveyingline to compress a blank together when the rotating stand is in a feeding position, and the compression device is used to place the blank on the second conveying line when the rotating stand is in adischarging position. The invention also proposes a blank production line, and the blank production line comprises the above blank turning machine. The blank turning machine is used on the blank production line, the blank can be automatically loaded and unloaded, the loading direction and the unloading direction are parallel to each other, the blank is automatically fed in and out, and the integrity of the blank can also be ensured.
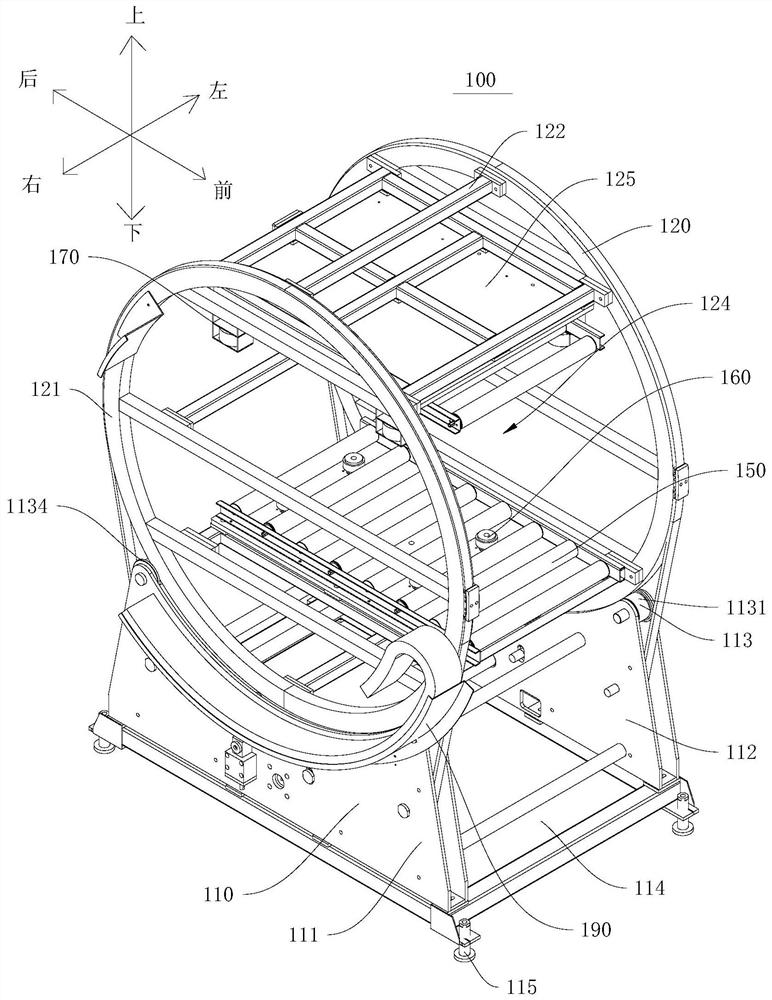
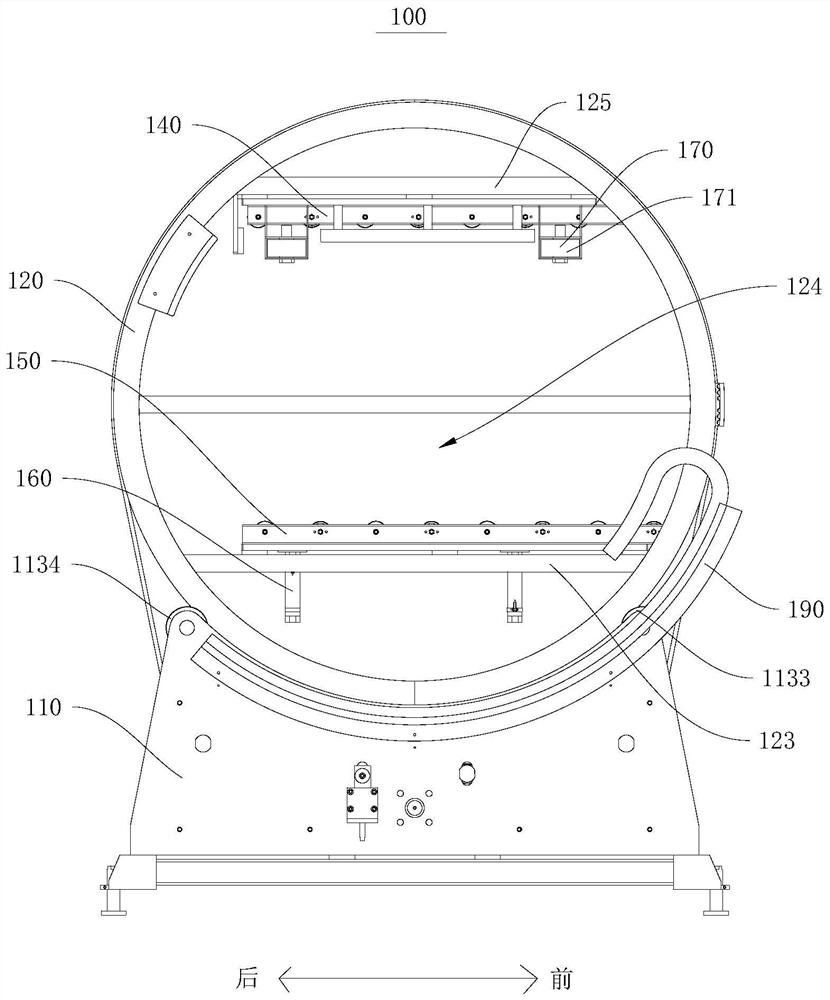
Owner:广东金马领科智能科技有限公司
Rapid forming convenient demolding mechanism for long-neck ceramic product
ActiveCN112356222AAchieve manual precision cuttingAchieve the effect of rotary demouldingDischarging arrangementCeramic shaping mandrelsGear wheelElectric machinery
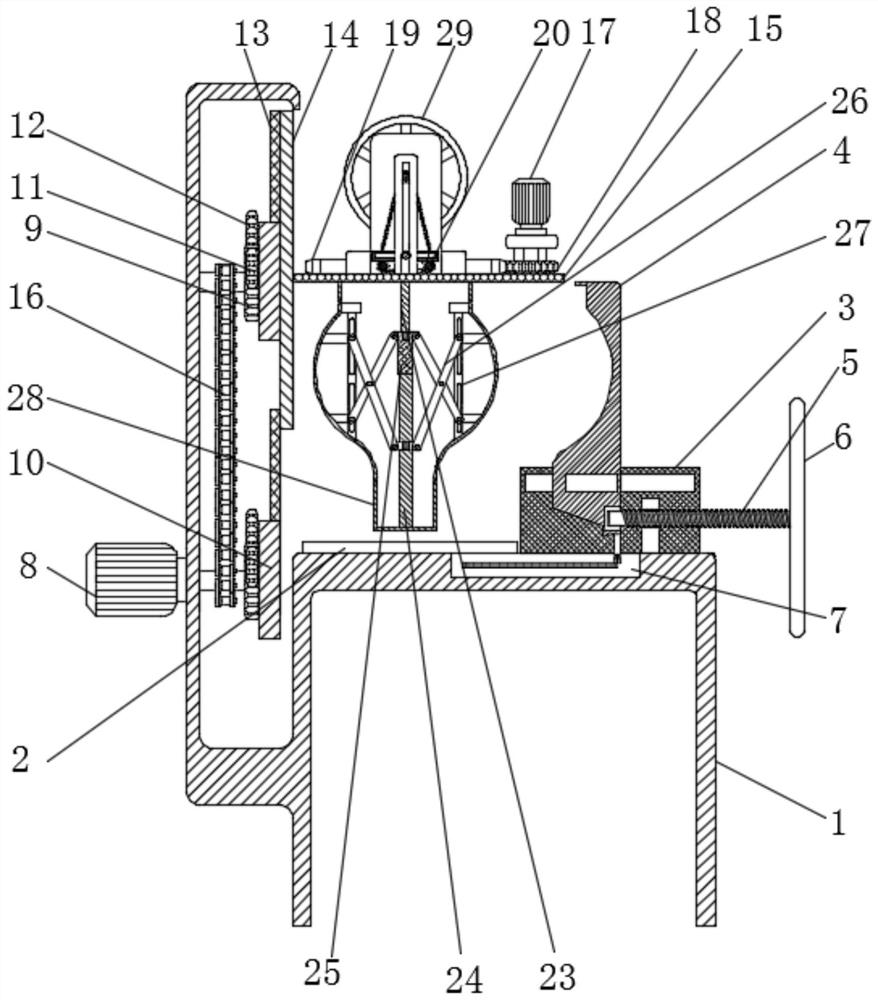
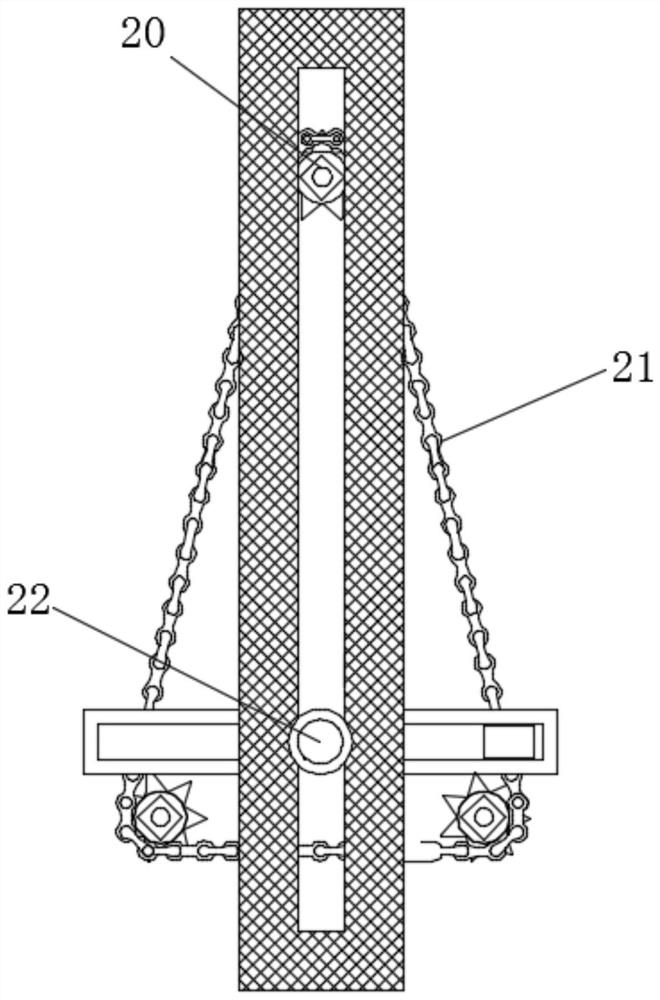
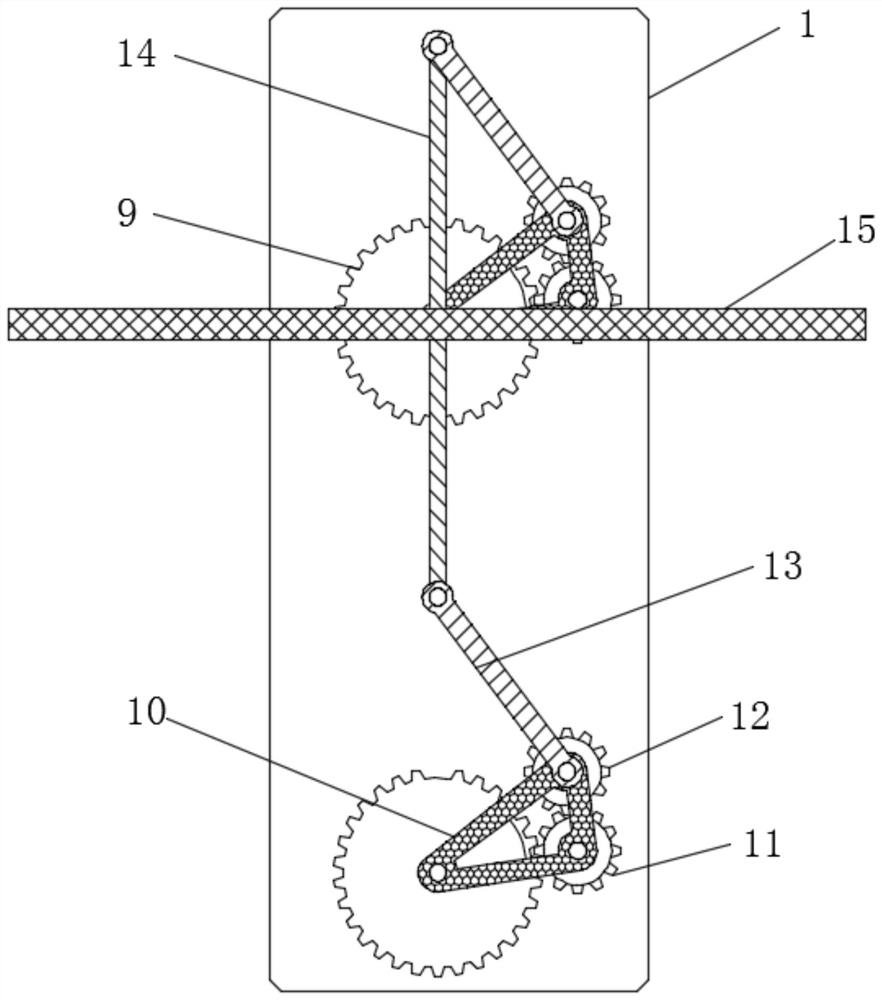
The invention relates to the technical field of ceramic forming, and discloses a rapid forming convenient demolding mechanism for a long-neck ceramic product. The rapid forming convenient demolding mechanism for the long-neck ceramic product comprises a rack; a deck plate and a horizontal sliding groove are fixedly connected to the top of the rack; an indication plate is fixedly connected to the front surface of the rack; and a feeding screw rod is rotationally connected to the top of the rack. According to the rapid forming convenient demolding mechanism for the long-neck ceramic product, a feeding screw rod is driven to rotate through a rotating flange, the feeding screw rod drives a cutting plate to move, and a manual precise cutting effect is achieved through cooperative use of mechanisms such as a horizontal sliding groove, an indicating plate and a fixing mold; and a telescopic lifting rod is driven to move through a lifting flange, the telescopic lifting rod drives a tensioningrod to rotate, the tensioning rod drives the fixing mold to contract, a lifting motor drives a lifting plate to rotate, the lifting plate drives a rotary transmission wheel to move upwards, the rotarytransmission wheel drives the fixing mold to move upwards, and then the automatic contracting, lifting and demolding effect is achieved through cooperative use of mechanisms such as a driving gear.
Owner:QICHUN MINGYAO POTTERY CO LTD
A ceramic filler forming apparatus
The application relates to the technical field of ceramic forming, in particular to a ceramic filler forming equipment, which comprises a machine table, a mold plate, a supporting plate, a supporting frame, a first hydraulic cylinder, a mold cavity arranged in the middle of the mold plate, a top column arranged below the mold cavity, a second hydraulic cylinder, a pressing block arranged at the bottom of the first hydraulic cylinder and matched with the shape of the mold cavity, and a material cleaning mechanism arranged at the left side of the machine table, wherein a second motor drives a reversing wheel to rotate intermittently by 60 degrees through a driving gear and a convex column, the rotating shaft switches a feeding block and an inner pressing plate to above the mold cavity in sequence, twice filling and twice intermediate compaction are realized, ceramic powder is uniformly distributed, ceramic powder is added twice before forming, ceramic powder in the middle position of the mold cavity is pressed twice, a ceramic blank is formed, the density of ceramic powder in the mold cavity is more uniform and compact, the problem that the density of ceramic powder in the middle position of a workpiece with a wide upper part and a narrow lower part is not uniform, which leads to layer cracking and micro-cracks of the workpiece during sintering, is solved.

Owner:HUAQIAO UNIVERSITY +1