
Patents
Literature
103results about "Forge furnaces" patented technology
Efficacy Topic
Property
Owner
Technical Advancement
Application Domain
Technology Topic
Technology Field Word
Patent Country/Region
Patent Type
Patent Status
Application Year
Inventor
Local thickening equipment for middle of drill pipe body
The equipment comprises a heating furnace, an opening is formed in one side of the heating furnace, a die forging furnace is arranged in front of the opening at intervals, transmission chains extending to the two sides of the die forging furnace are arranged on the two sides of the opening of the heating furnace, and pipe body deformation restraining pipes are arranged on the portions, located above the two transmission chains, of the two sides of the die forging furnace correspondingly. The two pipe body deformation restraining pipes are coaxially arranged, the ends, away from the die forging furnace, of the two pipe body deformation restraining pipes are connected with a stopping base and a power base respectively, and one side of the stopping base is coaxially connected with an easily-drilled metal rod stretching into an inner hole of a drill pipe body in the die forging furnace through a connecting rod. Compared with an existing drill rod with an anti-abrasion sleeve additionally arranged in the middle of a pipe body, the drill rod is safer and more reliable in use, and the service life of the pipe body of the drill rod is prolonged; meanwhile, compared with a drill rod with a thickened middle formed by turning a thick-wall round pipe, a large number of steel material resources can be saved, the production cost is reduced, and the production efficiency is improved.

Owner:CHINA NAT PETROLEUM CORP +2
Medium-frequency induction heating furnace body, furnace body manufacturing method and temperature control method
PendingCN111761020AImprove temperature measurement accuracySimple manufacturing processLinings repairForge furnacesEngineeringHeating furnace
The invention relates to the technical field of medium-frequency induction heating furnaces, in particular to a medium-frequency induction heating furnace body, a furnace body manufacturing method anda temperature control method. The medium-frequency induction heating furnace body comprises a furnace lining, a material channel allowing a blank to pass through is formed in the middle of the furnace lining, and an induction coil which extends in axial direction of the material channel and is spirally wound on outer side of the material channel is arranged in the furnace lining; and a pluralityof temperature measuring holes are formed in the side wall of the furnace lining in the axial direction of the furnace lining at intervals, the temperature measuring holes are formed in the radial direction of the furnace lining and penetrate through the side wall of the furnace lining, and the temperature measuring holes are located at the intervals between every two adjacent turns of coils of the induction coil. The invention further provides a manufacturing method of the medium-frequency induction heating furnace body and a temperature control method of the medium-frequency induction heating furnace. According to the furnace body, the temperature measuring holes are formed in the side wall of the furnace body for temperature measurement instead of adopting the temperature measurement mode at a discharge port so that the temperature measurement accuracy can be improved.
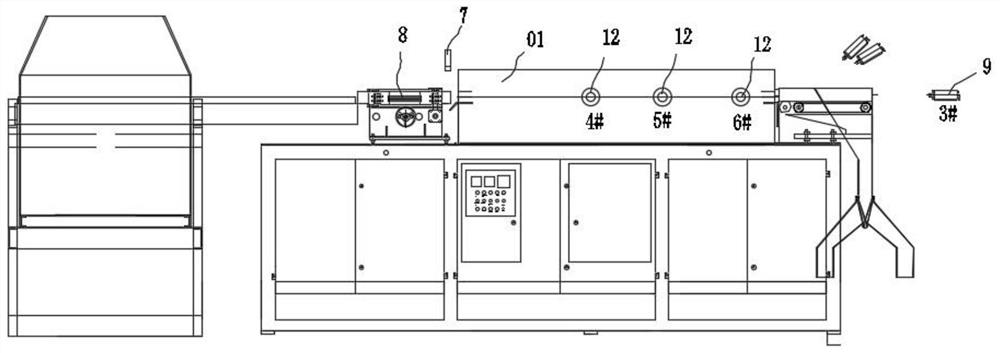
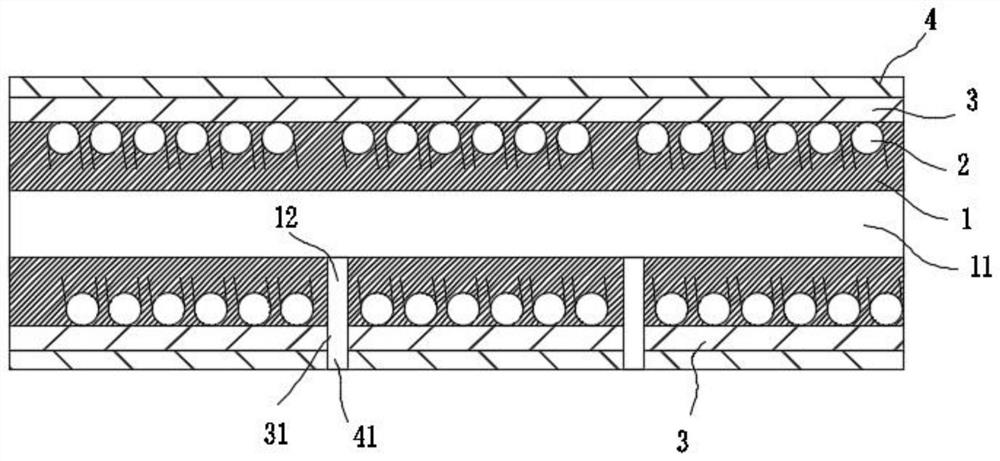
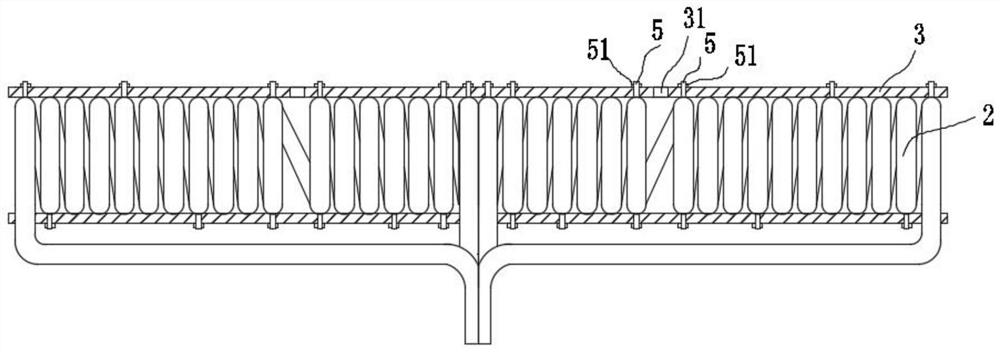
Owner:HANGZHOU KEYUAN ELECTRIC FURNACE CO LTD
Ultrahigh-hardness high-purity stainless steel forging equipment and process
PendingCN121423520AForging press detailsForging/hammering/pressing machinesTemperature controlSS - Stainless steel
The invention discloses ultrahigh-hardness and high-purity stainless steel forging equipment and process, and relates to the field of stainless steel forging.The ultrahigh-hardness and high-purity stainless steel forging equipment comprises a heating furnace and a rotary supporting seat, a first roller conveying belt and a second roller conveying belt are installed on the two sides of the heating furnace correspondingly, and a first door assembly is installed on one side of the heating furnace; a second door assembly is mounted on the other side of the heating furnace; the top of the rotary supporting base is rotationally connected with a cooling station, a hydraulic lifting rod is installed in the center of the top of the rotary supporting base, and an electric chuck is installed at the other end of the hydraulic lifting rod. According to the ultrahigh-hardness high-purity stainless steel forging equipment and process, the temperature control and cooling process is optimized, and the final mechanical property of a product is ensured. The heating resistance wire is accurately controlled through the mechanical thermostat, the heating temperature is stabilized within the accurate range of 1000 + / -20 DEG C, the heat preservation time is set according to the thickness of a workpiece, and reliable guarantee is provided for the austenitizing process.

Owner:GUOXIN ULTRA HIGH PURITY (JIANGSU) MATERIALS CO LTD
Composite forging device and metal lamination equipment using the same
A composite forging device includes a connecting component, a heating module and a forging module. The heating module is connected to the connector and includes a heater. The forging module is connected to the connector and includes a forger. The heater and the forger are disposed opposite each other.

Owner:IND TECH RES INST
Heating furnace for forgings
The heating furnace comprises a heating furnace body, a through hole is formed in the front side of the top end of the heating furnace body, a furnace door is assembled in an inner cavity of the through hole, sliding grooves are symmetrically formed in the left side and the right side of the furnace door, and one ends of guide blocks are symmetrically arranged on the left side and the right side of the through hole; and hydraulic cylinders are connected to the left side and the right side of the top end of the heating furnace through screws, and the output ends of the upper surfaces of the hydraulic cylinders are fixedly connected to the outer wall of the furnace door. The device is simple in structure and reasonable in design, the temperature in the furnace chamber can be locked when the furnace door is opened, temperature loss is reduced to the maximum extent, energy is saved, waste is avoided, the stability of heating in the furnace can be improved, the quality of machined forgings is remarkably improved, and the production cost is reduced. In addition, thermal stress change is reduced, a furnace body, a heating element and the like can be protected, the service life is prolonged, use is flexible, practicability is high, and the use requirement on the existing market is met.

Owner:ACHENG XINHE POWER STATION FITTINGS CO LTD
Pneumatic-electric combined heating continuous forging heating furnace
A gas-electricity combined heating continuous forging heating furnace relates to the field of metal forging processing and comprises a heating furnace, a partition plate cover is fixedly mounted on the rear side wall of an inner cavity of the heating furnace, a mesh plate is mounted between the left side wall and the right side wall of the inner cavity of the partition plate cover, and a natural gas nozzle opening is fixedly mounted on the left side end face of the heating furnace. A gas heating pipe is fixedly installed at an output port of the natural gas burner port, the gas heating pipe penetrates through the side face of the partition plate cover to abut against the upper end face of the mesh plate, a top plate is fixedly installed on the upper end face of the heating furnace, and fixing plates are installed on the top plate at equal intervals. According to the utility model, heat generated by gas heating is taken as a main part, heat generated by electric heating is taken as an auxiliary part, and gas and electric heating are combined bidirectionally, so that the heating uniformity and the temperature control precision are ensured, meanwhile, the heat can be circularly heated again, the utilization rate of the heat is greatly improved, and the heating energy is effectively saved.

Owner:ZHEJIANG XINFENG FURNACE TECH CO LTD
Precision forging device and working method thereof
The invention discloses a precision forging device and a working method thereof, and relates to the technical field of precision forging devices.The precision forging device comprises a mounting rail, a feeding mechanism, a clamping assembly, a forging assembly, a cleaning assembly and a lifting sensing assembly. The feeding mechanism drives the blank to move and rotate in the forging furnace; the lifting sensing assembly detects the position of the blank, the forging mechanism is controlled to only forge the middle high-temperature area of the blank, and cracks in the end low-temperature area are avoided; the cleaning assembly automatically removes surface waste residues in the forging process. The alarm system monitors the forging quality in real time. Automatic and precise forging of blanks is achieved, the forging quality and the material utilization rate are remarkably improved, and the precise forging device has the advantages of being reasonable in structure, convenient and fast to operate, easy to maintain, wide in adaptability and the like and is suitable for precise forging production of high-precision metal parts.


Owner:TIANGONG AIHE SPECIAL STEEL
Multi-station quick die changing mechanism for forging furnace
ActiveCN224294613Uquick switchRapid positioningForging/hammering/pressing machinesForge furnacesMechanical engineering
The utility model relates to the technical field of forging furnace discloses a kind of multi-station quick die changing mechanism of forging furnace, comprising: base, for supporting overall structure;Multiple groups of push cylinder, fixed on base, and its output end is connected with push rod;Guide limiting rod, parallel setting in push rod both sides, for orientation;Push seat, with push rod, guide limiting rod fixed connection, and push seat is equipped with guide bar mouth and positioning jack;Die holder guide bar, slidably installed in guide bar mouth, and positioning slot is equipped in die holder guide bar;Positioning jack, cooperate with positioning jack and positioning slot by positioning jack, realize the quick positioning and locking of die holder guide bar. Multiple groups of push cylinder and guide limiting rod cooperation of being set, so that die holder guide bar can be quickly, stably switched between different stations, greatly shorten die changing time. Meanwhile, the cooperation design of positioning jack and positioning slot realizes the quick positioning and locking of die holder guide bar, improves the accuracy and efficiency of die changing.

Owner:HENAN HENGDISHENG NEW MATERIALS CO LTD
Sorting device and sorting method for rapid discharging of intermediate frequency furnace
The invention discloses an intermediate frequency furnace rapid discharging sorting device which comprises a rack, a blank detection mechanism, a conveying chain, a material kicking assembly, a sorting assembly, a driving motor, an oxide skin assembly, a pneumatic FRL and an electric control box, and the blank detection mechanism is used for detecting whether blanks are qualified or not; the kicking assembly and the sorting assembly are arranged on the front side and the rear side of the middle of the conveying chain respectively. The material kicking assembly is used for kicking the unqualified blanks into the sorting assembly, and the sorting assembly is used for classifying the unqualified blanks falling into the sorting assembly. According to the sorting device for rapid discharging of the intermediate frequency furnace, unqualified hot blanks can be rapidly extracted, removed and classified, the production efficiency of the whole production line is improved, the harmful factor that qualified high-temperature blanks generate oxide skin due to long-time exposure in air is reduced, the energy loss of the hot blanks and the oxide skin are reduced, and the service life of the hot blanks is prolonged. Therefore, the service life of the forging equipment grinding tool is prolonged. The invention further discloses a sorting method for rapid discharging of the intermediate frequency furnace.

Owner:INDUCTOTHERM GROUP CHINA
Large titanium alloy double-hole frame forge piece forming process method
The invention provides a large titanium alloy double-hole frame forge piece forming process method which comprises the steps that a heated round bar is placed in a combined type pre-forming die to be pressed to a designated position, and a blank with a certain shape is obtained; the combined type pre-forming die comprises an upper die, a lower die and a die core with a certain shape. The obtained blank is taken out, remelted and heated and then put into a pre-forging die to be pre-formed, and a pre-forged piece is obtained through pre-forging deformation; the pre-forging die consists of an upper die and a lower die; and finally, the pre-forged blank is put into a final forging die to be subjected to final forging forming after being remelted and heated, and a final forging piece is obtained. By the adoption of the method, the complex free forging blank manufacturing process is avoided, the round bar is directly put into the blank manufacturing die to be deformed, the production quality and efficiency of forgings are guaranteed, forming on a fifty thousand-ton press can be achieved, the forming load is greatly reduced, the production efficiency is improved, and the production cost is reduced.

Owner:CHONGQING UNIV
Heat treatment device for gear forging
The utility model relates to the technical field of gear forging heating, in particular to a heat treatment device for gear forging. According to the technical scheme, the heat treatment device for gear forging comprises a forging furnace assembly and further comprises a feeding assembly, a track and an air supply assembly; an air supply assembly is arranged around the upper end of the forging furnace assembly; a feeding assembly is arranged on the lower end face of the forging furnace assembly. A track is arranged at the lower end of the feeding assembly; the forging furnace assembly comprises a heating furnace, a gas-fired boiler and a heating spray hole; the air supply assembly comprises a U-shaped air supply pipeline and an air blower. External air is blown into the gas-fired boiler through the air blower along the U-shaped air supply pipeline, so that gas in the gas-fired boiler is fully combusted, the combusted gas is blown into the heating furnace through the heating spray holes, a gear arranged on the gear sleeve rod in a sleeving mode is fully heated, heated waste gas is exhausted out of the smoke exhaust hole along the smoke exhaust pipe, and the heating efficiency is improved. The heat energy utilization rate in the heating furnace is effectively improved.

Owner:ZHEJIANG CHUANGWEI MASCH CO LTD
An automatic feeding and forming integrated device of a metal forming machine tool
The application discloses a kind of automatic feeding forming integration device of metal forming machine tool, it is related to metal forming machine tool related technical field, including forging quenching furnace, be set to the storage tank of the feed end of forging quenching furnace and be set to the forging forming machine of discharge end;The bottom discharge port of storage tank is equipped with the adjusting module for adjusting discharge width, and the blanking module for controlling material single branch falling;Adjusting module includes adjusting frame one and adjusting frame two vertically slidingly installed at both sides of discharge port, control module is equipped between adjusting frame one and adjusting frame two, control module is used to drive both synchronous or back to move to adapt to different diameter material.This automatic feeding forming integration device of metal forming machine tool realizes multi-specification adaptation and single-branch accurate blanking by adjusting module and blanking module, cooperates with storage tank preheating to reduce energy consumption, full-process automatic closed-loop operation replaces manual work, improves production efficiency, product quality and operational safety.

Owner:SUZHOU XINBAWU TECHNOLOGY CO LTD
A high temperature rotary heating furnace
This invention discloses a high-temperature rotary heating furnace, comprising a frame and a furnace body. The furnace body includes a furnace shell, a furnace chamber, and inlet / outlet doors. The furnace shell is mounted on the frame, the furnace chamber is located inside the furnace shell, and the inlet / outlet doors are located at one end of the furnace shell and connected to an opening / closing mechanism. A heating assembly is mounted on the top of the furnace shell. The frame also includes a turntable assembly and a rotary drive mechanism for rotating the turntable assembly. The turntable assembly passes through the furnace shell and is located inside the furnace chamber. A sealing mechanism is provided between the turntable assembly and the furnace chamber. This invention has the advantage of improving the heating uniformity and reaction effect of various parts of the workpiece.

Owner:HUNAN SEMICORE THERMAL INTELLIGENT EQUIP CO LTD
Precision forging mechanism and precision forging method thereof
The invention discloses a precision forging mechanism and a precision forging method thereof, and relates to the technical field of forging mechanisms, and the precision forging mechanism comprises a forging furnace, a forging mechanism, a cleaning assembly, a lifting sensing assembly and a master control system. The forging mechanism adopts a hydraulic telescopic cylinder to drive a hammering head, and dust is effectively isolated through a telescopic protective sleeve, so that a hydraulic system is prevented from being polluted and leaked. The cleaning assembly automatically blows away oxide skin and impurities on the surface of the forge piece through forging reciprocating motion, and the surface quality is improved. The lifting sensing assembly and the master controller cooperate to automatically recognize a blank temperature suitable section, the forging area is accurately controlled, and cracks generated at the low-temperature end during forging are avoided. The system also has real-time quality detection and alarm functions, and supports defect remelting and rerepairing. The mechanism has multiple functions of automatic forging, on-line cleaning, intelligent quality control and high-temperature protection, the consistency of forgings, the material utilization rate and the production efficiency are remarkably improved, and the mechanism is suitable for automatic precision forging production of high-precision forgings.

Owner:JIANGSU TIANGONG TOOLS CO LTD
Bearing forging heating furnace structure
The utility model discloses a bearing forging heating furnace structure which comprises a heating furnace body and a base, the heating furnace body is installed on the surface of the base, the bearing forging heating furnace structure further comprises a supporting mechanism, and the supporting mechanism comprises an L-shaped support, a fixed block, a V-shaped row seat, a C-shaped supporting strip, a guide plate, a supporting plate box, a sliding rod and an electric push rod. L-shaped supports are symmetrically installed on the surface of the base on the two sides of the heating furnace body, fixed blocks are inserted into the top ends of the L-shaped supports, a supporting mechanism is arranged at the position, where the heating furnace body is located, of the base, a V-shaped row base and a C-shaped supporting strip are adopted by the supporting mechanism to form a lifting material supporting structure, and bearing blanks with different diameters can be supported and connected through a V-shaped bracket type structure; the heating furnace body does not need to frequently replace supports of different sizes like a traditional mode, the heating requirements of bearing blanks of different sizes are met, and the universality and use convenience of the heating furnace are improved.

Owner:WAFANGDIAN HONGYU BEARING MFG CO LTD
Continuous forging heating furnace
The invention discloses a continuous forging heating furnace, and relates to the technical field of heating forging, the continuous forging heating furnace comprises a furnace body, a hearth is arranged in the furnace body, a feeding port and a discharging port are formed in the two sides of the hearth in the length direction respectively, and a conveying table is arranged in the hearth in a penetrating mode; a preheating cavity, a heating cavity and a transition cavity which can be opened and closed are sequentially formed in the hearth from a feeding port to a discharging port, a plurality of heating nozzles and combustion-supporting gas nozzles are arranged in the preheating cavity, the heating cavity and the transition cavity, a cavity is formed in the conveying table, and a rotatable rotating disc is arranged at the position, corresponding to the heating cavity, of the top wall of the cavity. Four first jacking blocks which are arranged in a matrix mode and can ascend and descend are slidably arranged on the rotary disc, a plurality of vent holes are formed in the top of the preheating cavity, the top of the heating cavity and the top of the transition cavity, and the workpiece forging and heating device has the advantage of improving the workpiece forging and heating efficiency and the workpiece forging and heating effect.

Owner:CHANGZHOU COLLEGE OF INFORMATION TECHNOLOGY
Induction Billet Heater
PendingJP2026043388AIncreasing energy efficiencyInduction heating apparatusElectric machineGear wheel
To provide an induction heating billet heater that suitably prevents welding during billet transportation. [Solution] The induction heating billet heater includes multiple rail components, multiple support posts, and a motor. The multiple rail components are round rod-shaped with spirally uneven sides, arranged to form a path for carrying and passing billets, and have gear portions formed circumferentially at at least one end, and are independently rotatable. Each of the multiple support posts has a gear formed thereon that meshes with the gear portions of the multiple rail components. The motor rotates the multiple support posts so that adjacent rail components rotate at different speeds. Each of the multiple rail components rotates in a direction opposite to the spiral rotation direction relative to the billet transport direction.

Owner:TOYOTA JIDOSHA KK
Uniformly-heated forging normalizing furnace
The utility model discloses a forging normalizing furnace with uniform heating, which relates to the technical field of forging normalizing furnaces, and comprises a furnace body and a soaking component, the inner wall of the furnace body is provided with a mounting plate, the surface of the mounting plate is provided with a mounting hole, and the soaking component for simultaneously heating multiple surfaces is arranged in the mounting hole. And the soaking assembly comprises a mounting frame, a heating plate, a blower nozzle and a blower box, the heating plate is mounted on the inner side of the mounting frame, and the blower nozzle is formed in the side of the heating plate. According to the forging normalizing furnace with the uniform heating function, the four sets of soaking assemblies are annularly distributed on the inner wall of the furnace body and located on the outer side of a workpiece, meanwhile, the workpiece is conveyed and heated to the four faces to be subjected to normalizing treatment, the periphery of the workpiece is heated at the same time, the heating uniformity is improved, and meanwhile the normalizing efficiency of the workpiece can be improved; and the blower nozzle outputs gas through a fan in the blower box, so that heat generated by the heating plate is more uniformly distributed in the furnace body.

Owner:JIANGSU GLERUI FORGING CO LTD
Intelligent distribution method and device for heating furnace of fully-closed vacuum isothermal forging system
ActiveCN119681191Bwell formedAchieve superplastic moldingForging/hammering/pressing machinesForge furnacesDistribution methodProcess engineering
The application provides a heating furnace intelligent distribution method and device of a fully-closed vacuum isothermal forging system, relates to the field of high-end intelligent device manufacturing, and is applied to an intelligent distribution device of a fully-closed vacuum isothermal forging system. The fully-closed vacuum isothermal forging system further comprises a plurality of heating furnaces in a vacuum environment and an intelligent robot for transferring a blank in the plurality of heating furnaces. The method comprises the following steps: obtaining attribute data of a blank to be distributed and performance data of an idle heating furnace; determining a target heating furnace corresponding to heating of the blank to be distributed based on the attribute data of the blank to be distributed, the performance data of the idle heating furnace and a heating furnace distribution model; and controlling the intelligent robot to transfer the blank to be distributed from an originally loaded heating furnace to the target heating furnace. The method is suitable for a heating furnace distribution process of a vacuum isothermal forging system, is used for improving transfer efficiency during blank heating, and improves the intelligent degree of the fully-closed vacuum isothermal forging system.

Owner:GUIZHOU ANDA AVIATION FORGING
Conduction pre-heating of sheet for hot forming
A method for producing components by hot forming includes receiving a blank having a patched region and a non-patched region; pre-heating the patched region of the blank in a pre-heat station to a pre-heat temperature by thermal conduction without pre-heating at least a portion of the non-patched region to the pre-heat temperature, to provide a pre-heated blank; transferring the pre-heated blank from the pre-heat station to a furnace; heating the entire blank in the furnace to an austenite temperature, wherein the austenite temperature is higher than the pre-heat temperature; transferring the heated blank from the furnace to a press; and shaping the heated blank in the press.

Owner:MAGNA INTERNATIONAL INC
Forging heating furnace for metal workpieces
The utility model relates to the technical field of metal forging, and provides a forging heating furnace for a metal workpiece, which comprises a heating box body, a fixing assembly is arranged in the heating box body and used for placing the heated metal workpiece, and a heating assembly is arranged in the heating box body and used for heating the metal workpiece. Through the arrangement of the fixing assembly, when a metal workpiece is machined, the metal workpiece is firstly placed in a containing bin, then a baffle plate is closed, a mounting block is fixed in a groove in the surface of a sliding rail, a heater is started through a control button for heating, and then a driving motor drives a connecting rod to rotate; and the sliding rail rotates together with the rotating shaft, so that the metal workpieces in the sliding rail can be machined in all directions, and meanwhile, the situation that the metal workpieces are adhered together due to long-time placement is avoided.

Owner:ZHEJIANG RUISHENG MASCH TECH CO LTD
Heating and forging integrated device
ActiveCN223801465UIncreasing energy efficiencyForging/hammering/pressing machinesThermodynamicsInsulation layer
The utility model discloses a heating and forging integrated device which comprises a hollow shell, and a heating layer, a heat preservation layer, a die sleeve and a die core are sequentially arranged in the shell from outside to inside in a sleeved mode. The heating layer is an induction heating coil layer, and a machining groove is formed in the mold core. An ejection piece is arranged at the bottom of the machining groove, and a male die is arranged above the machining groove. According to the utility model, die heating, blank heating and forging can be completed in the same process, efficiency reduction and heat loss caused by frequent blank transfer are avoided, and the die and the blank can be simultaneously and rapidly heated to the required forging temperature within an extremely short time, so that the production efficiency is greatly improved, the cost is reduced, and the production cost is reduced. And the product stability is further improved, and the product quality is improved.

Owner:HUNAN ZHONGCHUANG AEROSPACE NEW MATERIAL CO LTD
Alloy steel shaft forge piece and stepped heating and heat preservation method thereof
The invention relates to an alloy steel shaft forge piece and a stepped heating and heat preservation method thereof, and belongs to the technical field of forging heating. The obtained blank is heated to be 20-50 DEG C higher than the forging temperature through the stepped heating and heat preservation method, and the used time is X1; heat preservation is conducted at the temperature 20-50 DEG C higher than the forging temperature, and the heat preservation time is Y1; the temperature is reduced to the forging temperature, and the used time is X2; and heat preservation is conducted at the forging temperature, the heat preservation time is Y2, forging is conducted after heat preservation, and the alloy steel shaft forge piece is obtained. And the overall plastic deformation capacity is ensured to be consistent in the subsequent forging process, so that the risk of surface cracks generated due to too low local temperature and poor plasticity is greatly reduced, redundant procedures such as cleaning are reduced, and the surface quality of the forge piece is improved.

Owner:TIANJIN HEAVY EQUIP ENG RES +1
How Japanese swords are made
To provide a method of manufacturing a Japanese sword that can forge a sword with minimum reduction of steel.SOLUTION: A method of manufacturing a Japanese sword includes: a first step S1 of heating and beating out steel; a second step S2 of crushing the beaten steel; a third step S3 of selecting steel of good quality from the crushed steel; a fourth step S4 of stacking the selected steel; a fifth step S5 of heating and integrating the stacked steel; and a sixth step S6 of heating and beating out the integrated steel, and then folding it in two layers. In the first step S1, the steel is heated to a temperature of 800°C or lower and rolled to a thickness of 0.3 mm or less, and the sixth step S6 is repeated three times or four times.SELECTED DRAWING: Figure 1


Owner:倉島 一
Automatic feeding device of forging heating furnace
The utility model discloses an automatic feeding device of a forging heating furnace, and relates to the related technical field of cutting pick production and machining. The device comprises a conveying assembly and a cutting assembly, the conveying assembly comprises a chain conveyor, and an electric heating assembly is further arranged on one side of the discharging end of the chain conveyor; a containing piece is fixed to a conveying chain of the chain conveyor, a movable roller is rotationally connected into an inner groove of the containing piece, a supporting frame is further fixed to the side face, away from the electric heating assembly, of the chain conveyor, a hydraulic telescopic rod is fixed to the upper surface of the supporting frame, and a miniature belt conveyor is fixed to the telescopic end of the hydraulic telescopic rod. When cutting pick blanks are conveyed to the electric heating assembly through the conveying assembly and the chain conveyor to be heated, the hydraulic telescopic rod pushes the micro belt conveyor to move downwards, and then the micro belt conveyor is started to drive the cutting pick blanks to rotate, so that the cutting pick blanks are uniformly heated; the problem that in an existing scheme, when one end of a cutting pick blank is heated, uneven heating is likely to happen is solved.

Owner:XINXIANG SANNIU MACHINERY FORGING CO LTD
Heating furnace special for wind power variable pitch bearing forgings
The utility model relates to the technical field of bearing forging, in particular to a special heating furnace for wind power variable pitch bearing forgings, which comprises a furnace body, the front end of the furnace body is rotatably connected with a sealing door through a hinge, the upper end of the furnace body is fixedly connected with a motor, the inside of the furnace body is rotatably connected with a rotating rod, and the output shaft end of the motor is fixedly connected with the rotating rod. A plurality of rotating plates which are distributed up and down are fixedly connected to the circumferential surface of the rotating rod, supporting sleeves are fixedly connected to the ends, away from the rotating rod, of the rotating plates, carrying frames are rotatably connected to the interiors of the supporting sleeves, angle adjusting pieces are installed at the bottom ends of the carrying frames, and the angle adjusting pieces are used for controlling the carrying frames to rotate. According to the utility model, the wind power variable-pitch bearing forge piece can be heated more uniformly, so that the quality of the heated wind power variable-pitch bearing forge piece can be improved, and the qualified rate of the heated wind power variable-pitch bearing forge piece is higher.

Owner:ZHANGJIAGANG JINRI PRECISED FORGINGS CO LTD
Vacuum isothermal forging process and device suitable for high-temperature titanium-based materials
ActiveCN115846560BIncreasing energy efficiencyForging/hammering/pressing machinesOxygen metersTitanium
The application discloses a vacuum isothermal forging process and device suitable for high-temperature titanium-based materials, relates to the technical field of isothermal forging, and comprises a heating furnace, a male die is connected with a pressure head through high-temperature bolts, and a female die is fixedly connected with a die base through high-temperature bolts; a discharging device is arranged on the lower wall of the heating furnace, so that blank feeding and formed forging taking-out are facilitated; a vacuum pump set and an oxygen meter device matched with the heating furnace can realize monitoring of a vacuum environment and oxygen content in the furnace in the isothermal forging process; the device can guarantee that the whole process from blank and die heating to subsequent forging processes is completely closed, can guarantee the precision and performance of a final formed piece, and has the effects of prolonging the service life of the die and the like. The device can realize almost all heat treatment processes involved in conventional heat treatment and can realize true vacuum isothermal forging.

Owner:TAIYUAN UNIVERSITY OF TECHNOLOGY
Automatic scroll plate forging heat treatment turnover material production line
The invention discloses an automatic scroll plate forging heat treatment turnover material production line, relates to the technical field of new energy automobile spare part production, and aims to solve the problems that in the prior art, scroll plate blanks are easily clamped at a feeding end when being transferred to a heating furnace for heat treatment, so that a subsequent conveying line is cut off, and the production efficiency is low. In order to solve the problems that the number and the time of multiple groups of scroll plates entering a heating furnace are not consistent, the heat treatment effects of the scroll plates are not consistent, and the production quality of the scroll plates is influenced, the technical key points are that the device comprises an anti-blocking conveying module, a sorting conveying module and a control module, the anti-blocking conveying module comprises a storage hopper and a sorting conveying module, and the storage hopper is internally provided with a first slope and a second slope; the sorting and conveying module comprises an anti-blocking disc, and the anti-blocking disc is flush with the slope face of the second slope. The most common cutoff bottleneck in the turnover process is solved, a continuous and stable blank flow is provided for all subsequent procedures, and the overall production takt and heat treatment consistency are guaranteed.

Owner:NINGBO SHUNYI PRECISION MFG CO LTD
A forging method for TC4 titanium alloy three-way pipe joint forging
ActiveCN119702943BForging/hammering/pressing machinesEngine componentsAviationManufacturing technology
The present invention belongs to the field of forging hot working, and specifically relates to a forging method for TC4 titanium alloy three-way pipe joint forgings. By designing the rough shape, reasonably allocating the deformation amount, and designing a one-die, multi-cavity forging die, a single-fire, multi-step forging of titanium alloy small-die forging is achieved. By removing the α layer on the forging surface through chemical milling, and providing appropriate key process parameters such as forging heating temperature, deformation amount, insulation coefficient, cooling method, and heat treatment, TC4 three-way pipe joint forgings with uniform structure and excellent performance can be stably produced. This method realizes the application and promotion of technologies such as the design, die design, and manufacturing process of aviation forgings with similar structures, improves process stability, increases production efficiency, and reduces manufacturing costs.

Owner:SHAANXI HONGYUAN AVIATION FORGING
A forge heating furnace with an adjustable hearth
The utility model provides a kind of adjustable furnace cavity of forging heating furnace, it is related to heating furnace technical field, including ultrasonic welding head body, including heating furnace body, the outer wall side of heating furnace body is fixedly installed with lift door assembly, the inner surface wall of heating furnace body is fixedly connected with four guide rods, four guide rods are movably sleeved with upper high-temperature heat insulation plate between outer surface wall, and the top of upper high-temperature heat insulation plate is fixedly connected with upper insulating layer.In the utility model, under the interaction of each component of the device, the volume of the forging heating furnace cavity can be adjusted flexibly, which precisely fits the blank shape specification, significantly enhances the temperature uniformity of the heating process, effectively reduces the invalid diffusion loss of heat, and thus greatly improves the heating efficiency and reduces energy consumption, providing reliable support for ensuring the forging heating quality and subsequent forging process stability.

Owner:JIANGSU YANXIN SCI & TECH INC CORP