
Patents
Literature
941 results about "Butt welding" patented technology
Efficacy Topic
Property
Owner
Technical Advancement
Application Domain
Technology Topic
Technology Field Word
Patent Country/Region
Patent Type
Patent Status
Application Year
Inventor
Butt welding is a commonly used technique in welding that can either be automated or done by hand on steel pieces. Butt welding can also be done with brazing for copper pieces. It is used to attach two pieces of metal together such as pipe, framework in factories, and also flanges. A flange is something that either is internal or external that provided to strengthen a piece of material. In factories butt welding has shown how economical it can be for companies to use when building things out of metal. This is because if they wanted to make something out of metal without welding it together they would have to bend everything and reinforce the structure which costs more than welding the two pieces together. Butt welding is accomplished by heating up two pieces of metal, or applying pressure, or doing both of those. Penetration while welding the metal is important to maintain and with thin pieces of metal this is possible however, with thick pieces edge preparation may have to be done to prepare the metal. Full penetration butt welds are made when they are in the within the parent(bigger, stronger) metal. In butt welding the strongest welds will have the fewest imperfections. To achieve this the heat input is controlled, which decreases the size of the weld. In commercial welding when this is done it also reduces cost but in order to maintain the strength of the weld double butt welds will be used. In butt welding there are two types used to achieve the specific welds and then there are also a variety of joints considered to be butt joints.
Steel structure butt welding device for steel structure machining
The invention discloses a steel structure butt welding device for steel structure machining, and relates to the technical field of steel structure welding. Comprising a welding handheld part, a movable light blocking piece is installed on the welding handheld part, and the movable light blocking piece is used for preventing flash drilling; a shielding safety piece is mounted on the movable light shielding piece; the shielding safety piece is used for controlling welding after preferential shielding; an included angle adapting piece is mounted on the movable light blocking piece; an inserting seam control piece is mounted at the bottom of the welding handheld part; the inserting seam control piece is used for ensuring the installation of the run-on plate; the shielding safety piece is adopted to be matched with the movable light shielding piece, automatic control can be achieved, and before welding work is conducted, a welding gun gooseneck pipe is shielded through the welding light filter, and drilling prevention work is conducted; the steel structure butt welding device solves the problems that an existing steel structure butt welding device for steel structure machining is poor in anti-trepanning safety effect, and welding wire bonding and blocking cannot be conveniently and automatically controlled after welding is completed.

Owner:JINAN JINYILIN REAL ESTATE DEVELOPMENT CO LTD
Steel beam butt welding device
The utility model discloses a steel beam butt welding device which comprises tool frames arranged on the two sides at intervals, and a connecting plate is fixedly connected between the bottoms of the tool frames. A plurality of pushing rollers are rotationally connected to the connecting plate; clamping wheel assemblies for clamping a steel beam are assembled and connected to the tool frame, each clamping wheel assembly comprises a plurality of clamping wheels assembled on the tool frame in a sliding mode, and sliding rods connected to the tool frame in a sliding mode are fixedly connected to the clamping wheels; the clamping wheel assembly further comprises a driving arm fixedly connected to the sliding rod, and the two ends of the driving arm are each provided with a pushing air cylinder. In the welding and pushing process of the steel beam, the clamping wheel assemblies are clamped on the two sides of the steel beam, and the pushing accuracy is kept. According to the device, in the steel material welding process, a steel beam is accurately pushed and aligned to a welded steel frame in a labor-saving and easy-to-adjust mode, and in this way, the welding difficulty is reduced while the welding efficiency is improved.

Owner:QINGDAO MCDERMOTT WUCHUAN OFFSHORE ENG CO LTD
Large-span corrugated steel web composite beam and construction method thereof
The invention provides a large-span corrugated steel web composite beam and a construction method thereof. The composite beam adopts section prefabrication and field assembly, and a composite abutted seam system is creatively adopted between beam sections. Butt welding is adopted for corrugated steel webs between beam sections, glue seams are adopted for concrete, and shear key teeth are matched, so that the self-alignment performance and the interface shear bearing capacity of a matching surface are improved; wave-shaped abutted seam notches are formed in the upper portions of the concrete top plate and the concrete bottom plate, concrete above abutted seams is a continuous pouring body, the waterproof performance is durable and reliable, and the long-term safety and the service life of the structure are effectively guaranteed under the condition that a waterproof leveling layer is not arranged. And in addition, the concrete in the notches is pre-pressed through the tensioning external prestressing procedure after the beam bodies are closed, the concrete at the abutted seams is further compacted, and super-strong durability is provided. A concrete waterproof layer does not need to be independently arranged on the main beam structure, the second-phase dead load borne by the main beam is effectively reduced while the work amount is reduced, and economic benefits are remarkable.

Owner:HUNAN PROVINCIAL COMM PLANNING SURVEY & DESIGN INST CO LTD +1
Laser welding method for unequal-thickness heterogeneous hot forming steel joint through annular light spot and light beam deflection coordinated regulation and control
The invention provides a laser welding method for an unequal-thickness heterogeneous hot-formed steel joint by cooperatively regulating and controlling annular light spots and light beam deflection. The method comprises the following steps: firstly, pretreating, clamping and positioning the PHS1500 and PHS2000 unequal-thickness ultrahigh-strength steel plates; then, the deflection angle of the light beam is adjusted to be within the range of-30 degrees to + 30 degrees; and finally, a galvanometer control system is used for driving a laser beam to conduct swing scanning in a circular track, and welding is completed under the condition that parameters such as laser power, welding speed, swing frequency, the ratio of swing amplitude to core ring energy and the like are set. According to the method, wire filling is not needed, the PHS1500 and PHS2000 butt welding joints can be effectively connected within the light beam deflection angle range of-30 degrees to + 30 degrees, efficient connection can be achieved within the light beam deflection angle range of-20 degrees to + 20 degrees, weld joint forming is effectively improved, weld joint grains are refined, and the problems of stress concentration and welding softening areas caused by different thicknesses and different strengths of plates are solved. And within the light beam deflection angle range of-20 degrees to + 20 degrees, the obtained joint welding seam is well formed, the tensile strength can reach 1400 MPa or above, and the method is suitable for manufacturing the tailor-welded structure of the unequal-thickness plates of the automobile body.

Owner:SHENYANG UNIV
A method for predicting deformation of plate butt welding based on inherent strain method
ActiveCN116372406BWelding/cutting auxillary devicesAuxillary welding devicesButt weldingClassical mechanics
The present invention provides a method for predicting deformation of plate butt welds based on an inherent strain method. The method comprises: providing a group of plates of the same material with different thicknesses, establishing a welding deformation prediction model based on the plates; obtaining the plate thicknesses, and using the deformation prediction model to obtain the shrinkage of plates of different thicknesses, thereby establishing a curve relationship diagram of the shrinkage and plate thickness under unit inherent strain and regional width; and calculating the shrinkage angle of the plate butt welds based on the curve relationship diagram to determine the maximum deformation of the plate shrinkage. By calculating the shrinkage angle of the plate butt welds based on the curve relationship diagram to determine the maximum deformation of the plate shrinkage, the present invention enables technicians to approximately calculate and predict the maximum deformation of the plate shrinkage caused by welding deformation through the prediction method of the present invention, thereby quickly guiding work in the design and production stages.

Owner:HEFEI UNIV OF TECH
A pipe welding apparatus for self-positioning butt welding of a pipe
The application belongs to the technical field of welding, and particularly relates to a pipe welding device for butt welding of self-positioning pipes. The following scheme is proposed and comprises a welding table, a butt joint mechanism, two top fixing mechanisms and a welding mechanism. The butt joint mechanism is fixed on the welding table, the two top fixing mechanisms are arranged on the two sides of the butt joint mechanism, the welding mechanism is fixed on the top of the welding table, and the top of the welding table is provided with a side edge fixing mechanism. The side edge fixing mechanism comprises a transmission assembly, a support frame, a rotary table, a guide rod, a push plate, a support plate, a side edge support seat and a side edge butt joint plate. One end of the support frame is fixed on the side edge of the butt joint mechanism, and the rotary table is rotationally connected in the support frame. The application can effectively improve the butt joint effect of the pipes, so as to facilitate the welding of the two pipes, prevent the misalignment of the two pipes during butt joint due to the poor fixing effect of the pipes, and thus affect the welding of the pipes.

Owner:JILIN PROVINCE HAONING LASER WELDED PIPE TECH DEV CO LTD
Automatic welding equipment for hubbed welding neck flanges for pipe fittings
InactiveCN120839413AWelding/cutting auxillary devicesAuxillary welding devicesButt weldingPipe fitting
The invention relates to the technical field of automatic welding of pipe fittings, and provides automatic welding equipment for hubbed butt welding flanges for pipe fittings, which comprises a workbench, and the workbench is provided with a roller assembly, two clamping assemblies, a flange feeding assembly, a pipe fitting feeding assembly, a receiving box and a welding assembly, the rolling wheel assembly is located between the two clamping assemblies, the flange feeding assembly and the pipe fitting feeding assembly are located on one side of the rolling wheel assembly and the clamping assemblies, and the material collecting box is located on the other side of the rolling wheel assembly and the clamping assemblies. The pipe fitting is moved through the roller assembly, the center of the pipe fitting is aligned with the center of the three-jaw chuck, alignment is not needed during welding, and therefore the adjusting time is saved, and the efficiency is improved; a plurality of pipe fittings and flanges are stored in a fixed-axis mode through the flange feeding assembly and the pipe fitting feeding assembly, convenience is provided for welding, the adjusting time is shortened, and the efficiency is improved.

Owner:YANCHENG HAILONG PIPE FITTINGS MFG CO LTD
Steel structure butt welding adjusting device
The invention discloses a steel structure butt welding adjusting device which comprises a supporting plate and supporting rods fixed to the four corners of the bottom of the supporting plate. A grinding part is arranged in the butt joint mechanism, in the butt joint process of the two steel structure bodies, the grinding part can make contact with the steel structure bodies along with continuous movement of a driving part, the grinding part comprises a coarse grinding plate, a fine grinding plate and a polishing plate, in the grinding process, a sliding plate slides on the top of a supporting plate along with a mounting plate driven by the driving part to move, and the grinding plate is in contact with the grinding part. The rough grinding plate firstly makes contact with the rotating steel structure main body and conducts comprehensive rough grinding on the end face of the steel structure main body through rotation of the steel structure main body, and due to the fact that a second gear at the bottom of a lead screw is meshed with a second rack at the bottom of a mounting shell, the lead screw can rotate, and therefore when a grinding piece moves to a certain degree, the grinding piece can rotate. And the rough grinding plate, the fine grinding plate and the polishing plate can sequentially treat the steel structure body and then move downwards into the second mounting frame.

Owner:YANGZHOU ZHONGTIAN MASCH MFG CO LTD
Full-coverage and full-process automatic production line of steel arch for tunnel supporting and technology thereof
PendingCN121491761AOther manufacturing equipments/toolsMetal working apparatusProduction lineButt welding
The full-coverage and full-process automatic production line comprises a feeding mechanism, a feeding cutting mechanism, a butt welding mechanism, a cold bending mechanism, a hole cutting mechanism, a transferring mechanism and a connecting plate welding mechanism, and the feeding cutting mechanism is used for cutting and chamfering the two ends of steel; the butt-joint welding mechanism is arranged between the feeding cutting mechanism and the cold bending mechanism and is used for performing butt-joint welding on the current steel and the remaining raw materials of the previous section; the cold bending mechanism carries out cold bending treatment on the steel; the hole cutting mechanism is arranged on a discharging path of the cold bending mechanism, and a guide pipe hole for loading a small guide pipe is formed in the steel; the fixed-length cutting mechanism is arranged at the output end of the hole cutting mechanism and is used for carrying out fixed-length cutting treatment; the transferring mechanism is arranged on the downstream portion of the fixed-length cutting mechanism and transfers the steel to a welding preset station, and the connecting plate welding mechanism conducts end connecting plate welding on the steel transferred in place. The automatic production line can meet the requirements of tunnel construction for steel hole sites, structural strength and batch production.

Owner:JIANGSU JINSANLI MACHINERY MFG
Butt welding device for safe machining of welded pipe
The butt welding device comprises a workbench, stand columns are connected to the four corners of the bottom of the workbench, guide rods are connected to the front end and the rear end of the workbench, the outer portions of the guide rods are movably sleeved with two sliding sleeves left and right, a translation base is connected between the front sliding sleeve and the rear sliding sleeve, and a steering shaft is rotationally connected to the center of the translation base; the upper end of the steering shaft is connected with a bearing shell, the middle section of the top of the workbench is connected with a vertical base, a round through hole is formed in the upper portion of the vertical base, an annular base is installed in the round through hole, the left end of the annular base is connected with a welding assembly, and the outer wall of the vertical base is connected with a PLC. The welding pipe butt welding device is reasonable in structural design, accurate positioning of the welding pipe is achieved through photoelectric calibration and mechanical synchronization, the machining process is shortened by integrating multiple functions of clamping, grinding, welding and dust removal, the flexibility and durability of the system are improved by means of modular steering and low-friction design, and the butt welding efficiency, precision and safety of the welding pipe are remarkably improved.

Owner:WUXI HUITAI STAINLESS STEEL IND PIPE CO LTD
Bridge steel vertical position welding method
The invention provides a vertical position welding method for bridge steel. The vertical position welding method comprises the steps that 1, a groove is manufactured, specifically, the X-shaped groove without a truncated edge is manufactured in a vertical position mode through a flame cutting technology; and the groove is polished and derusted according to requirements. 2, preheating, wherein the bridge steel is preheated to 75 DEG C in an electric heating mode; and 3, welding, wherein solid welding wire argon-rich mixed gas shielded welding is adopted for vertical position welding. And 4, post-weld heat treatment is conducted, specifically, after welding is completed, post-heat treatment is conducted at 200-250 DEG C through a crawler-type heater, and slow cooling is conducted to the room temperature after heat preservation is conducted for 3 hours. By researching and developing a welding material and a welding process matched with the Q890qE high-strength bridge steel, the technical problem of quality of a Q890qE vertical position butt welding seam is solved. Welding forming is stable, efficiency is high, deformation is small, the appearance is good, strength and weather resistance are balanced, the service life is long, and economical efficiency and environment friendliness are both considered; the method is especially suitable for engineering scenes with strict requirements on strength, toughness and durability such as long-span bridges and alpine region bridges, and has remarkable economic advantages and social value.

Owner:CHINA RAILWAY BAOJI BRIDGE GROUP CO LTD +1
Butt welding mechanism for molybdenum metal processing
PendingCN120734629AWelding/cutting auxillary devicesAuxillary welding devicesButt weldingMetal machining
The invention discloses a butt welding mechanism for molybdenum metal processing, and relates to the technical field of molybdenum metal processing, the butt welding mechanism for molybdenum metal processing comprises a placing plate of which the bottom is fixedly provided with a mounting frame, placing frames for placing molybdenum rods are symmetrically fixed on the placing plate along the left-right direction, and the two sides of the top of each group of placing frames are of V-shaped structures; side frames making contact with the side ends of the molybdenum rods are arranged on the two sides of the top of the containing plate in a sliding mode, sliding grooves are symmetrically formed in the two sides of the top of the containing plate in the front-back direction, and auxiliary adjusting assemblies used in cooperation with the containing frames and the side frames are arranged on the containing plate. And the machining requirements of molybdenum rods of different specifications can be flexibly met, the positioning stability and precision in the welding process can be ensured, the welding quality and the production efficiency are effectively improved, and the method is suitable for the high-precision molybdenum metal machining scene.

Owner:RUYANG COUNTY TAIYING FURNACE CO LTD
A method for laser wire filler welding of dot rings
ActiveCN117532161Bquality improvementPrevent sidewall melt defectsLaser beam welding apparatusButt weldingThick plate
This invention discloses a spot-and-ring laser filler wire welding method, comprising the following steps: cleaning the surface and bevel of the welding plate, and fixing the welding plate on a welding fixture; using a circular spot and an annular spot as a composite heat source for narrow-gap multi-layer filler wire welding of the welding plate; adjusting the defocusing amount, setting the diameter of the circular spot, and setting the diameter of the annular spot; setting the power of the circular spot and the power of the annular spot; setting the welding speed and the wire feeding speed; starting the welding system to perform welding, selecting the number of welding passes until the welding plate completes the butt welding. This invention uses a circular spot and an annular spot as a composite heat source for narrow-gap multi-layer filler wire welding. The circular spot is used to melt the filler wire to perform laser filler wire welding, and the annular spot is used to heat the sidewalls, preventing sidewall melting defects. This can avoid sidewall incomplete fusion defects during narrow-gap welding of thick plates.

Owner:SHANGHAI JIAOTONG UNIV
High-precision butt welding machine for stainless steel pipes
The invention belongs to the technical field of stainless steel pipe butt welding, and particularly relates to a stainless steel pipe high-precision butt welding machine which comprises a supporting plate, the upper side of the supporting plate is rotationally connected with a positive and negative tooth screw rod, the outer side of the positive and negative tooth screw rod is in threaded connection with a clamping plate, and the outer side of the supporting plate is fixedly connected with a fixing ring. The outer side of the fixing ring is fixedly connected with a first motor, and the output end of the first motor is fixedly connected with a gear. In other words, after the butt joint position of the pipeline is placed and aligned with the laser welding assembly, the butt joint position of the pipeline is clamped and fixed through the clamping plate, the pipeline does not need to rotate through rotation of the laser welding assembly, then the welding position of the pipeline is not prone to deviation, and the welding position of the pipeline is not prone to deviation by reserving enough length for an outer side wire of the laser welding assembly. And the connecting wire can synchronously rotate along with the laser welding assembly, so that the rotation of the laser welding assembly is not limited, the welding of the device is more stable, and the stability of the device is improved.

Owner:XINGHUA ZHENTAI ALLOY STEEL
A profile butt-welding device for construction engineering
ActiveCN120395331BWelding/cutting auxillary devicesAuxillary welding devicesButt weldingMechanical engineering
This invention belongs to the field of profile butt welding technology, specifically a profile butt welding device for construction engineering. It includes a worktable and multiple U-shaped grooves on the upper surface of the worktable. Each U-shaped groove has a rotating roller inside for supporting and conveying tubular profiles. A welding device is installed on the upper surface of the worktable. Two sets of grooves are formed on the upper surface of the worktable, with two grooves in each set, arranged in a triangular pattern. Two sets of positioning and docking components are slidably connected to the upper surface of the worktable. This invention solves the problem that existing butt welding devices typically clamp two tubular profiles, but it is difficult to simultaneously push the two profiles closer together for docking during clamping. This results in a situation where, after clamping and positioning the tubular profiles, if the gap between the two profiles is large, the clamps need to be loosened and readjusted, which is not only cumbersome but also affects the efficiency of tubular profile butt welding.

Owner:BEIJING E-SUNNY ENVIRONMENTAL PROTECTION ENG CO LTD
A hand butt welder
The application belongs to the technical field of welding equipment, and discloses a manual butt welding machine. The manual butt welding machine comprises a rack, a left electrode clamping device, a right electrode clamping device and a position adjusting mechanism; the left electrode clamping device, the right electrode clamping device and the position adjusting mechanism are arranged on the rack; the position adjusting mechanism comprises a sliding shaft and a hand crank assembly; the sliding shaft is arranged on the rack and slides along the left-right direction; the sliding shaft is connected with the right electrode clamping device; the hand crank assembly is arranged on the rack and rotates; the hand crank assembly is sleeved on the sliding shaft and is threadedly connected with the sliding shaft; the hand crank assembly can drive the sliding shaft to move leftward and rightward by rotating relative to the rack. The sliding shaft and the hand crank assembly form a screw nut pair, which is compact in structure, occupies a small space and is beneficial to reducing the size of the manual butt welding machine, so that the manual butt welding machine is more flexible in movement and use; on the other hand, the right electrode clamping device can be driven to move by rotating the hand crank assembly, which is convenient and labor-saving and is beneficial to reducing the labor intensity of the operator.

Owner:TJK MACHINERY (TIANJIN) CO LTD
Welding device for radiator of engineering machinery
The invention relates to the technical field of radiator welding, and particularly discloses a welding device for an engineering machinery radiator. Comprising a circular concave shell, the outer side of the circular concave shell is sleeved with and rotationally connected with a first annular electric sliding rail, the outer side of the first annular electric sliding rail is fixedly connected with an auxiliary driving assembly, the top of the first annular electric sliding rail is fixedly connected with a correction angle block, the inner side of the circular concave shell is fixedly connected with an arc-shaped grinding block, and an arc-shaped through hole is formed in the inner side of the circular concave shell; according to the welding device for the engineering machinery radiator, the two round concave shells are used for conducting inner clamping type fixing on the end portions of the main pipe from the two ends of the main pipe, and the situation that when branch pipe butt welding operation is conducted on the main pipe, the main pipe shakes and deflects due to the influence of external force, and the welding effect is affected is prevented; the arc-shaped grinding blocks are arranged on the inner wall of the circular concave shell to grind and flatten the end face of the pre-fixed main pipe, and the situation that the butt welding effect of the branch pipes is affected due to the fact that the end face of the main pipe is uneven when the main pipe is fixed and is integrally in an inclined state is avoided.

Owner:江苏弘川智能电气科技有限公司
Vacuum consumable electric arc furnace smelting method for titanium and titanium alloy
The invention discloses a titanium and titanium alloy vacuum consumable electric arc furnace smelting method in the technical field of metallurgy. The titanium and titanium alloy vacuum consumable electric arc furnace smelting method comprises the following steps that an electrode block with the preset size and density is machined; an electrode bar formed by splicing the electrode blocks is put into a vacuum arc welding box to be vacuumized; argon is filled, argon filling is stopped when the preset pressure is reached, and standing is maintained for the preset duration; argon is continuously filled, the pressure in the welding box reaches a preset range, electrode bar welding is conducted, and cooling is conducted for a preset duration after electrode bar welding is completed; the welded electrode bar and the prepared auxiliary electrode are placed in a VAR furnace for butt welding, and the self-consuming machine after butt welding is cooled for a preset time length; primary smelting; carrying out secondary smelting; after the electrode blocks are spliced and placed in a vacuum arc welding box, argon with preset pressure is filled, and standing is carried out for preset time, so that it is guaranteed that the argon can penetrate into the electrodes, oxidation in the welding process is reduced, ingot inclusion is reduced, and the surface quality is improved.

Owner:PANZHIHUA IRON & STEEL RES INST OF PANGANG GROUP
Assembly line system for construction of B-type cabin middle assembly sheet bodies
The invention provides an assembly line system for building a B-type cabin middle group sheet body. The assembly line system comprises a feeding unit, a laser cleaning and scribing unit, a friction stir welding plate splicing unit, a ray detection unit, an assembling and welding unit and a discharging unit which are connected in sequence. During construction, the bottom plate plates for splicing the bottom plate are hoisted to an assembly line one by one, the laser cleaning and scribing unit is used for cleaning and polishing a welding bead and scribing various mounting line indication lines, then the friction stir welding plate splicing unit is used for carrying out butt joint on the bottom plate plates one by one according to a plate splicing sequence, and the bottom plate of a middle group sheet body is synthesized; a butt welding seam of a bottom plate is subjected to flaw detection of the ray detection unit and then flows to the assembling and welding unit, T rows and rib plates are subjected to falling assembly according to the positions of an installation line and an indication line through the assembling and welding unit, fillet weld arc welding is carried out after assembly is completed, and finally discharging of a whole middle-group sheet body is carried out through the discharging unit.

Owner:JIANGNAN SHIPYARD (GRP) CO LTD
Method for improving cooperative enhancement effect of laser and electric arc in attraction mode
The invention relates to the technical field of laser material processing, in particular to a method for improving the synergistic enhancement effect of laser and electric arc in an attraction mode. The method comprises the following steps that a workpiece to be welded is installed on a workbench; the back face of the to-be-welded workpiece is subjected to air exhaust treatment, so that a back attraction area is formed on the back face of the to-be-welded workpiece, and the position of the to-be-welded workpiece is adjusted to enable the back attraction area to be located on the lower side of the weld joint; laser and electric arc hybrid welding is carried out on the welding seam, meanwhile, the back attraction area guides electric arc airflow and laser-induced metal steam to directionally escape from the lower side of the butt welding seam, and the concentration ratio of electric arc plasma in the laser action area is improved under the action of attraction force. By the adoption of the method for improving the cooperative enhancement effect of the laser and the electric arc in an attraction mode, the impact effect on electric arc airflow when metal steam generated during laser welding is erupted is reduced, and the cooling effect of the metal steam on electric arc plasmas is reduced. Meanwhile, arc plasmas are attracted to key an orifice area, so that the energy of the arc is more concentrated, and the welding quality and stability are improved.

Owner:BEIJING UNIV OF TECH
Welding device for constructional engineering steel structure
PendingCN121199477AWelding/cutting auxillary devicesAuxillary welding devicesButt weldingDrive wheel
The invention relates to the technical field of building steel structure welding, and particularly discloses a building engineering steel structure welding device which comprises a rack, a first roller and a third roller which are used for assisting in pushing a steel plate are arranged on the top face of the rack, and a welding gun is arranged in the middle of the rack; the second roller is arranged above the first roller in a lifting mode, and sliding sleeves are arranged on the outer sides of the first roller, the second roller and the third roller in a sliding and sleeving mode; and the fixing frame is connected between the first roller and the third roller in a front-back sliding mode, a liftable mounting frame is arranged on the inner side of the fixing frame, a driving wheel used for pushing the steel plate is rotationally mounted on the inner side of the mounting frame, and an anti-skid cushion pad is attached to the outer side of the driving wheel. According to the constructional engineering steel structure welding device, after different steel structures are tailor-welded and fixed, stable conveying of the steel structures and fixing structures of the steel structures can be kept, stable welding can be achieved, and the welding quality is guaranteed.

Owner:ZHEJIANG XURUI GREEN BUILDING CONSTRUCTION GROUP CO LTD
A kind of adjusting device for butt welding of steel structure
This invention discloses an adjustment device for butt welding of steel structures, relating to the field of steel structure welding technology. It includes a load-bearing component, comprising a support base on which a main steel pipe is placed, and a drive rod rotatably connected to the center of the support base; and an adjustment component, disposed on the drive rod, including a displacement frame slidably connected to the drive rod, with a first turntable rotatably connected within the displacement frame. The beneficial effects of this invention are that, through the arrangement of the adjustment component, feeding component, and angle-changing component, after multiple first auxiliary steel pipes are installed, three first auxiliary steel pipes can be driven to move inward simultaneously. When there are discrepancies in manual installation, the drive component can perform adaptive adjustment to ensure that the first auxiliary steel pipe is properly positioned between the two main steel pipes. Simultaneously, the angle-changing component allows for angle-changing adjustment, adapting the installation of second auxiliary steel pipes of different lengths. The overall operation is quick and convenient, requiring no constant manual support.

Owner:JIANGSU ZHONGXU STEEL STRUCTURE MATERIALS CO LTD
Water tank of splitting solar water heater
InactiveCN101294748AEfficient use ofReduce heat transfer medium capacityFluid heatersSolar heat devicesSolar waterConfined water
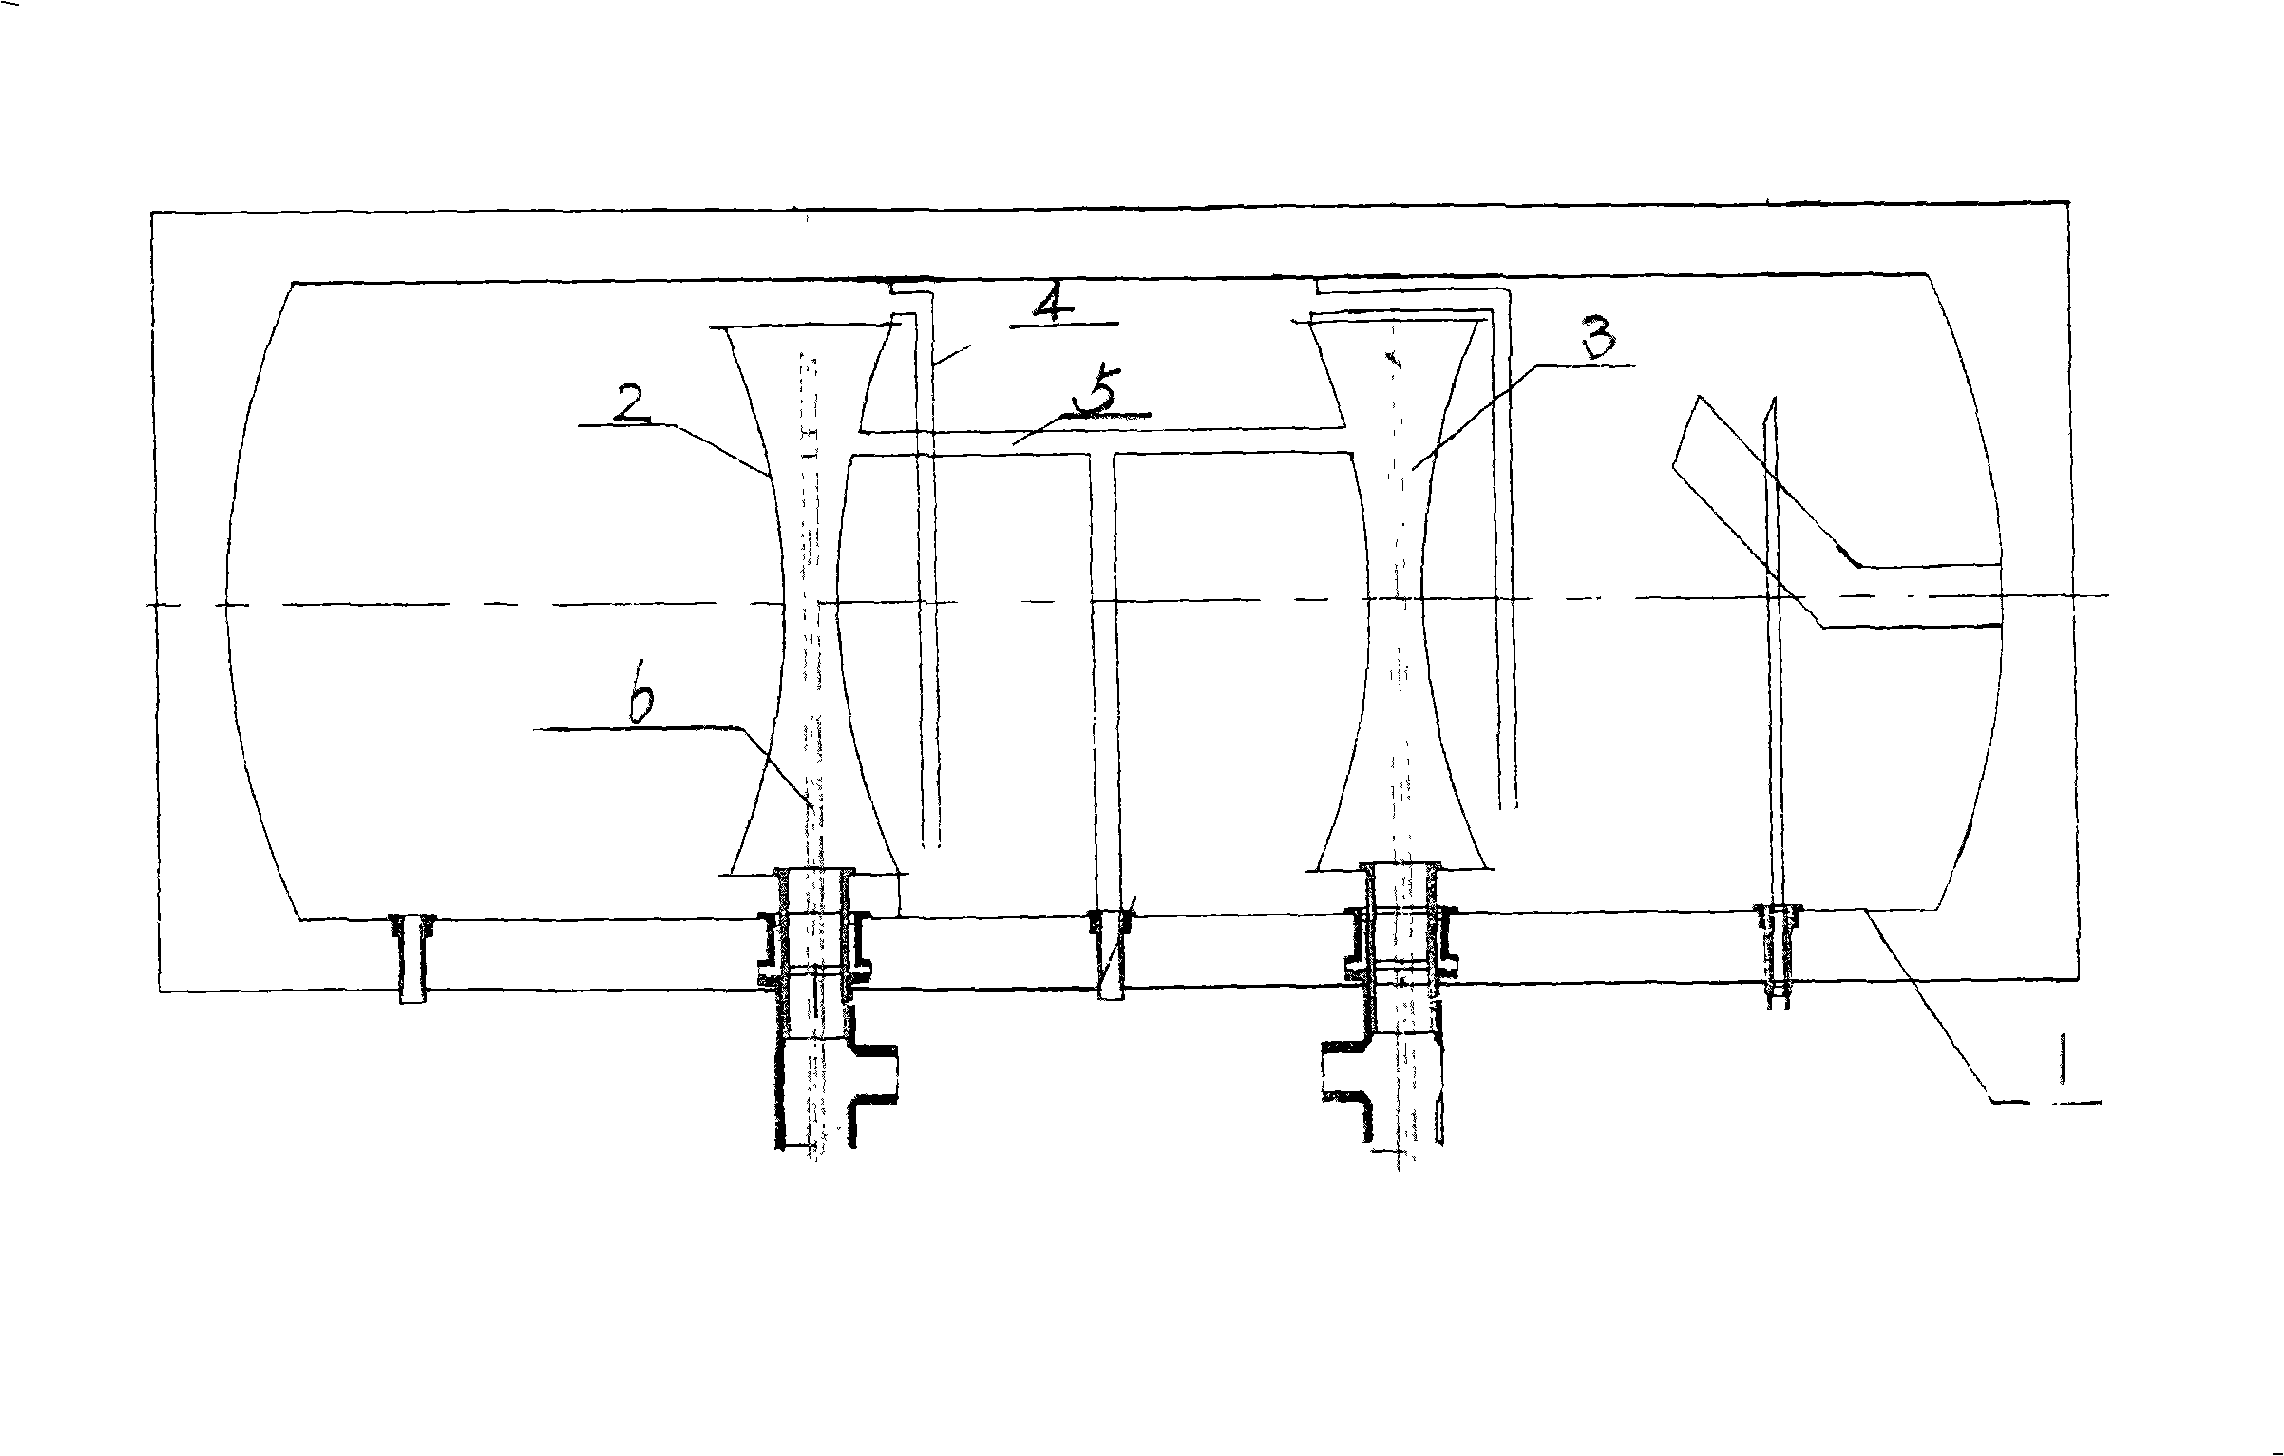
The invention discloses a divided water tank device for an internal heat exchanger of a split type solar water heater. Butt welding is carried out by utilizing an end enclosure of a stainless steel confined water bank inner bag; the end enclosure is used as the heat exchanger to play the role of a water tank partition board; the water tank is divided into independent divided cavities; the heat exchanger is sealed with the inner bag of the water tank; the adjacent cavity bodies communicate with each other via draught tubes; the medium circulation and the medium supplement, namely unconfined running of the heat exchanging part, are carried out safely and reliably via an upper circulating pipe and a heat collecting part; and the device can fully improve heat energy transformation and reduce heat loss.
Owner:江苏元升太阳能集团有限公司
Laser welding equipment for automobile spraying tool production
The invention discloses laser welding equipment for automobile spraying tool production, and belongs to the technical field of laser welding equipment. The laser welding equipment for automobile spraying tool production comprises a welding device and a welding table fixedly installed on the surface of the welding device, two to-be-welded welding plates are placed on the surface of the welding table, a plurality of through-type transverse grooves are correspondingly formed in the surface of the welding table, and two through-type vertical grooves are correspondingly formed in the surface of the welding table; a penetrating type open groove is formed in the middle of the surface of the welding table. Compared with a traditional laser welding device, the laser welding equipment for automobile spraying tool production has the advantages that welding of two flat butt joint welding plates is achieved, welding of two welding plates forming an angle of 90 degrees is also achieved, the welding tool does not need to be replaced in the welding process, and the welding efficiency is improved. And therefore, the welding efficiency of the laser welding device on the automobile spraying tool is improved, and the functionality and practicability of the laser welding device are improved.

Owner:SHANGHAI QIHUAN MACHINERY EQUIPMENT CO LTD
High-strength weldable aluminum alloy cold pressure welding connection and heat treatment method
The invention discloses a high-strength weldable aluminum alloy cold pressure welding connection and heat treatment method. The method comprises the steps of material preparation, cold pressure welding connection, subsequent heat treatment and the like. According to the method, room-temperature cold-pressing butt welding and overall heat treatment are combined and applied to the 7000-series high-strength weldable aluminum alloy, heat input and component deformation in the connection stage are reduced, the welding coefficient of a connection joint can reach 89%-99%, and the method is remarkably superior to fusion welding and other solid-phase welding methods. And a melting solidification structure is not formed in the joint area, so that the structure state and the mechanical performance of the joint area are closer to those of the base material area through a subsequent process, and good overall consistency can be kept under the scenes of long material splicing, component extension and the like. Meanwhile, the process route has certain combination flexibility, and compared with the process only depending on single fusion welding or friction stir welding, the multiple cold pressure welding and heat treatment combination routes are provided to adapt to wires and bars of different specifications and different production rhythms.

Owner:QUZHOU UNIV +1
Stainless steel sheet welding deformation control method
PendingCN121912086AWelding/cutting auxillary devicesAuxillary welding devicesFillet weldButt welding
The invention belongs to the technical field of ship building and repairing, discloses a stainless steel sheet welding deformation control method, and solves the problem that welding deformation of a liquid collecting tray of a sheet stainless steel flat plate structure is difficult to control. Comprising the steps that a flat steel bracket is used in the transportation process, and oily paper is used for packaging; during storage and stacking, putting on a flat ground; during hoisting, an air suction cup or a hoisting plate steel clamp is used for carrying out single-piece hoisting; a hole is formed through laser cutting; before fillet weld welding, permanent toggle plates are assembled between adjacent steel plates, and positioned welding is carried out; before butt joint welding, permanent flat iron is additionally arranged on steel plates on the two sides of a welding seam on the back face of the butt joint welding seam, and staggered positioned welding is conducted on the flat iron and the steel plates; a positioning code plate stretching across the welding seam is additionally arranged on the front face of the butt welding seam; in the welding process, carbon dioxide gas shielded welding is adopted, and a centering and sectioning back welding method is adopted in the welding process of all welding seams. The method is easy and convenient to operate, wide in application range, high in efficiency and low in cost.

Owner:QINGDAO BEIHAI SHIPBUILDING HEAVY IND CO LTD
Diameter-adjustable pipeline welding inner supporting clamp
PendingCN121514811AWelding/cutting auxillary devicesAuxillary welding devicesButt weldingStructural engineering
The invention discloses a diameter-adjustable pipeline welding inner supporting clamp, and relates to the technical field of clamps, the diameter-adjustable pipeline welding inner supporting clamp comprises an expanding and supporting structure, the expanding and supporting structure comprises a guide shaft fixed at the top end of a supporting column and a plurality of expanding and supporting plates distributed in an annular structure, and a fixed sleeve is fixed at the upper end of the guide shaft; the outer wall of the guide shaft is slidably sleeved with a sliding sleeve located under the fixed sleeve, and the height of the sliding sleeve relative to the fixed sleeve is adjustable. One end of the link mechanism is connected with the side wall of the expanding plate, and the other end is simultaneously hinged with the radial outer walls of the fixed sleeve and the sliding sleeve. In order to solve the problems that a pipeline inner supporting clamp is single in applicable caliber, pipe walls are prone to being damaged, and accurate butt joint of pipelines with parts on the circumferential angle cannot be guaranteed, the inner supporting clamp with variable-diameter adjustment, flexible contact and the positioning identification function is provided, circle supporting and circumferential accurate positioning during butt welding of process waste gas pipelines with different diameters are achieved, and the butt welding quality of the process waste gas pipelines with different diameters is improved. And the angle alignment precision of a pipeline with accessories such as a pipe nozzle and a liquid outlet during welding is ensured.

Owner:DIANDUO ELECTROMECHANICAL ENG JIANGSU
Large-diameter pressure pipeline butt welding equipment
PendingCN120862246AWelding/cutting auxillary devicesAuxillary welding devicesButt weldingMechanical engineering
The invention relates to the field of welding equipment, and discloses large-diameter pressure pipeline butt welding equipment which comprises a base, two sets of supporting columns are installed at the top of the base, fixing cylinders are fixedly installed at the tops of the supporting columns, and a welding mechanism is rotationally installed at the tops of the two sets of fixing cylinders; two first telescopic rods are movably hinged to one side of the inner wall of the fixing cylinder. According to the device, three sets of pressing columns and rolling wheels located in a fixing cylinder are horizontally pushed by second telescopic rods and sliding columns to rotate, the outer surfaces of the rolling wheels abut against the outer surfaces of workpieces in a rolling mode, clamping and supporting are conducted at the same time, and after the two sets of workpieces abut against each other, first telescopic rods are used for driving adaptive plates to wrap and abut against the outer surfaces of the workpieces; and the adaptive plate and the workpieces are in large-area contact, butt joint and pressure application, so that only horizontal thrust is generated at the butt joint of the two groups of workpieces, the stress at the butt joint is eliminated, and the welding quality of the device is improved.

Owner:WUHAN HUAHAI TESTING EQUIP CO LTD
Pipe body butt welding equipment
InactiveCN121199546AWelding/cutting auxillary devicesAuxillary welding devicesButt weldingPipe fitting
The invention discloses pipe body butt welding equipment, which belongs to the technical field of welding and comprises a support, a welding assembly and a clamping device. The welding assembly comprises a welding gun and a rail for the welding gun to move, the rail is composed of an upper clamping ring and a lower clamping ring which can move oppositely or oppositely, the upper clamping ring and the lower clamping ring are in butt joint to form a continuous circular rail, and the welding gun can move along the rail. A sliding way is arranged outside the upper clamping ring and the lower clamping ring, a moving body is sleeved outside the upper clamping ring and the lower clamping ring, a welding gun is installed on the moving body, a driving gear is arranged in the moving body, teeth are arranged in the sliding way, a motor drives the gear to enable the moving body to move along the clamping rings, clamping grooves are formed in the inner rings of the clamping rings, and clamping wheels of the moving body roll in the clamping grooves. By means of the design of separation and butt joint of the clamping rings, pipe fitting installation does not need rail penetrating and is suitable for various scenes, the rails are gapless after butt joint, the clamping wheels are matched for guiding, 360-degree welding of pipe fittings is achieved, solder skips and insufficient solder are avoided, and the welding quality is improved.

Owner:JIANGSU JIUXIANG AUTOMOTIVE ELECTRICAL GRP CO LTD
A butt joint device for pipe welding
ActiveCN117984022BReduce alignment errorsWeld firmlyWelding/cutting auxillary devicesAuxillary welding devicesButt weldingButt joint
The application discloses a butt joint device for pipeline welding and belongs to the technical field of pipeline welding, which comprises a holding mechanism and a butt joint mechanism. The holding mechanism comprises two holding arc plates which are hingedly connected, and arc-shaped insertion grooves are formed in the holding arc plates. The butt joint mechanism comprises two butt joint outer plates which are hingedly connected, and a butt joint inner plate which is movably inserted into the butt joint outer plates and is slidably matched with the arc-shaped insertion grooves. Welding ports are formed in the butt joint outer plates in a penetrating manner. In the scheme, the holding mechanism and the butt joint mechanism are connected, so that the pipelines on both sides can be centrally positioned, the operation of assisting in the central positioning of the pipelines by additional workers is avoided, the central positioning error can be greatly reduced, the conditions such as incomplete welding and large butt joint ports in the pipeline welding are prevented, and the welding quality is improved. One person can operate the butt joint device, the labor cost and a large amount of time are saved, the construction efficiency is remarkably improved, the construction period is reduced, and the butt joint device has great popularization and application values.

Owner:CHINA TIESIJU CIVIL ENGINEERING GROUP CO LTD