
Patents
Literature
34results about How to "Meet the processing performance" patented technology
Efficacy Topic
Property
Owner
Technical Advancement
Application Domain
Technology Topic
Technology Field Word
Patent Country/Region
Patent Type
Patent Status
Application Year
Inventor
Magnetic current changing polishing device for large caliber aspheric surface optical part
InactiveCN101249626AWorkpiece clamping is simple and convenientMeet the processing capacityGrinding carriagesOptical surface grinding machinesMagnetic currentMachine tool
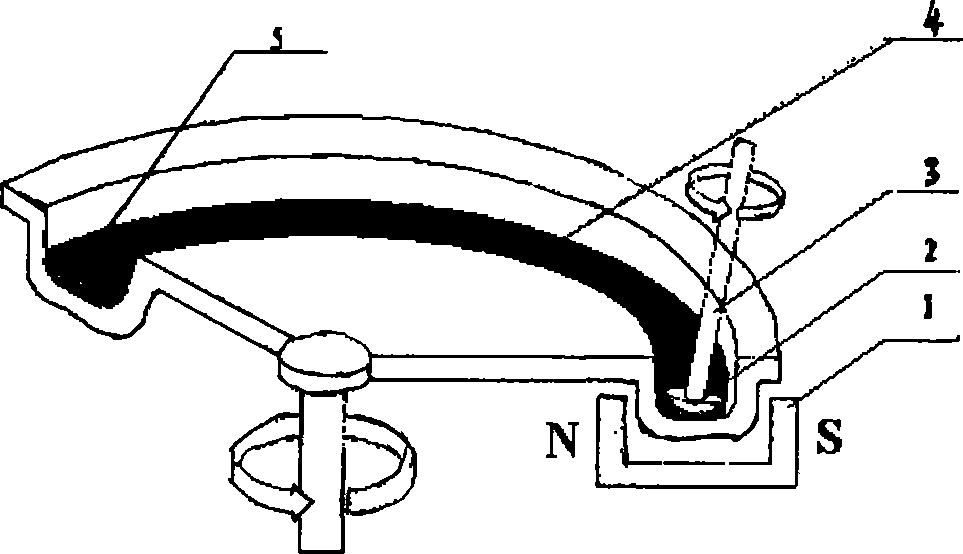
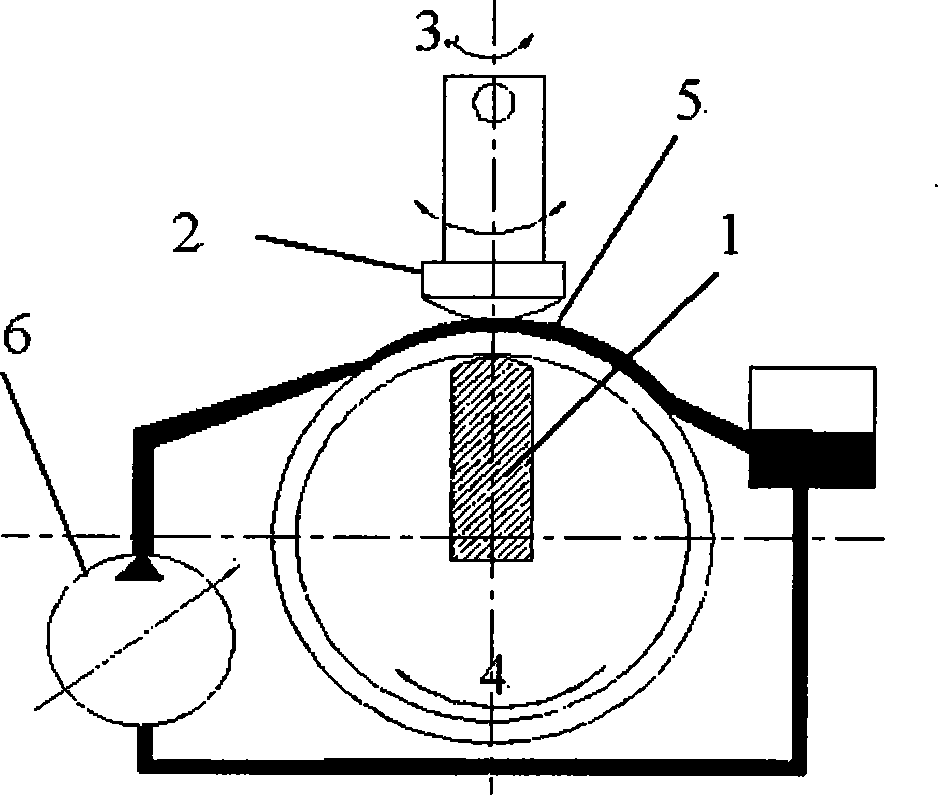
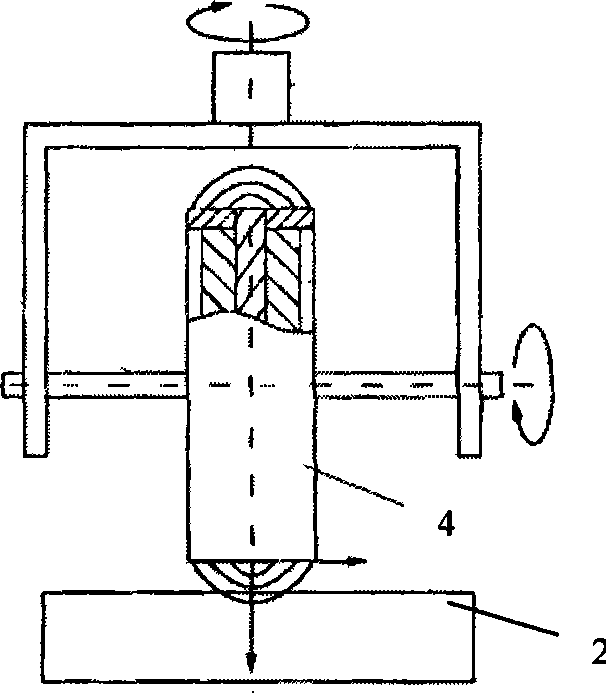
The invention discloses a magnetorheological finishing device for large-caliber aspheric optical parts. The magnetorheological finishing device comprises a machine tool, a finishing device, a magnetorheological finishing liquid circulating system for providing the finishing liquid with stable performance, and a control system connected with the components described above. The machine tool has four or more than four degrees of freedom. The finishing device is fixed on the machine tool and is positioned over the workpiece on the machine tool to be processed. The device has the advantages of simple and compact structure, low cost, simple control, wide range of application, and strong processing capacity, and is used for large-caliber aspheric optical parts.
Owner:NAT UNIV OF DEFENSE TECH
Five-axis linkage numerical control (NC) machining post processor and processing method thereof
InactiveCN102023613ARealize simulationRealize serial communicationProgramme controlComputer controlPost processorManagement functions
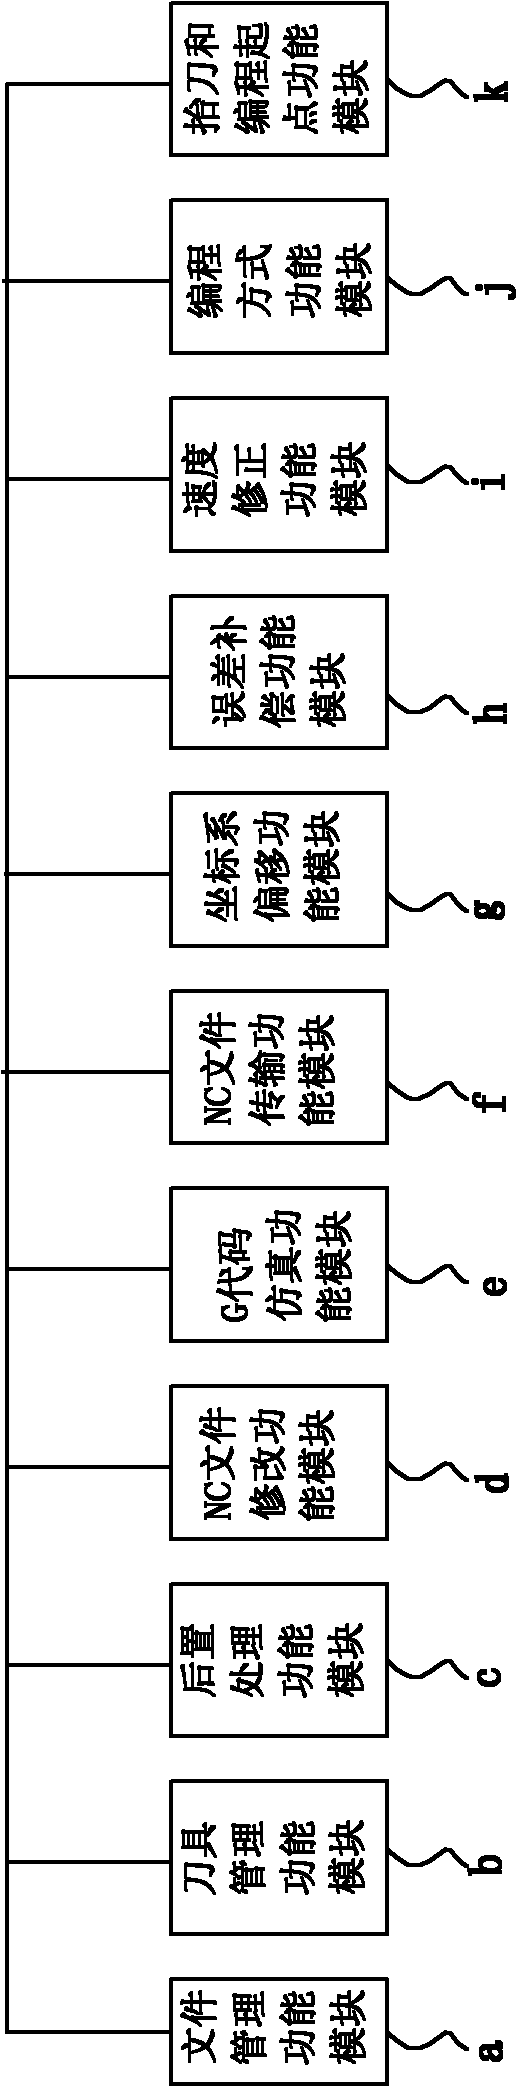
The invention discloses a five-axis linkage numerical control (NC) machining post processor and a processing method thereof, and relates to a post processor for an NC machining program and a processing method. The processor comprises computer program software which is used for processing a cutter location source file generated by a workpiece shape characteristic and a machining process, wherein the computer program software comprises a file management function module, a cutter management function module, a postprocessing function module, an NC file modification function module, a G code simulation function module, an NC file transmission function module, a coordinate system offset function module, an error compensation function module, a speed modification function module, a programming mode function module and a cutter-lifting and programming staring point function module. The processing method comprises the steps of setting a file, arranging a cutter, processing a programming mode, processing data of machine tool motion parameters, processing data of cutter dynamic cutting speed, outputting a G code file and the like. By the processor and the processing method, machining dynamic speed, speed compensation, non-linear error compensation and analog simulation of G code five-axis linkage can be realized.
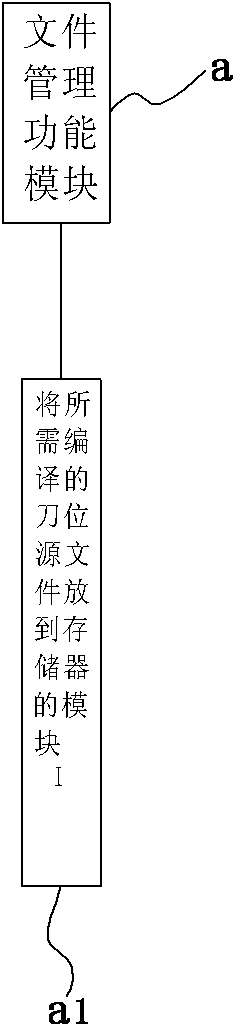
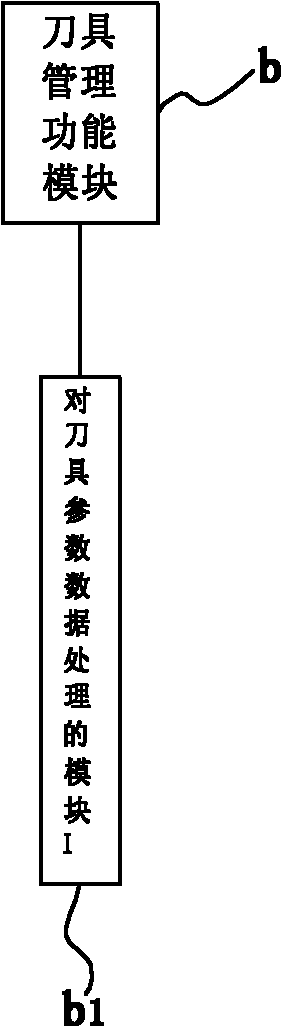
Owner:GUANGXI UNIVERSITY OF TECHNOLOGY +1
Modified chemical fiber using natural protein fiber superfine powder and production process thereof
InactiveCN1594682AMeet the processing performanceGood hygroscopicityConjugated synthetic polymer artificial filamentsProtein fiberMelt spinning
The object of the invention is to provide a modified chemical fiber using natural protein fiber superfine powder and production process thereof. The modified chemical fiber is processed by superfine protein powder and chemical fiber material, in which the protein powder is 5-10%, fiber material is 90-95%. The modified chemical fiber using natural protein fiber superfine powder has an improved wettability, a good anti-static property, a good dyeing performance, and has the effects of wool-like and silk-like. The material is natural protein fiber material with a low price and broad source. The melt spinning and wet spinning will not change the processing craft of the traditional chemical fiber and has a good economic performance.
Owner:WUHAN TEXTILE UNIV
Low-temperature curing color coiled material paint and method for preparing same
ActiveCN101531860ASuitable for continuous roller coatingMeet the hardness and toughnessPolyester coatingsLow temperature curingSolvent
The invention relates to a paint composition, in particular to a low-temperature curing paint used for manufacturing color steel plates and a method for preparing the same. The method comprises the following steps: adding 45 to 60 weight percent of saturated polyester resin, 3 to 5 weight percent of fully-methylated amino resin and 3 to 5 weight percent of partially-methylated amino resin into a reaction kettle; while stirring, adding 3 to 5 weight percent of propylene glycol ether acetate, 2 to 5 weight percent of binary acid dimethyl ester, 2 to 0.5 weight percent of closed cooling catalyst, 0.2 to 0.5 weight percent of open cooling catalyst, 5 to 10 weight percent of trimethyl benzene solvent to the mixture; after stirring the mixture evenly, adding 0.3 to 0.8 weight percent of dispersant to the mixture, and then adding 20 to 40 weight percent of filling pigment and 0.3 to 0.8 weight percent of wax powder while stirring; and after the mixture is dispersed evenly, performing sanding in a sand mill, and then performing paint and color mixing process to obtain the finished product, namely the low-temperature curing color coiled material paint. The method can solve the problems that the prior high-temperature baking curing paint has high curing temperature to cause energy sources waste.
Owner:JIANGSU LANLING POLYMER MATERIAL CO LTD
Production method of glass fiber SMC yarn
The invention discloses a production method of glass fiber SMC yarn, which comprises the following steps: 1) preparation of an impregnating agent; 2) dosing; 3) melting in a kiln; 4) bushing; 5) coating with the impregnating agent; 6) drawing; 7) drying; 8) roving winding; 9) inspection and storage. According to the method disclosed by the invention, by adopting the complete-performance glass component and the special impregnating agent, the need of the drawing operation is met in the drawing technology while the processability of a later unwinding process is also guaranteed, thus the glass fiber SMC yarn has good acid resistance and water resistance, relatively high strength and good electric properties and mechanical properties.
Owner:JIANGSU ZHONGYA NEW MATERIAL
Low temperature curing color coil suede coating
InactiveCN101857767AHigh reactivityProduce a suede effectPolyester coatingsMulticolor effect coatingsLacquerLow temperature curing
The invention relates to a low temperature curing color coil coating, in particular to a low temperature curing color coil suede coating which comprises paint and a curing agent, wherein the paint and the curing agent are stored individually. The formula of the paint comprises the following components by weight proportion: 50% to 70% of saturated polyester resin, 5% to 8% of completely methylated melamine-formaldehyde resin, 1% to 2% of ethylenediamine surface active agent, 0.5% to 0.8% of closed p-toluenesulfonic acid catalyst, 5% to 20% of rutile titanium pigment, 5% to 19% of pigment, 3% to 5% of propylene glycol aether acetate, 2% to 5% of dibasic acid dimethyl ester, 5% to 10% of aromatic hydrocarbon solvent, 0.3% to 0.8% of dispersant and 0.3% to 0.8% of polytetrafluoroethylene wax.
Owner:JIANGSU LANLING COATING TECHN RES INST
Stainless steel tooth zipper and manufacture method thereof
InactiveCN102672077AHigh bonding strengthMeet the processing performanceSlide fastenersWire rodEngineering
The invention relates to a stainless steel tooth zipper and a manufacture method thereof. The stainless steel teeth include pairs of bilaterally-symmetrical tooth bodies, concave surface portions and tooth point portions, wherein the concave surface portions and the tooth point portions are connected in a consubstantiality mode and arranged on the tooth bodies. The concave surface portion is matched with the tooth point portion on the other tooth body in a buckled mode, external clamping convex portions are arranged at the ports on the inner sides of the tooth bodies, and internal clamping convex portions are arranged in the middle of the inner sides of the tooth bodies. The manufacture method of the stainless steel tooth zipper is that a stainless steel wire processed by softening is pull-rolled into a stainless steel wire with a Y-shaped section, then arrangement of teeth is performed by a tooth arrangement machine, and post-processing combination is performed to obtain a stainless steel tooth zipper product. The product has the advantages of being high in corrosion resistance, large in tensile strength, good in quality, high in grade and the like. In addition, the cost of the product is reduced.
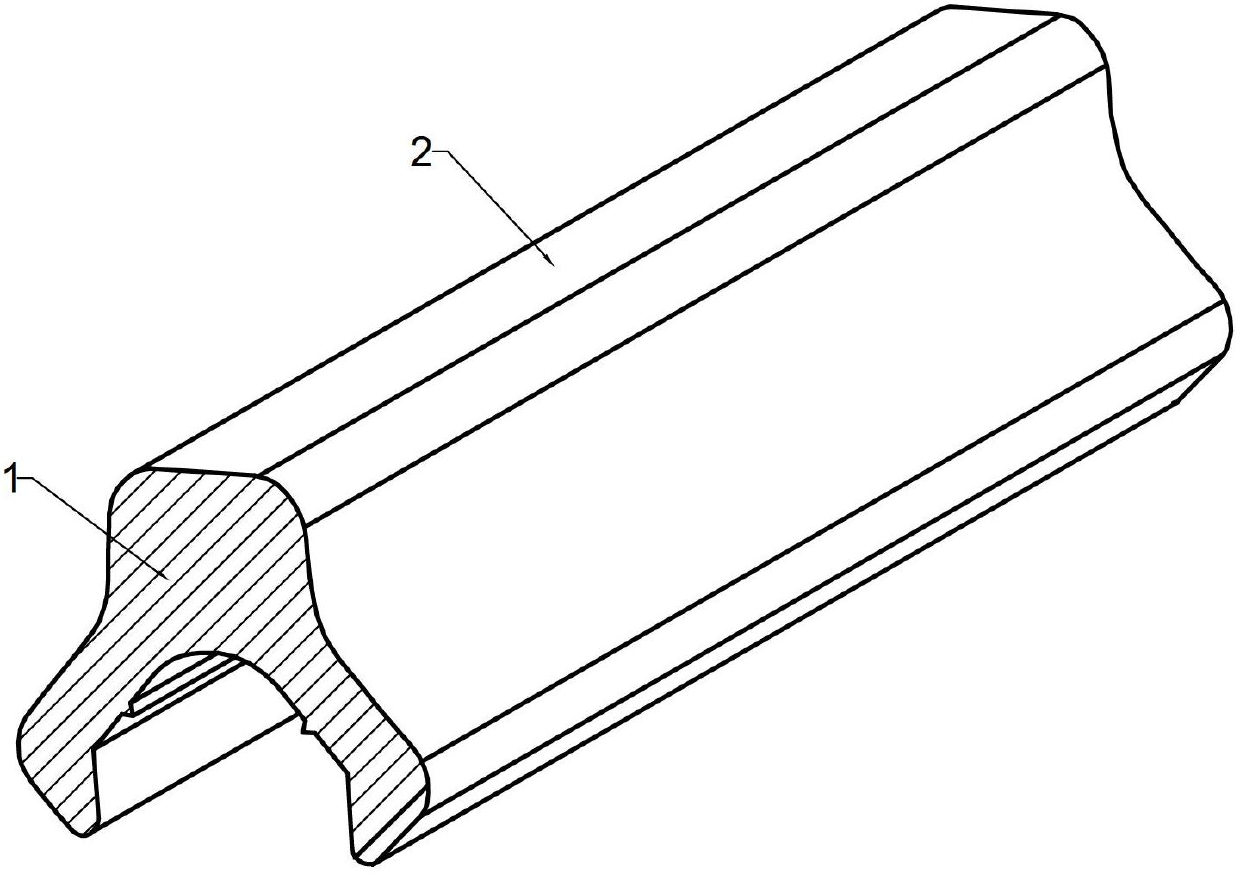
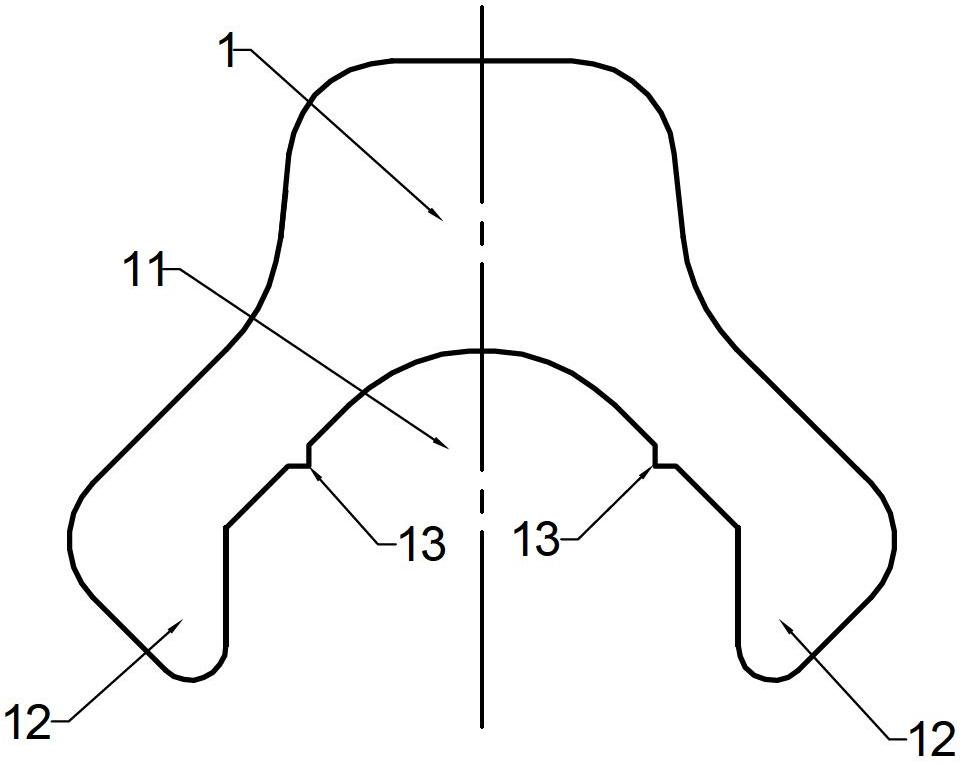
Owner:广东辉丰科技股份有限公司
Thermosetting resin composition, b graded resin film, metal foil, copper-clad board and multi-layer lamination substrate
InactiveCN103665762AMeet bending performanceMeet reliabilitySynthetic resin layered productsMetal layered productsEpoxyInsulation layer
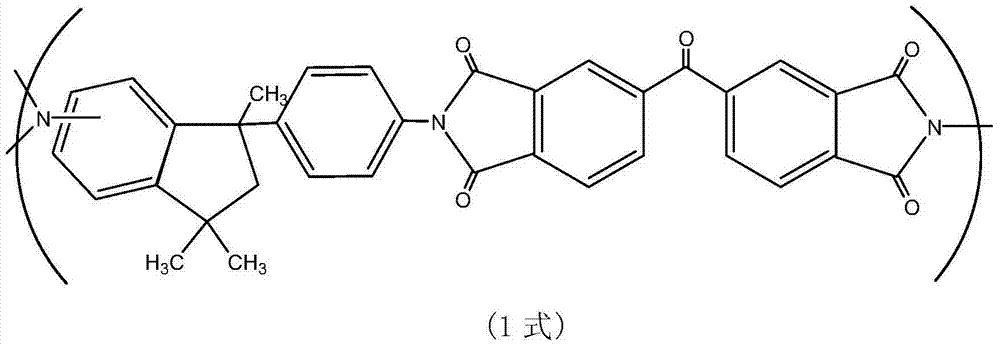
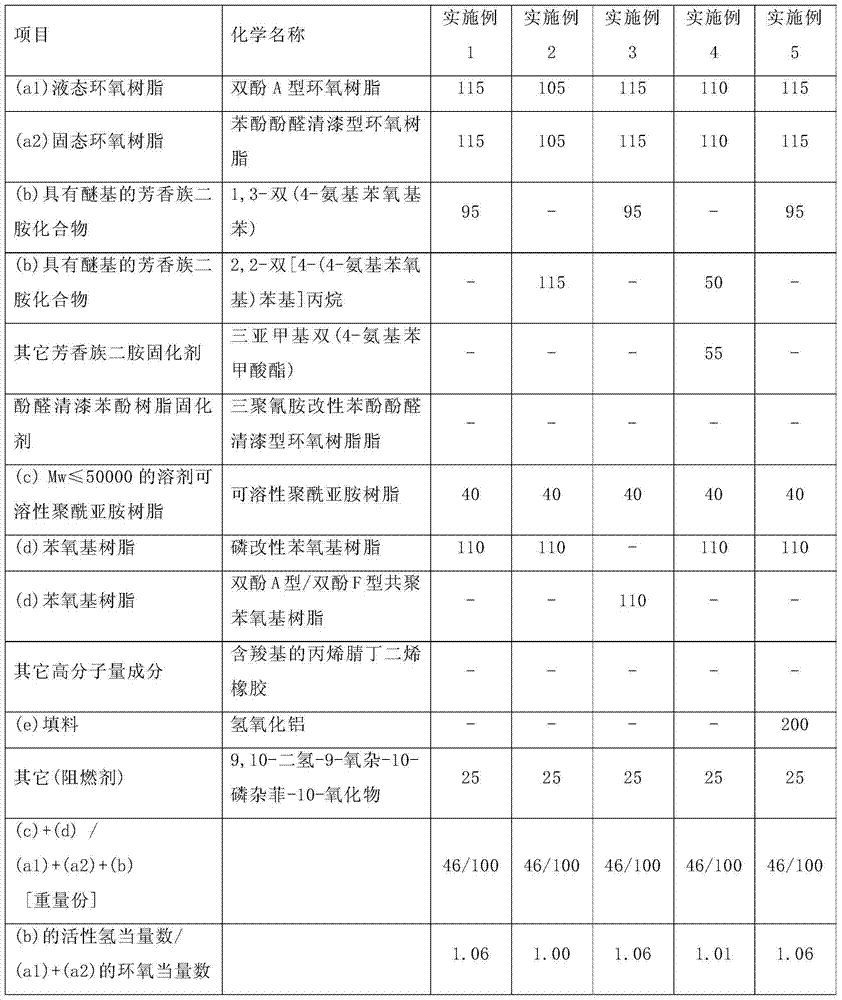
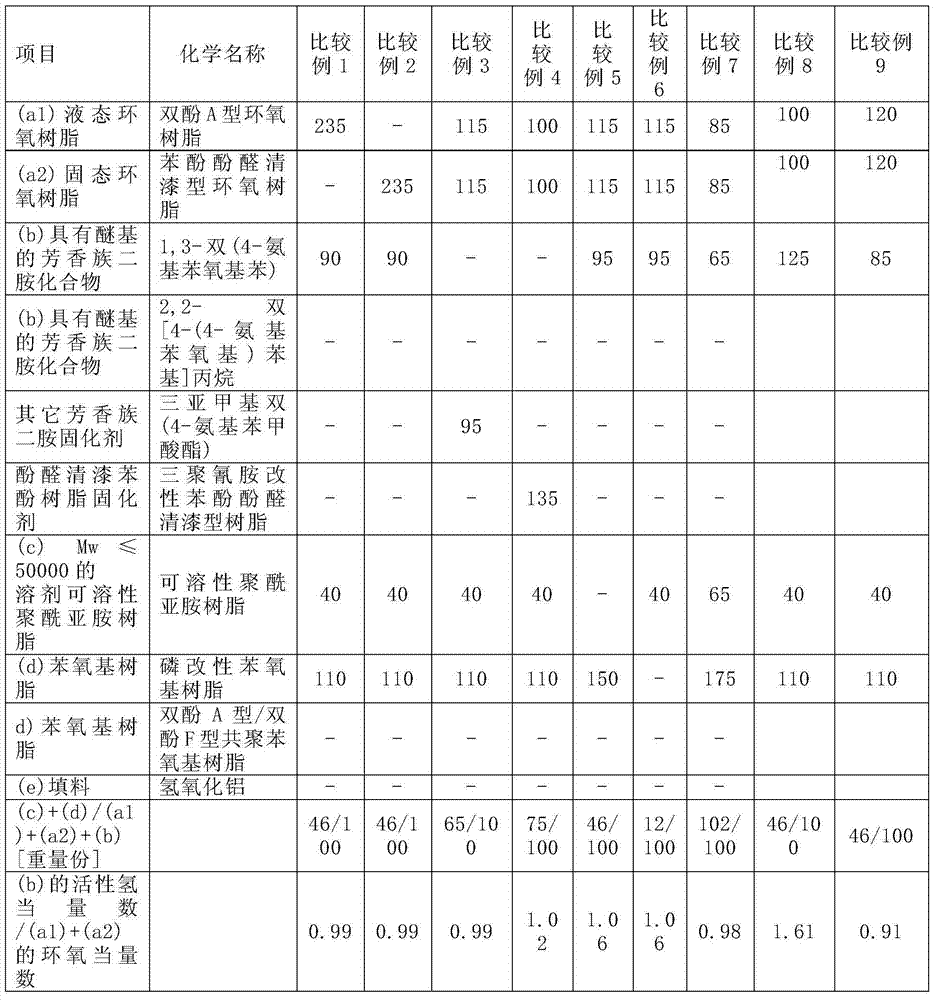
The invention aims to provide an epoxy thermosetting resin composition that can be bent and have a film insulation layer, has reliability and processing characteristic that compare favourably with halogen-free FR-4, and is low in fluidity in a vacuum pressing process. The thermosetting resin composition includes (a1) liquid epoxy resin; (a2) solid epoxy resin; (b) aromatic diamidogen compound with ether group; (c) solvent soluble polyimide resin with weight-average molecular weight below 50000; and (d) phenoxy resin. The amount of (c) solvent soluble polyimide resin with weight-average molecular weight below 50000 and (d) phenoxy resin is more than 15 parts by weight and less than 100 parts by weight when the total amount of the (a1) liquid epoxy resin, (a2) solid epoxy resin, (b) aromatic diamidogen compound is arranged to be 100 parts by weight.
Owner:TAMURA KK
Colorful fingerprint-resisting coating, preparation method and use method thereof
InactiveCN101914332ACorrosion resistanceSatisfy processabilityPretreated surfacesMulticolor effect coatingsSilane compoundsWater based
The invention discloses a colorful fingerprint-resisting coating, which comprises the following components in parts by mass: 50-70 parts of water-based macromolecular latex, 5-10 parts of deionized water, 15-25 parts of pigment, 5-10 parts of resin, 0.1-1 part of wetting agent, 0.5-1 part of flatting agent, 0.1-1 part of antifoaming agent and 1-5 parts of silane compound. Accordingly, the invention discloses a preparation method and a use method of the colorful fingerprint-resisting coating. The colorful fingerprint-resisting coating does not contain metal ions, and has excellent environmental conservation, decay resistance and fingerprint resistance.
Owner:上海丰野表面处理剂有限公司
Low-temperature curing primer-topcoat coil coating back paint and preparation method thereof
InactiveCN105419575AMeet the hardness and toughnessCorrosion resistanceAnti-corrosive paintsEpoxy resin coatingsEpoxyLow temperature curing
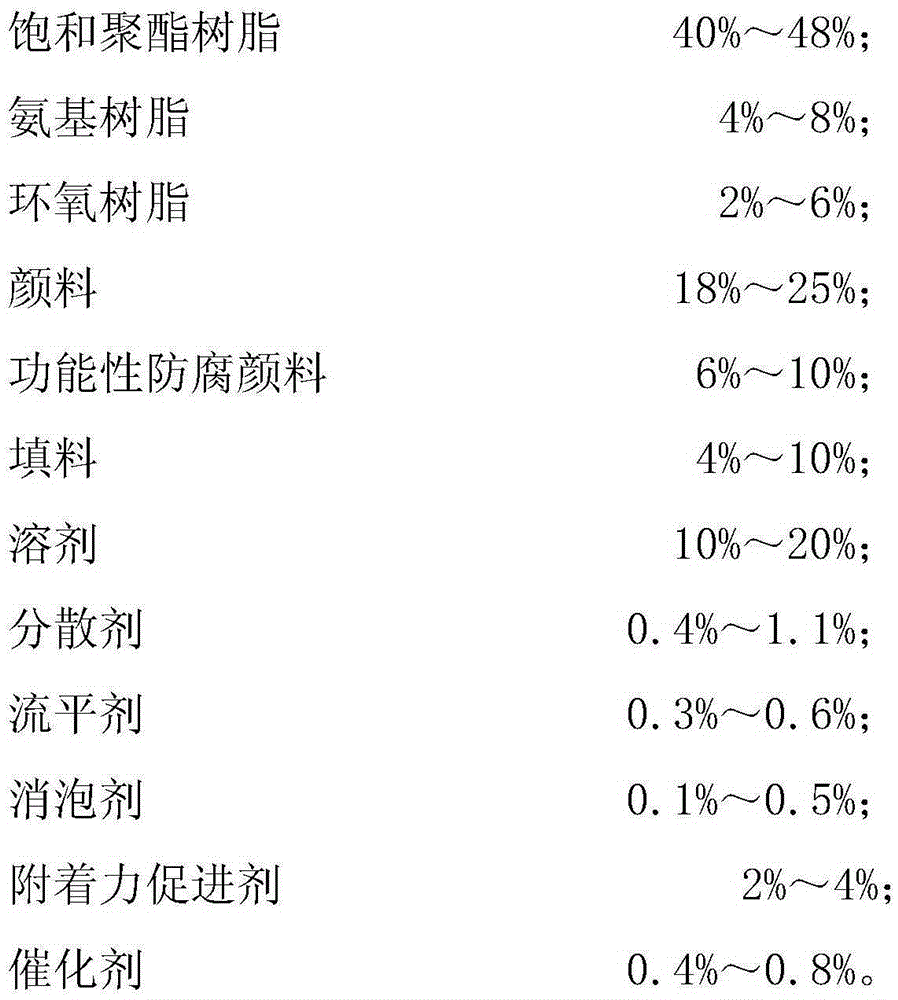
The invention discloses low-temperature curing primer-topcoat coil coating back paint and a preparation method thereof. The low-temperature curing primer-topcoat coil coating back paint is prepared from the following components in mass ratio by stirring and mixing under the rotating-speed stirring condition: 40-48% of saturated polyester resin, 4-8% of amino resin, 2-6% of epoxy resin, 18-25% of pigment, 6-10% of functional anticorrosion pigment, 6-10% of filler, 10-20% of a solvent, 0.4-1.1% of a dispersing agent, 0.3-0.6% of a leveling agent, 0.1-0.5% of a defoaming agent, 2-4% of an adhesion promoter and 0.4-0.8% of a catalyst. The low-temperature curing primer-topcoat coil coating back paint product has low curing temperature and can meet hardness, toughness, corrosion resistance, acid resistance, alkali resistance, heat resistance and processability required by a galvanized steel sheet, and a single coating has excellent adhesive force, machinability and anti-corrosion property. The low-temperature curing primer-topcoat coil coating back paint product is simple in preparation technology, is applicable to being coated on the surfaces of a hot galvanized steel sheet, an electro-galvanized steel sheet and a cold-rolled steel sheet, so as to form a colorful coating protective film, and is also applicable to continuous roller painting of a continuous coating high-speed production line.
Owner:陕西宝塔山油漆股份有限公司
Bake hardening type high-strength steel and manufacturing method thereof
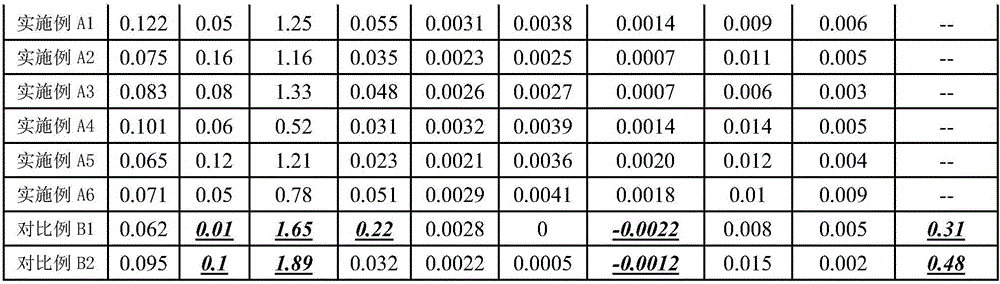
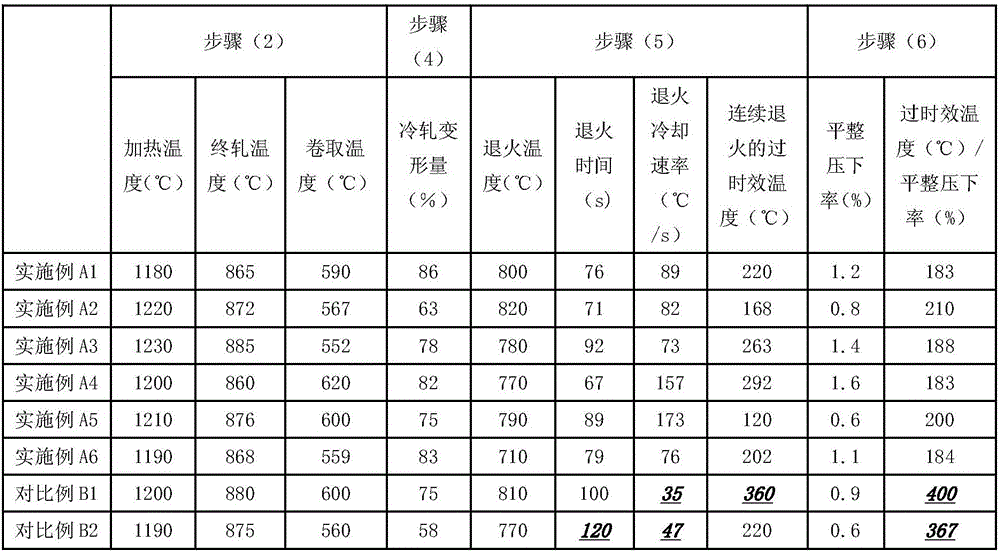
The invention discloses bake hardening type high-strength steel. The bake hardening type high-strength steel comprises, by mass percentage, 0.05 to 0.13% of C, 0.05 to 0.20% of Si, 0.50 to 1.50% of Mn, 0.02 to 0.06% of Al, larger than 0 and not larger than 0.0050% of N, and the balance iron and other inevitable impurities, and in addition, the condition that B-0.77*N is larger than or equal to 0.0005 and smaller than or equal to 0.0020% should be met. According to the bake hardening type high-strength steel, under the condition of not adding precious metals such as Mo, Cr, Ti and Nb, by controlling the mass percentage of carbon, manganese and boron, the technological processes and the technological parameters, the steel which is high in strength, low in cost, high in surface quality and of which the machining performance meets the requirements of automotive parts is manufactured.

Owner:BAOSHAN IRON & STEEL CO LTD
Method for preparing environmentally-friendly flame-retardant bio-based automobile chair polyurethane synthetic leather
InactiveCN109056356AMeet the processing performanceMeet the test requirementsRoad vehiclesTextiles and paperPolyurethane membranePhysical strength
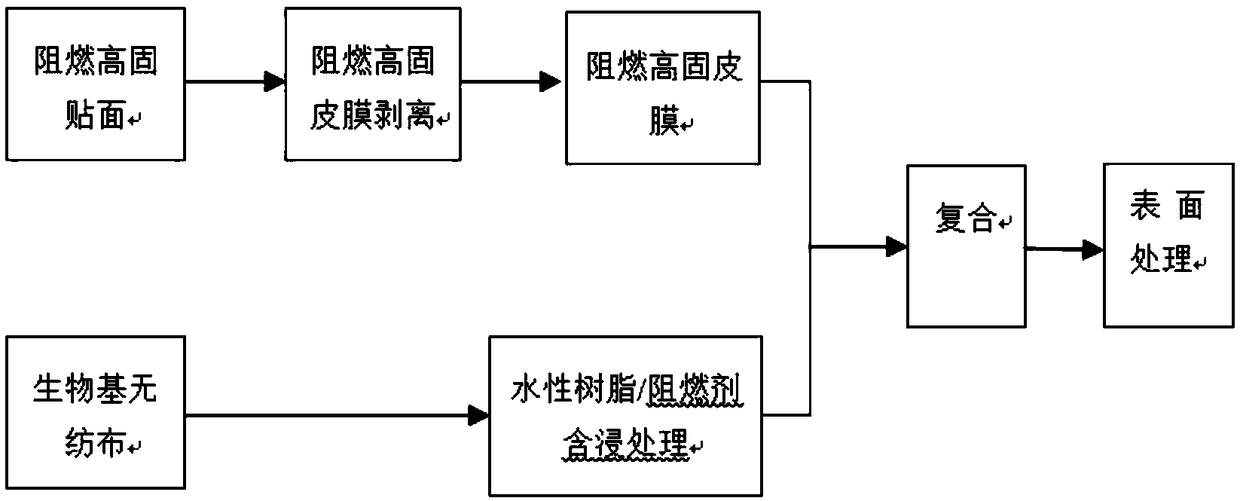
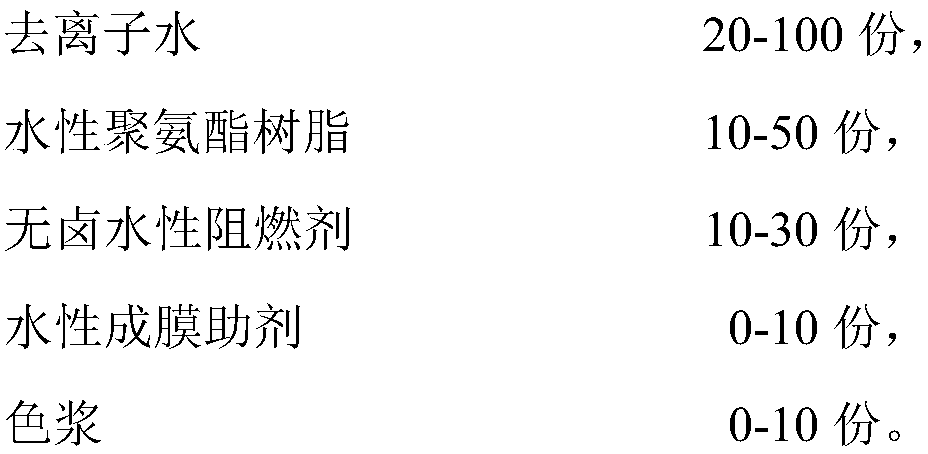
The invention relates to a method for preparing environmentally-friendly flame-retardant bio-based automobile chair polyurethane synthetic leather. The method comprises the following steps: firstly, cospinning a bio-based raw material and chinlon to obtain bio-based base cloth, and carrying out dipping, extrusion and drying to obtain a bio-based basic material with flame retardancy; preparing a halogen-free flame-retardant high-solid polyurethane membrane in a release paper membrane transferring mode, and peeling off the release paper membrane to obtain a high-solid membrane with flame retardancy; finally compounding the bio-based basic material with the high-solid membrane, thereby obtaining a finished product. The environmentally-friendly flame-retardant bio-based automobile chair polyurethane synthetic leather prepared with the method has flame retardancy which meets requirements of grade B provided by 'GB 8410-2006 combustion property of automotive trim material'. Meanwhile, the leather has the advantages of low VOC (volatile organic compound), good environment protection, flexible and full hand feelings, good surface skin friendliness, high physical strength, oil resistance, aging resistance, and the like.
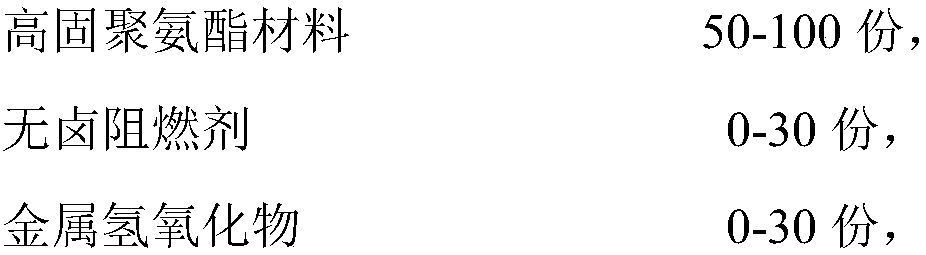
Owner:ANHUI ANLI MATERIAL TECH
Finishing withdrawing-straightening tension control method for deep-draw galvanized steel sheet
ActiveCN103934282AImprove surface qualityGuaranteed surface qualityTension/compression control deviceSheet steelEconomic benefits
The invention belongs to the technical field of galvanized steel sheet production methods, and relates to a finishing withdrawing-straightening tension control method for a deep-draw galvanized steel sheet for guaranteeing the steel sheet performance and the surface quality. According to the technical scheme, the tension set values before and after the finishing withdrawing-straightening are adjusted, and the matching relation between steel plates with different thicknesses and the tension before and after the finishing withdrawing-straightening is adopted, wherein the tension before finishing conforms to the formula: T(strip steel thickness)*(25-30)KN, and the tension after finishing and withdrawing-straightening conforms to the formula: T(strip steel thickness)*(27.5-33)KN. According to the finishing withdrawing-straightening tension control method, the surface quality of the deep-draw galvanized product can be guaranteed, the performance is not greatly affected, the requirement for machining and using performance of a user is met, and the performance aggravating effect brought by increasing the finishing rolling force to guarantee the surface of the deep-draw galvanized product is avoided. The performance judgment amending ratio of the deep-draw galvanized product is greatly reduced, the surface quality and the profit space of the deep-draw galvanized product are greatly improved, the competitiveness of enterprises is enhanced, and considerable economic benefits are brought to the enterprises.
Owner:HEBEI IRON AND STEEL
Heat-sealing coating for aluminum foil meal box and preparation method of heat-sealing coating
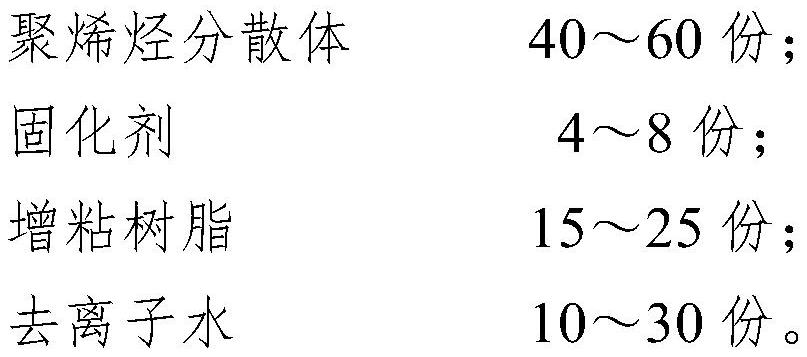
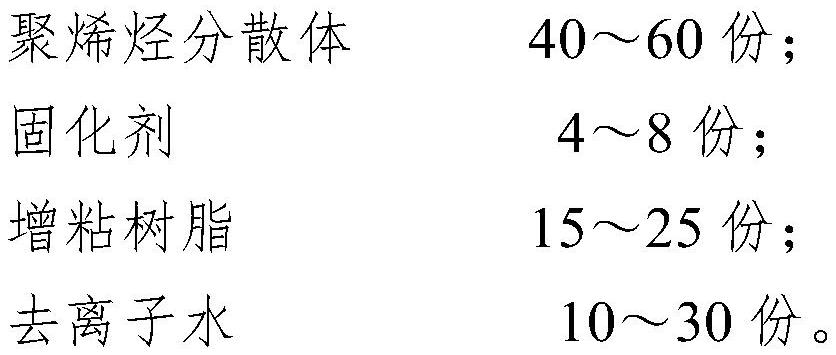
In order to overcome the problems of low heat-sealing strength of the existing aluminum foil meal box heat-sealing material on PP and PE films and poor boiling resistance, steaming resistance and acid resistance, the invention provides a heat-sealing coating for an aluminum foil meal box, the heat-sealing coating comprises the following components in parts by mass: 40-60 parts of polyolefin dispersion; 4-8 parts of a curing agent; 15-25 parts of tackifying resin; and 10-30 parts of deionized water. The invention also provides a preparation method of the heat-sealing coating for the aluminum foil meal box. The heat-sealing coating obtained by coating the inner wall of the aluminum foil meal box with the heat-sealing coating has excellent flexibility, meets the tensile deformation capacity of the aluminum foil meal box in use, is excellent in high-temperature boiling resistance and acetic acid boiling resistance, can be subjected to heat-sealing adhesion with PP and PE laminated adhesives at 160-230 DEG C, and the meal box after heat sealing has excellent air tightness.
Owner:清远慧谷新材料技术有限公司
Low-viscosity high-tear-resistance bi-component addition type liquid silicone rubber and preparation method thereof
The preparation method comprises the following steps: putting vinyl-terminated silicone oil, fumed silica, MQ resin, enol, a fumed silica treating agent and water into a kneading machine according to a certain proportion and sequence, stirring at room temperature for 3 hours, starting vacuum stirring, heating to 120-160 DEG C, stirring at high temperature for 3 hours, and cooling to room temperature to obtain the low-viscosity high-tear-resistance double-component addition type liquid silicone rubber. After the rubber material is cooled, respectively adding a platinum catalyst to prepare a rubber A, and adding hydrogen-containing silicone oil, polyvinyl silicone oil and an inhibitor to prepare a rubber B; the method is simple in process, the prepared AB glue is low in viscosity and can be used for preparing high-hardness and high-tear silicone rubber products, the main raw materials are low-risk substances, the storage period of the prepared AB glue exceeds 12 months, and the AB glue is colorless and transparent in appearance and good in fluidity.

Owner:HUBEI XINGRUI SILICON MATERIAL CO LTD
Preparation method of anti-puncture high-barrier co-extrusion film
PendingCN111421934ASolve the tensile resistanceAddress performance requirementsSynthetic resin layered productsFlat articlesBlow moldingTear resistance
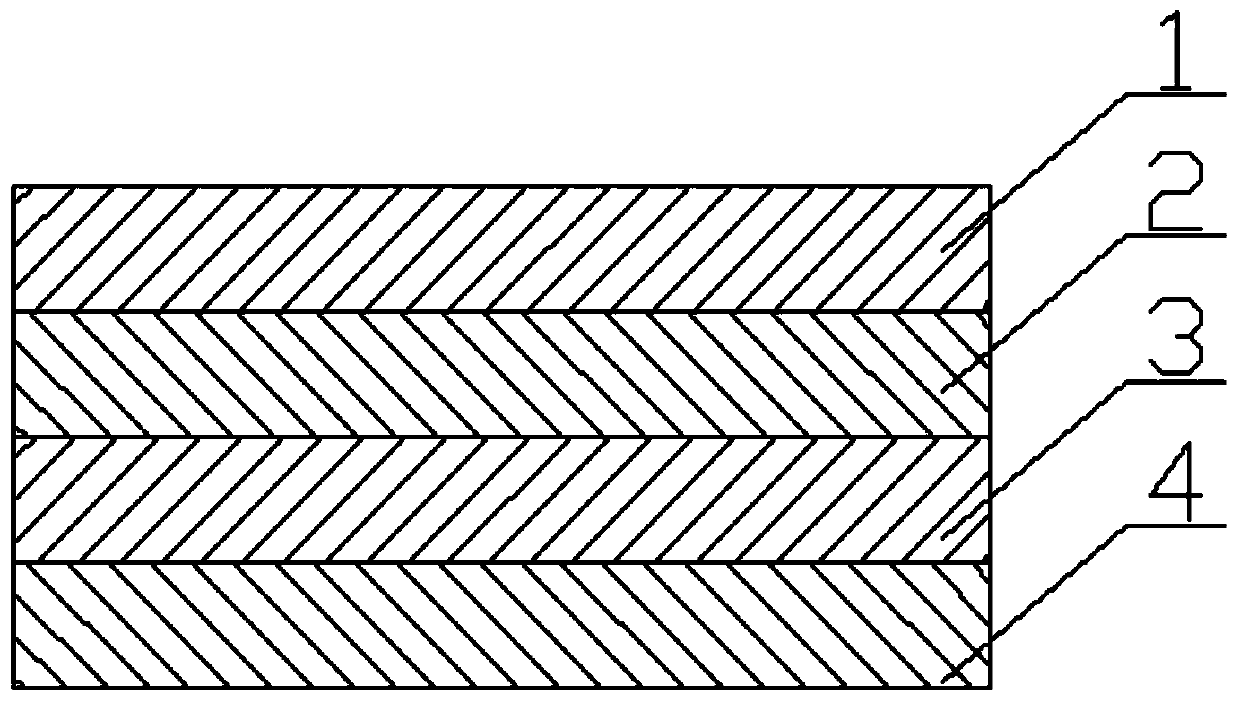
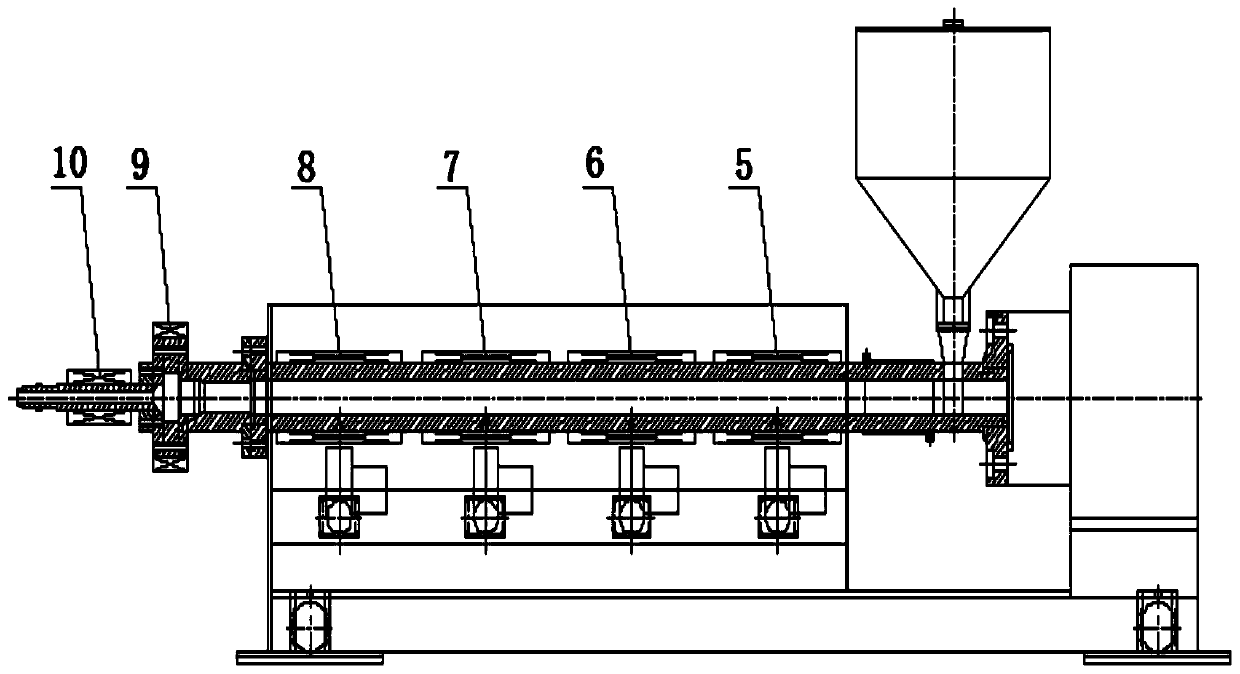
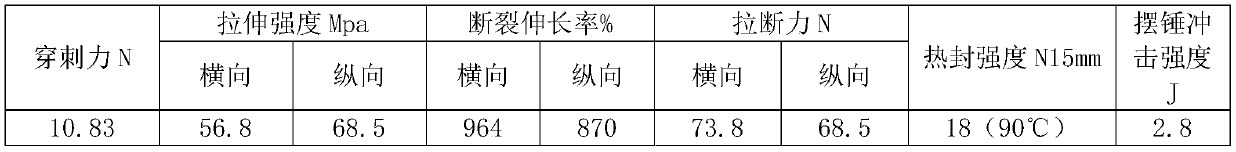
The invention provides a preparation method of a puncture-resistant high-barrier co-extrusion film, relates to the technical field of packaging materials, and solves the technical problems that a PE film and a PP film in the prior art are low in puncture resistance, poor in tensile resistance and low-temperature resistance and prone to bag breaking and poor sealing. The co-extrusion film comprisesa composite layer, a first core layer, a second core layer and a heat sealing layer, and the co-extrusion film is formed by blow molding and co-extrusion of the composite layer, the first core layer,the second core layer and the heat sealing layer which are sequentially arranged. The co-extrusion film provided by the invention integrates a series of mechanical properties such as puncture resistance, stretching resistance, impact resistance, tear resistance and the like, and in addition, on the premise of ensuring the mechanical properties, the processability of a product and the use performance of a client need to be met at the same time.
Owner:DALIAN JUTONG PLASTIC PRODS
Antifouling alloy, method for producing the same, and antifouling sheet produced from the same
The application relates to a scale-inhibiting alloy and a preparation method thereof and a scale-inhibiting sheet manufactured from the scale-inhibiting alloy. The scale-inhibiting alloy comprises the following components: 55wt%-70wt% of Cu, 15wt%-30wt% of Zn, 5wt%-15wt% of Ni, 0.5wt%-3wt% of Si, 1wt%-5wt% of P, 0.001wt%-0.05wt% of a modifying element, and the balance of inevitable impurities, wherein the modifying element is one or more of B, Ti and Zr. The scale-inhibiting alloy adds the Si element for strengthening, so as to improve the mechanical properties and corrosion resistance; the Zn element is added as a negative electrode and the P element is added as a positive electrode, the alloying forms alpha phase+beta phase+multi-element brittle compound phase, can well excite the active current, and prevents the generation of water scale. The scale-inhibiting alloy has low production cost, meets the comprehensive requirements of cost, processing performance, corrosion resistance, mechanical properties, health and market acceptance of water treatment products, and has a good application prospect.

Owner:JOMOO KITCHEN & BATHROOM
Round billet continuous casting and rolling micro-alloying steel for shield tunneling machine cutter hub and manufacturing method of round billet continuous casting and rolling micro-alloying steel
PendingCN119615012Ahigh strengthImprove toughnessProcess efficiency improvementMetal rolling arrangementsProduct inspectionMetallurgy
The invention relates to steel for a microalloying shield tunneling machine cutter hub. The steel comprises the following chemical components in percentage by mass: 0.25 to 0.45 percent of C, 0.05 to 0.37 percent of Si, 0.40 to 1.00 percent of Mn, 1.00 to 1.80 percent of Cr, 0.05 to 0.50 percent of Ni, 0.10 to 0.35 percent of Mo, 0.0010 to 0.0030 percent of B, 0.010 to 0.050 percent of Al, less than or equal to 0.015 percent of P, less than or equal to 0.010 percent of S, less than or equal to 0.15 percent of Cu, 0.010 to 0.040 percent of Ti, less than or equal to 0.030 percent of Nb, less than or equal to 0.00050 percent of Ca, less than or equal to 0.040 percent of As, less than or equal to 0.030 percent of Sn, less than or equal to 0.0050 percent of Sb, less than or equal to The manufacturing process comprises the steps of full molten iron treatment, BOF converter treatment, LF refining furnace treatment, RH vacuum degassing, CCM round billet continuous casting (the size of phi 700 mm or above), warm feeding / slow cooling, heating rolling (round steel with the diameter of phi 200 mm or above), saw cutting, slow cooling, flaw detection, finished product inspection and packaging. According to the steel for the shield tunneling machine cutter hub, round billets with the specification of phi 700 mm or above are rolled into bar round steel, and the macroscopic quality, the mechanical property, the impact quality and the internal quality of the steel for the shield tunneling machine cutter hub are guaranteed.

Owner:JIANGYIN XINGCHENG SPECIAL STEEL WORKS CO LTD
Low-temperature curing color coiled material paint and method for preparing same
ActiveCN101531860BSuitable for continuous roller coatingMeet the hardness and toughnessPolyester coatingsLow temperature curingSolvent
Owner:JIANGSU LANLING POLYMER MATERIAL CO LTD
High temperature sterilized eye drop applicator
The invention provides an eyedrops container which is easy to manufacture and easy to sterilize, ensures a sterile guarantee, and moreover is excellent in instilling operability, the eyedrops container is integrally formed of a resin material that does not melt or deform in time of sterilization performed under a condition of approximately 121 DEG C, for approximately 20 minutes.
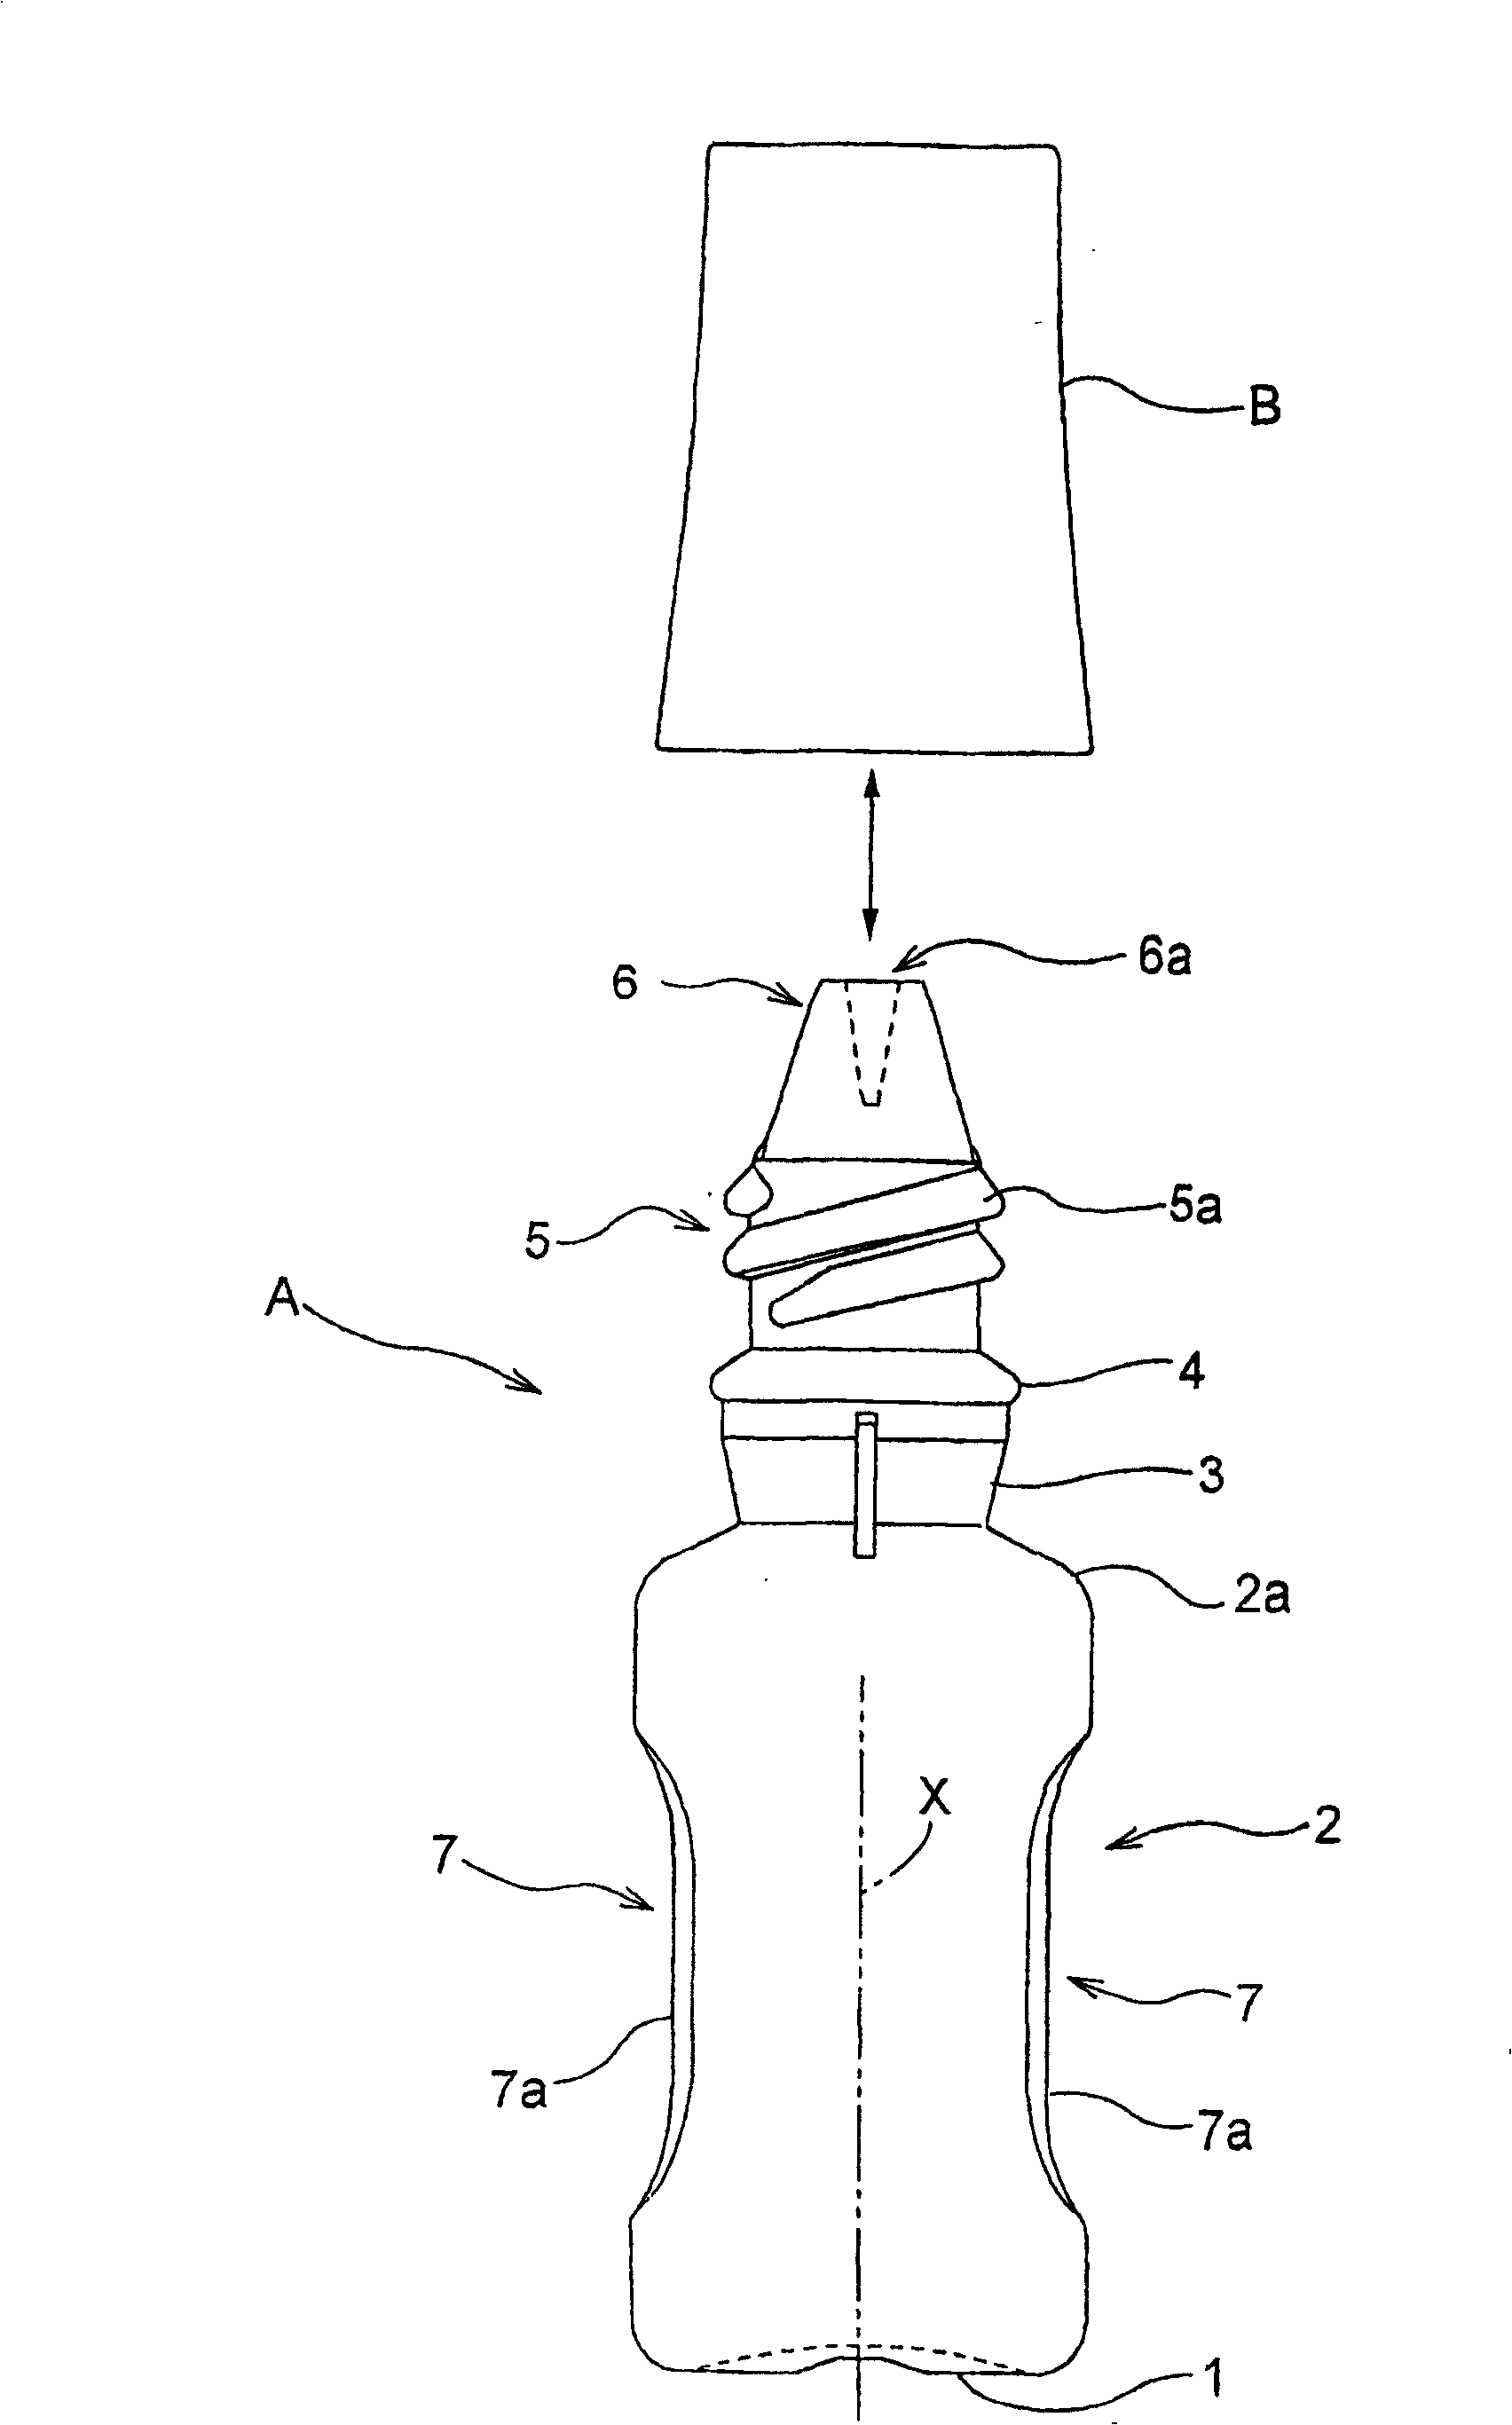
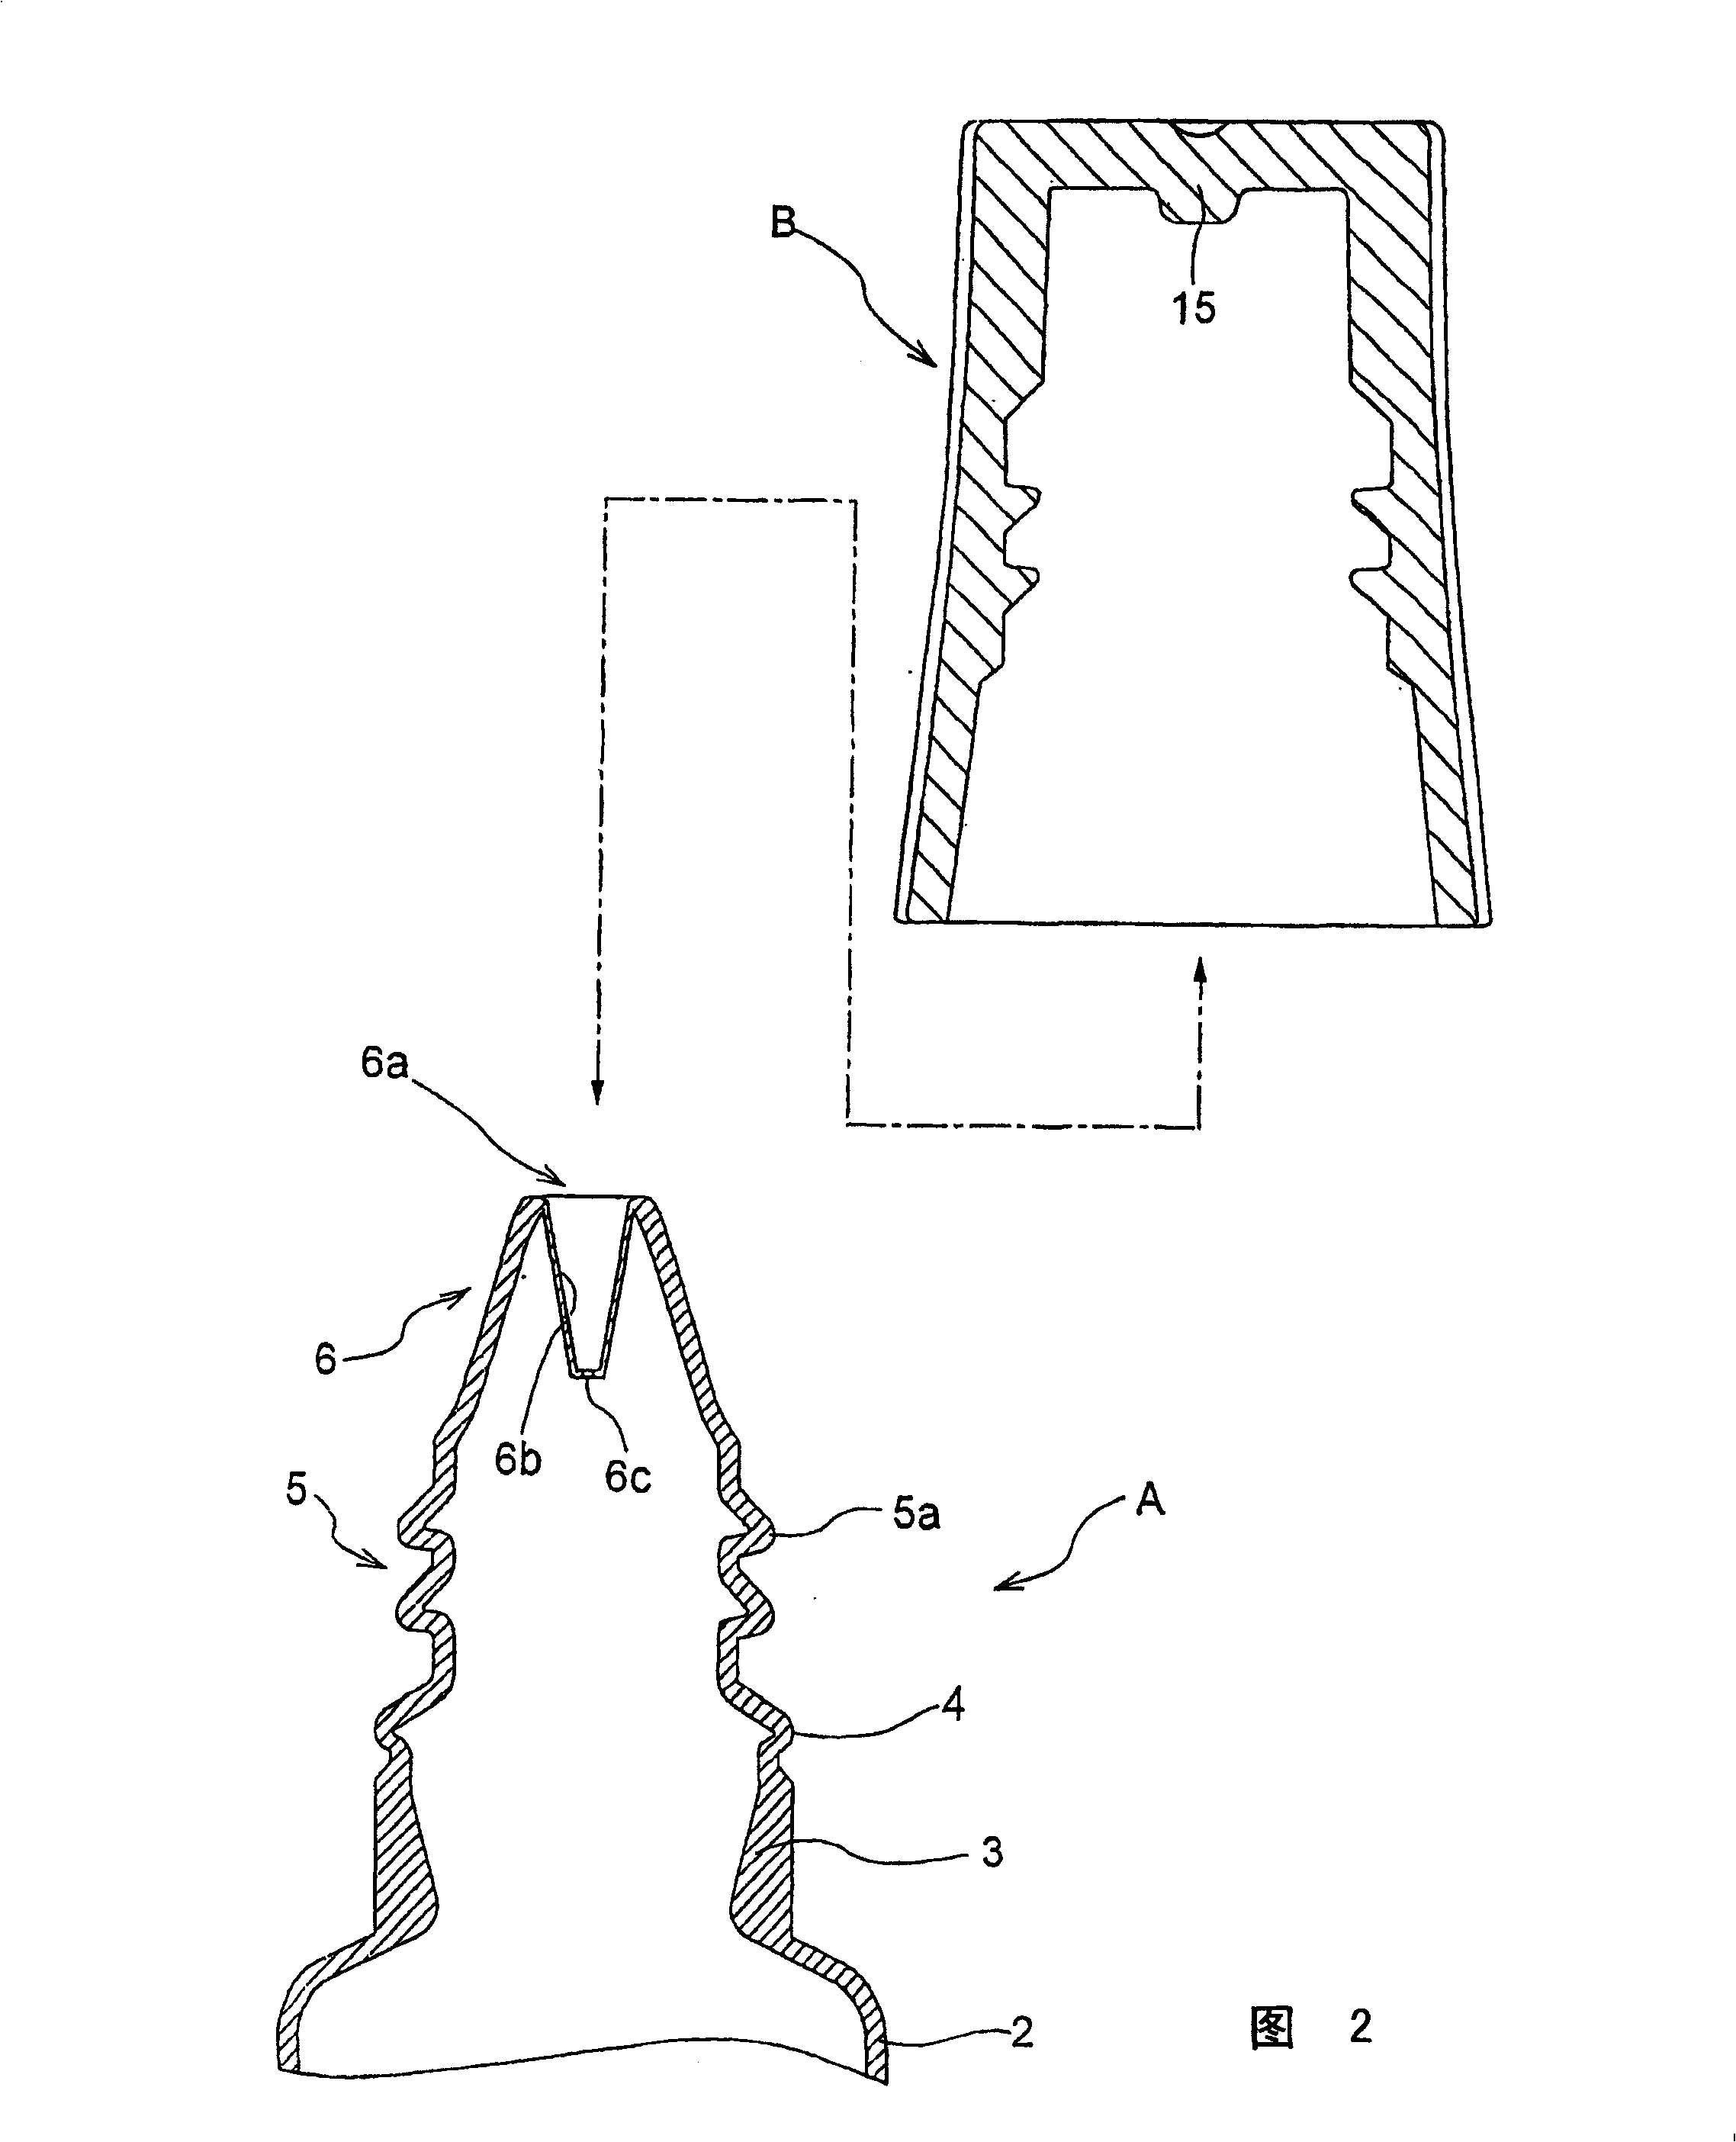
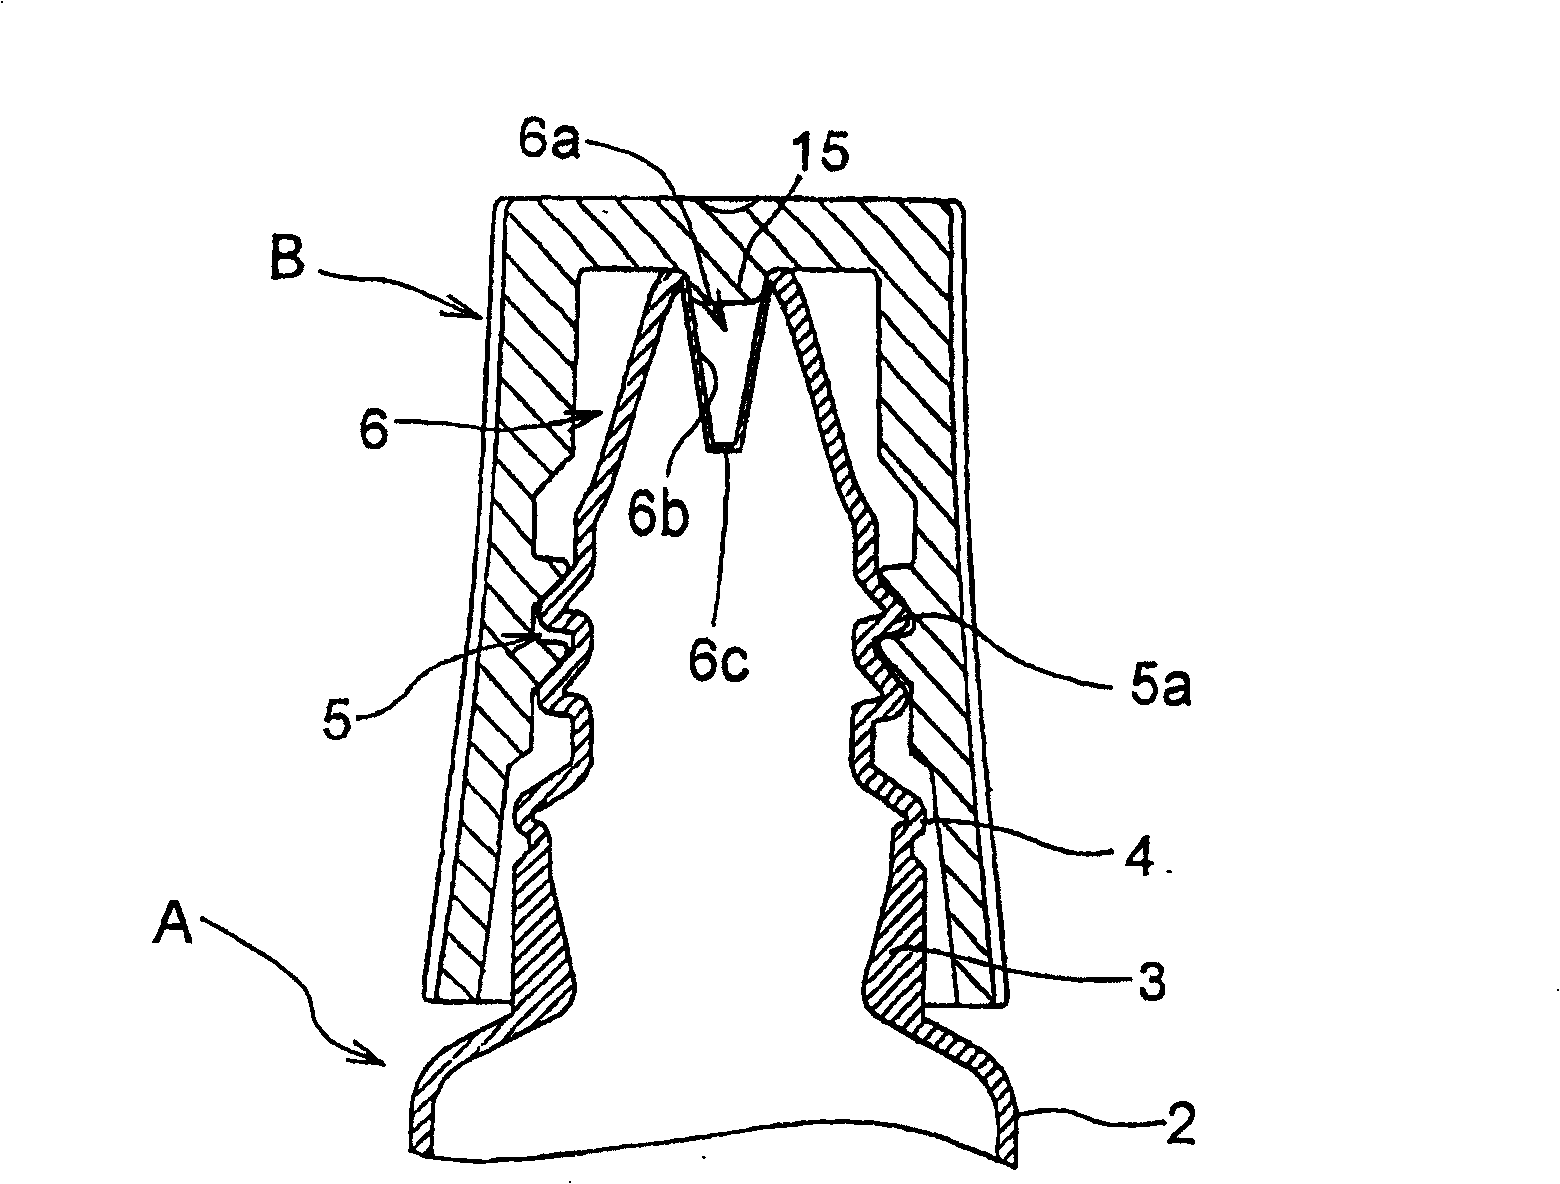
Owner:SANTEN PHARMA CO LTD
Magnetic current changing polishing device for large caliber aspheric surface optical part
InactiveCN100566935CProcessing size is not limitedEasy to set upGrinding carriagesOptical surface grinding machinesMagnetic currentControl system
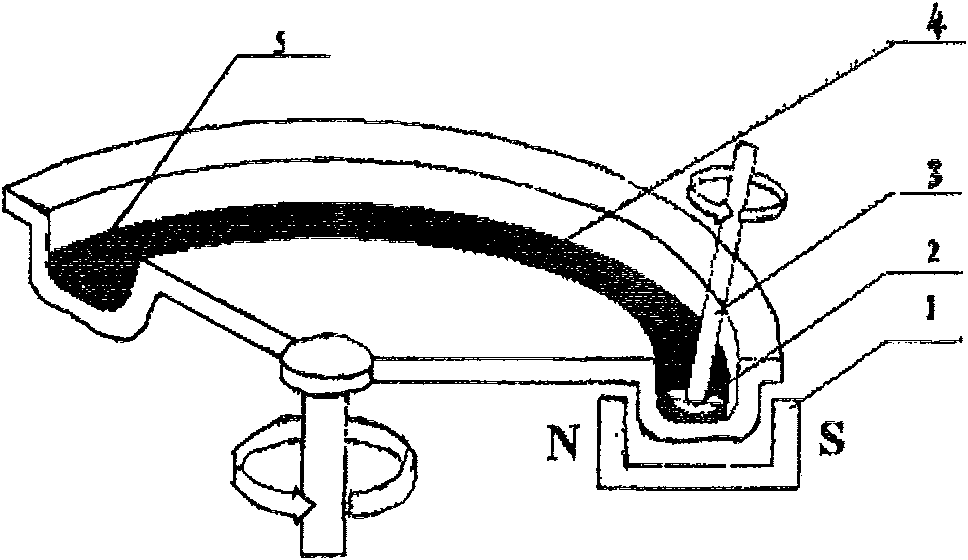
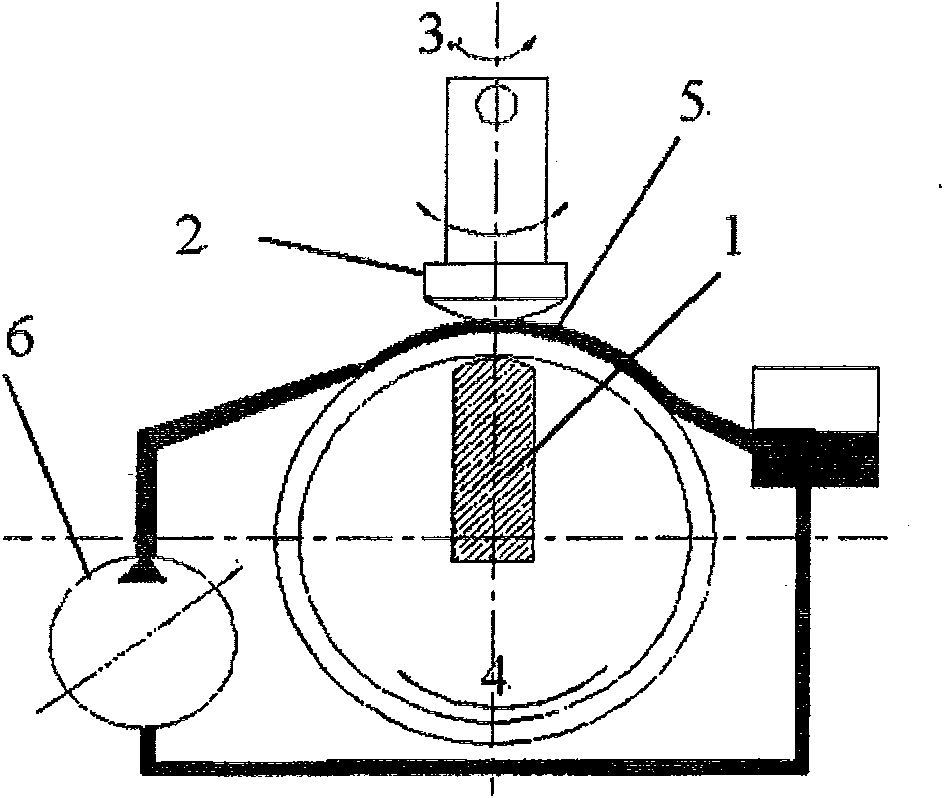
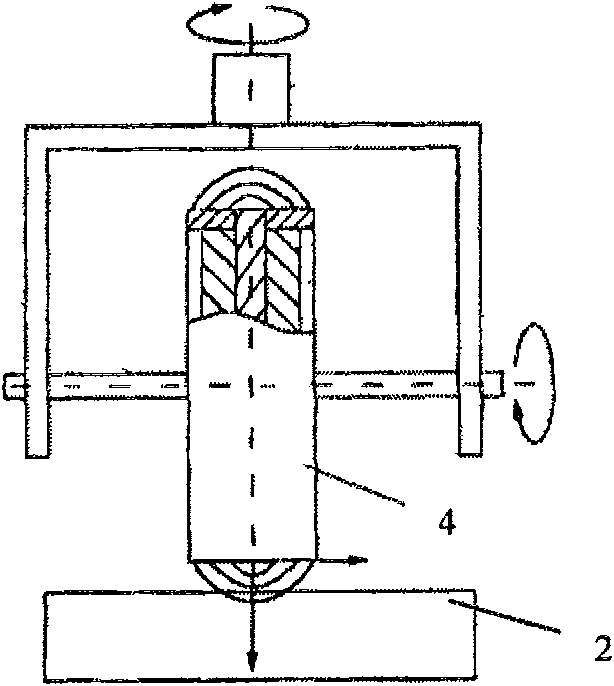
Owner:NAT UNIV OF DEFENSE TECH
A bake-hardening high-strength steel and its manufacturing method
The invention discloses bake hardening type high-strength steel. The bake hardening type high-strength steel comprises, by mass percentage, 0.05 to 0.13% of C, 0.05 to 0.20% of Si, 0.50 to 1.50% of Mn, 0.02 to 0.06% of Al, larger than 0 and not larger than 0.0050% of N, and the balance iron and other inevitable impurities, and in addition, the condition that B-0.77*N is larger than or equal to 0.0005 and smaller than or equal to 0.0020% should be met. According to the bake hardening type high-strength steel, under the condition of not adding precious metals such as Mo, Cr, Ti and Nb, by controlling the mass percentage of carbon, manganese and boron, the technological processes and the technological parameters, the steel which is high in strength, low in cost, high in surface quality and of which the machining performance meets the requirements of automotive parts is manufactured.

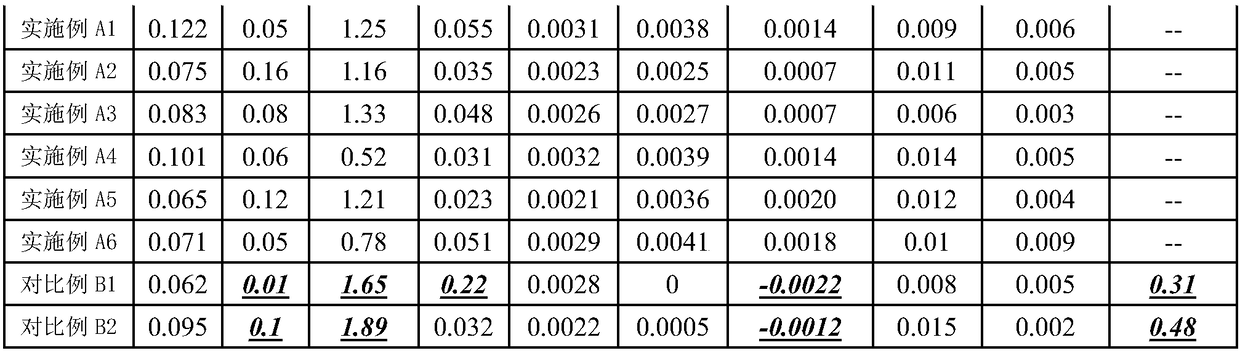
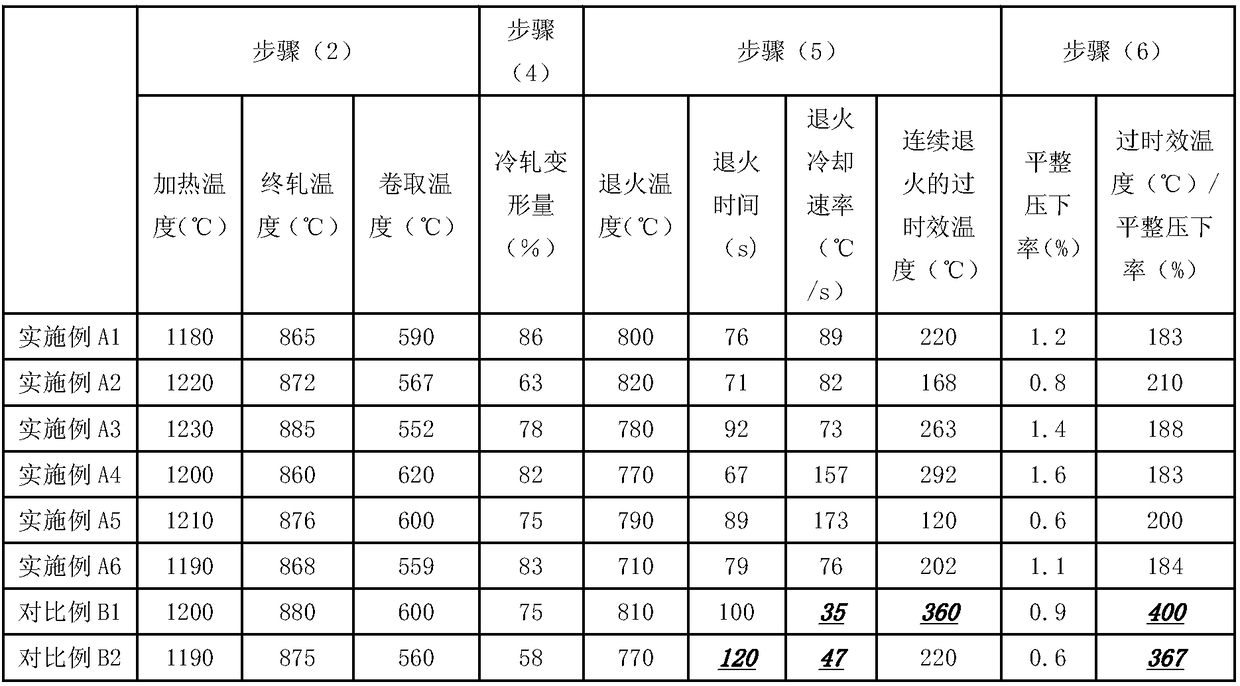
Owner:BAOSHAN IRON & STEEL CO LTD
Aluminum-plated ternary copolymerized polypropylene casting film resin composition
InactiveCN109721856AMeet the processing performanceMeet the optical performanceHalogenOptical property
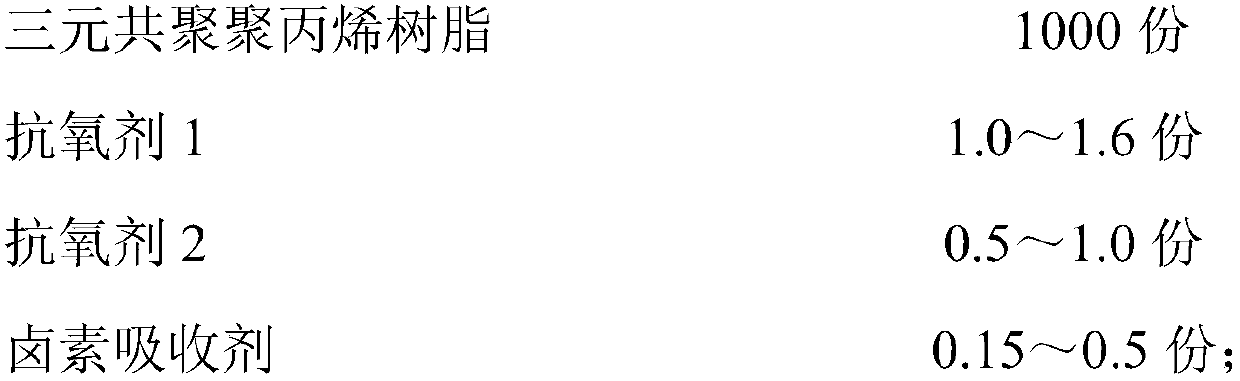
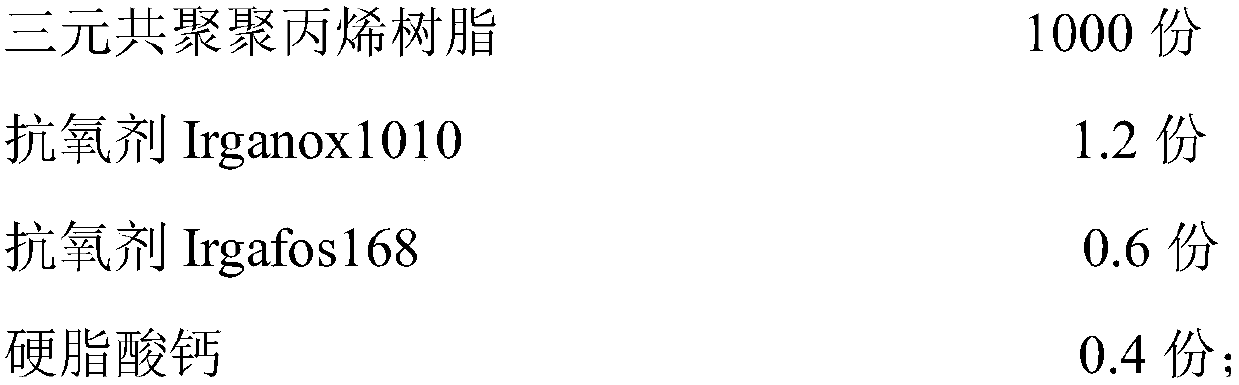
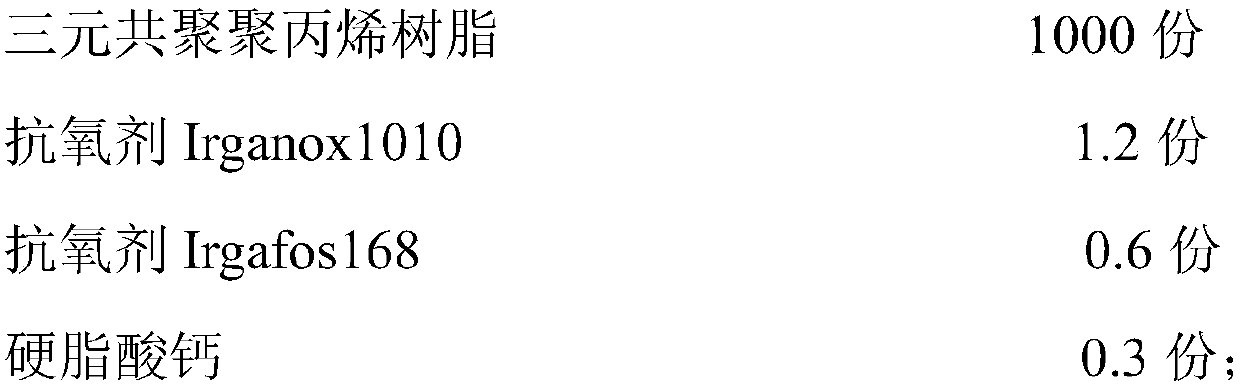
The invention relates to an aluminum-plated ternary copolymerized polypropylene casting film resin composition, which comprises the following raw materials by weight: 1000 parts of a ternary copolymerized polypropylene resin, 1.0-1.6 parts of an antioxidant 1, 0.5-1.0 part of an antioxidant 2, and 0.15-0.5 part of a halogen absorbent, wherein the ternary copolymerized polypropylene resin comprises5.5-10 wt% of 1-butene, 0.5-1.5 wt% of ethylene, and the balance of propylene. According to the present invention, the ternary copolymerized polypropylene composition has characteristics of excellentimpact strength, excellent rigidity and low n-hexane extract under the premise of meeting of the processing property, the aluminum plating property, the optical property and the thermal adhesive property of food-grade aluminum-plated films, and can completely meet the production requirements of high-end casting film packaging manufacturers on metalize cast polypropylene.
Owner:CHINA PETROLEUM & CHEM CORP +1
Ultra-thin small-caliber high-resolution endoscopic microscope objective
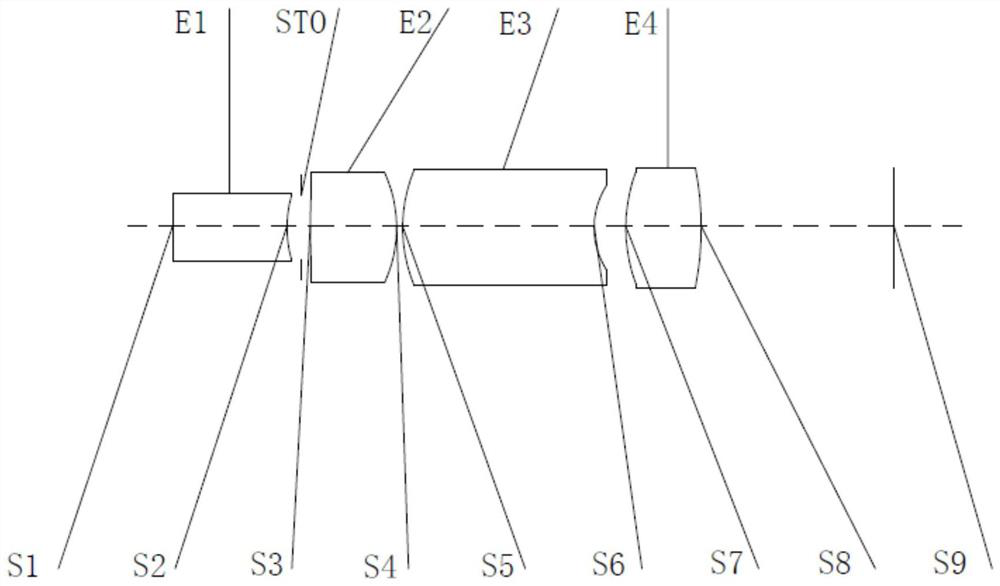
The invention relates to an ultra-thin small-caliber high-resolution endoscopic microscope objective which comprises a first lens, a diaphragm, a second lens, a third lens and a fourth lens sequentially arranged from the object side. All the lenses are spherical lenses and are separately arranged by taking air as an interval, the first lens has negative focal power, the object side surface of the first lens is a plane, and the image side surface of the first lens is a concave surface; the second lens has positive focal power, the object side surface of the second lens is a convex surface, and the image side surface is a convex surface;the third lens has positive focal power, the object side surface of the third lens is a convex surface, and the image side surface of the third lens is a concave surface; the fourth lens has positive focal power, the object side surface of the fourth lens is a convex surface, the image side surface of the fourth lens is a convex surface, the maximum clear aperture is less than or equal to 0.6, the axial distance from the object side surface of the first lens to the imaging surface is less than or equal to 4.0 mm, and 1.1< f*TAN(HFOV) / T34< 2.3. The endoscopic microscope objective is small in caliber, small in thickness, high in resolution, compact in structure, convenient to machine and install and good in imaging quality, and the requirements for miniaturization and light weight of the medical endoscopic microscope objective are met.
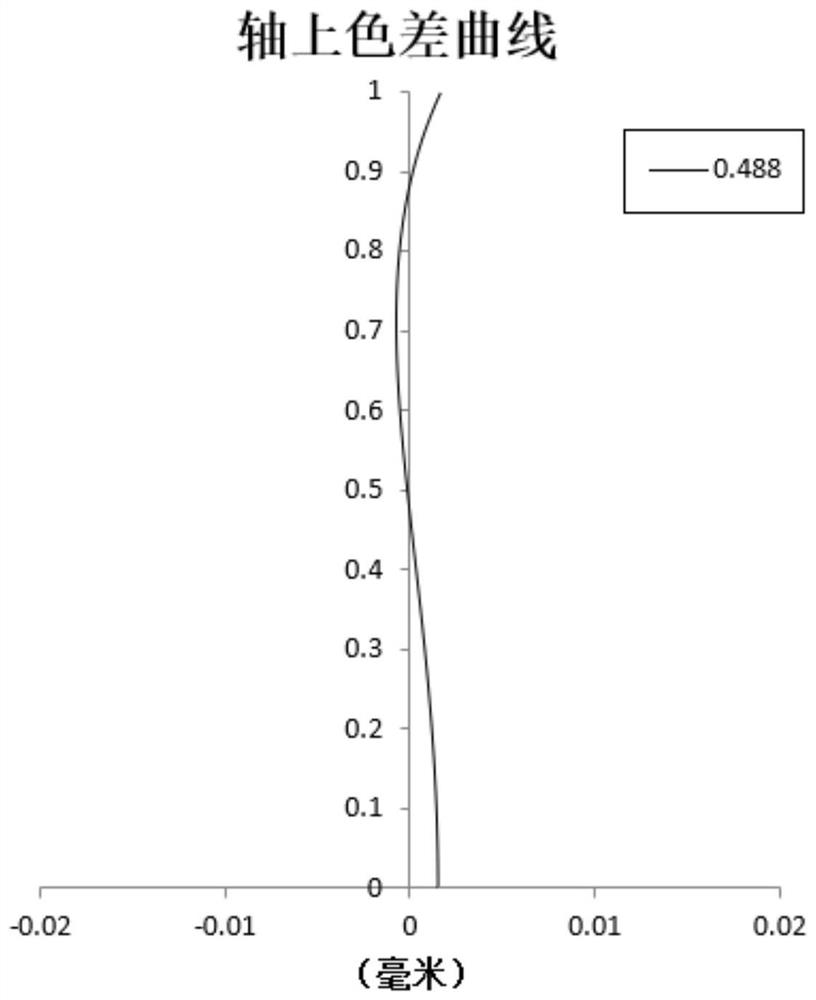
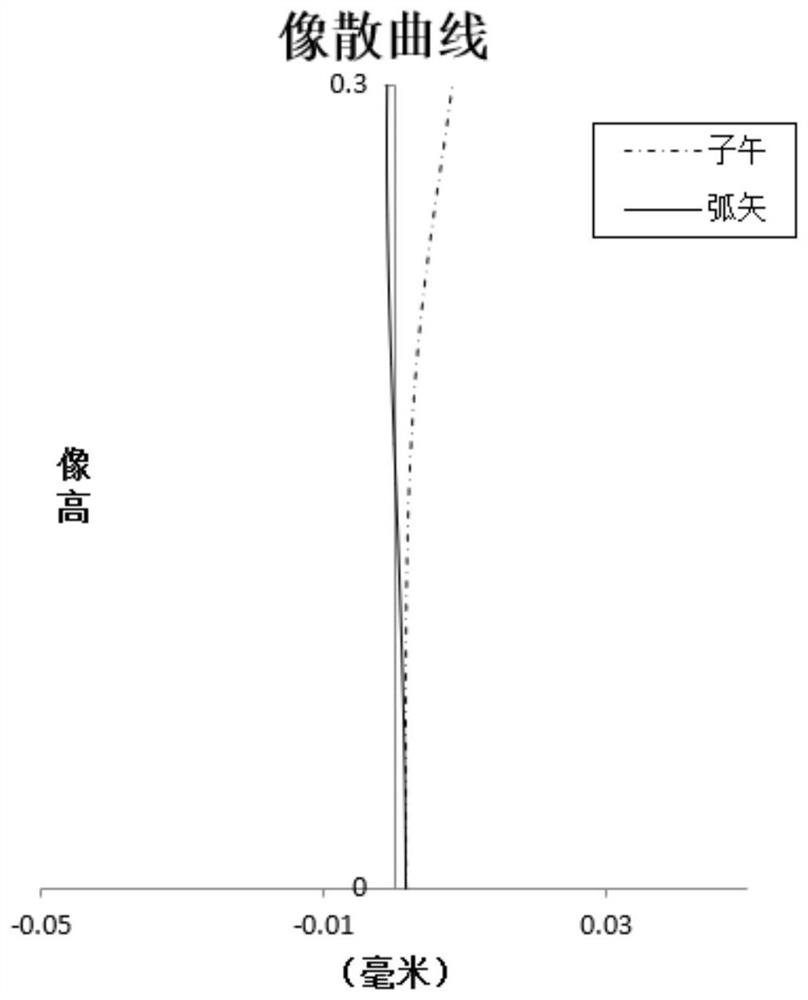
Owner:ZHEJIANG LAB +1
A kind of tension control method for fair drawing and straightening of deep-drawn galvanized steel sheet
ActiveCN103934282BImprove surface qualityGuaranteed surface qualityTension/compression control deviceSheet steelEconomic benefits
The invention belongs to the technical field of galvanized steel sheet production methods, and relates to a finishing withdrawing-straightening tension control method for a deep-draw galvanized steel sheet for guaranteeing the steel sheet performance and the surface quality. According to the technical scheme, the tension set values before and after the finishing withdrawing-straightening are adjusted, and the matching relation between steel plates with different thicknesses and the tension before and after the finishing withdrawing-straightening is adopted, wherein the tension before finishing conforms to the formula: T(strip steel thickness)*(25-30)KN, and the tension after finishing and withdrawing-straightening conforms to the formula: T(strip steel thickness)*(27.5-33)KN. According to the finishing withdrawing-straightening tension control method, the surface quality of the deep-draw galvanized product can be guaranteed, the performance is not greatly affected, the requirement for machining and using performance of a user is met, and the performance aggravating effect brought by increasing the finishing rolling force to guarantee the surface of the deep-draw galvanized product is avoided. The performance judgment amending ratio of the deep-draw galvanized product is greatly reduced, the surface quality and the profit space of the deep-draw galvanized product are greatly improved, the competitiveness of enterprises is enhanced, and considerable economic benefits are brought to the enterprises.
Owner:HEBEI IRON AND STEEL
Method for preparing ternary copolymerized metalize cast polypropylene resin composition
InactiveCN109721808AMeet the processing performanceMeet the optical performancePolymer scienceOptical property
The invention relates to a method for preparing a ternary copolymerized metalize cast polypropylene resin composition, comprising the steps of: 1) preparing a ternary copolymerized polypropylene resinbinder: using propylene as a main reaction material, 1-butylene and ethylene as comonomers to carry out copolymerization reaction in a loop reactor to obtain the ternary copolymerized polypropylene resin binder; 2) mixing the ternary copolymerized polypropylene resin binder prepared in the step 1, an antioxidant 1, an antioxidant 2, and a halogen absorber at ambient temperature and pressure, andthen adding the mixture to a twin-screw extruder for granulation to obtain the ternary copolymerized metalize cast polypropylene resin composition. The ternary copolymerized metalize cast polypropylene resin composition of the invention satisfies the processing property, aluminum plating property, optical property and thermal adhesive property for a food grade aluminized film, and also has excellent impact strength, rigidity and low hexane extract content. The resin composition fully meets the requirements of high-end cast film packaging manufacturers for producing aluminized cast films.
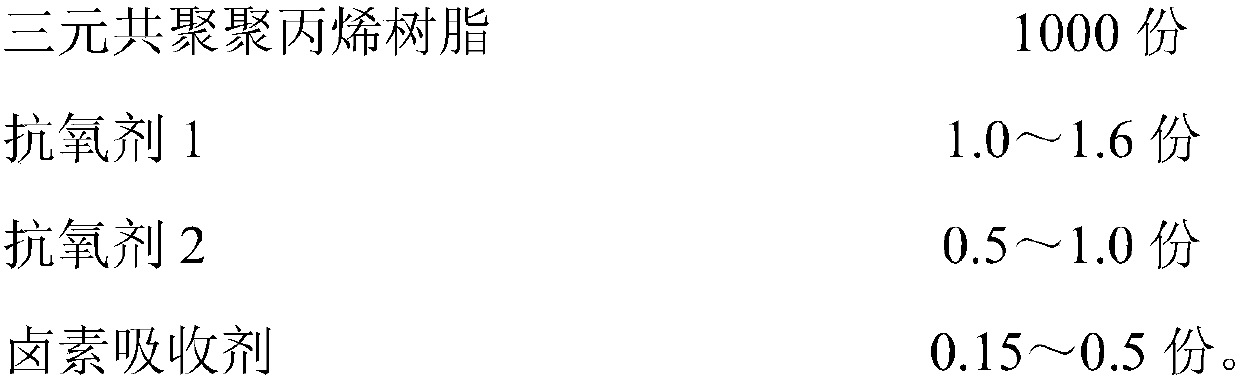
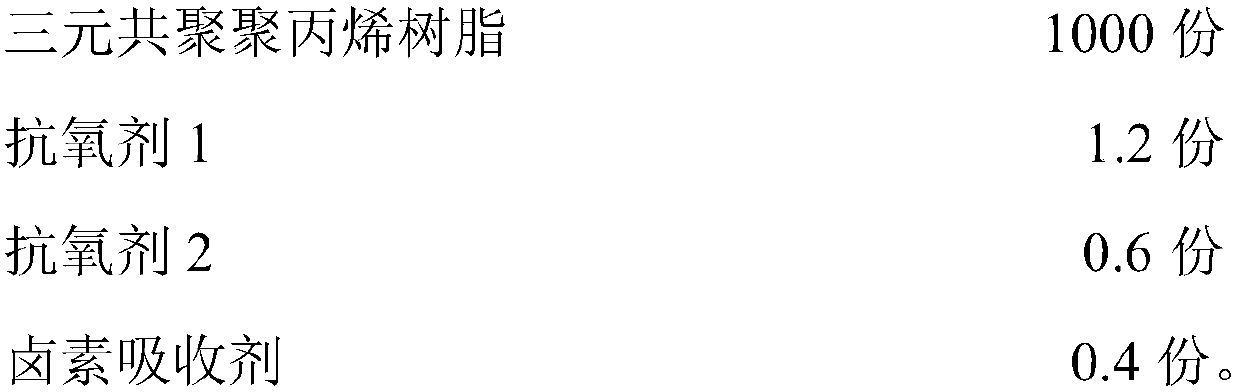

Owner:CHINA PETROLEUM & CHEM CORP +1
Vacuum brazing welding piece blank material and preparation method thereof
InactiveCN111451667ANo holesReduce consumptionWelding/cutting media/materialsSoldering mediaMaterial consumptionIngot
The invention discloses a vacuum brazing welding piece blank material and a preparation method thereof. The preparation method comprises the following steps that raw materials are prepared, and the raw materials comprise an aluminium ingot, waste aluminum and aluminum-silicon intermediate alloy; the raw materials are added into a smelting furnace and are ignited to be melted; after the raw materials are completely liquefied into aluminum water, silicon content blending is firstly performed, then the aluminum water is guided into a standing furnace to perform magnesium content blending, after the two-time ingredient blending, the silicon content is not more than 9.0%, and the magnesium content is not more than 0.35%; and cast rolling is performed to obtain cast rolling rolls, namely the vacuum brazing welding piece blank material. According to the vacuum brazing welding piece blank material and the preparation method thereof provided by the invention, the production cycle is short, material consumption is low, and the blank material has no holes, is not prone to breaking and is easy to roll.
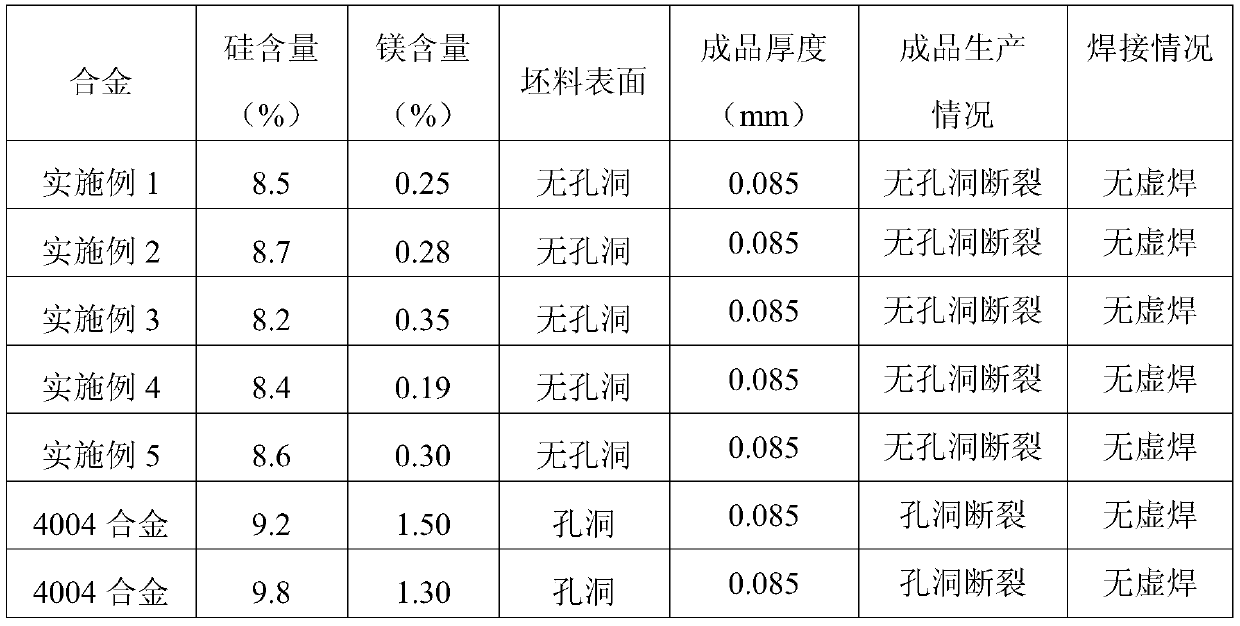
Owner:JIANGSU DINGSHENG NEW MATERIAL JOINT STOCK CO LTD
An ultra-thin small-aperture high-resolution endoscopic microscope objective lens
The invention relates to an ultra-thin small-caliber high-resolution endoscopic microscope objective lens, which comprises a first lens, a diaphragm, a second lens, a third lens and a fourth lens arranged in sequence from the object side, and each lens is a spherical lens And they are all separated by air. The first lens has a negative refractive power, its object side is a plane, and its image side is concave; the second lens has a positive refractive power, its object side is a convex surface, and its image side is a convex surface; The lens has positive refractive power, the object side is convex, and the image side is concave; the fourth lens has positive refractive power, the object side is convex, the image side is convex and the maximum light aperture is ≤0.6, the first lens object side to imaging The axial distance of the surface ≤ 4.0mm, and meet 1.1
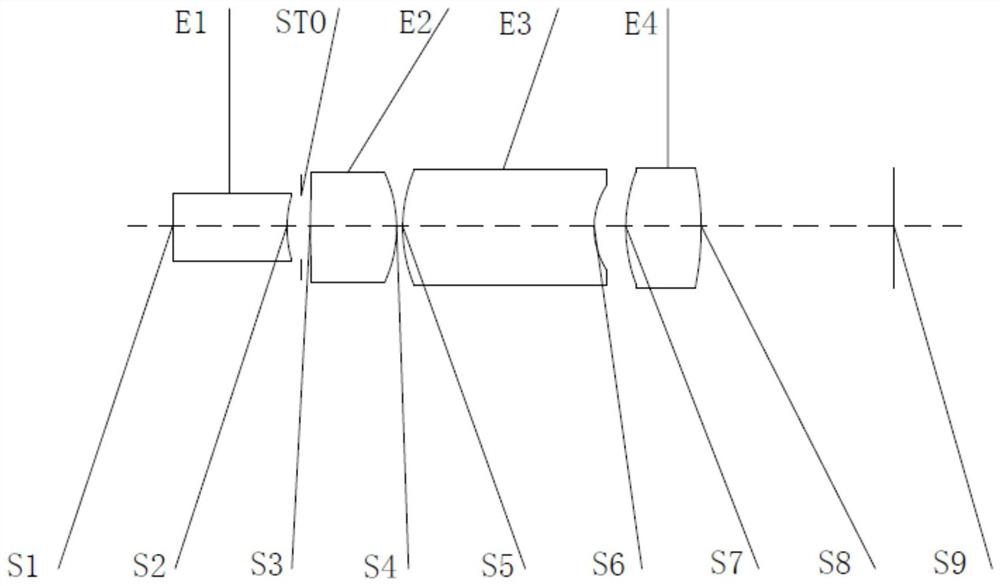
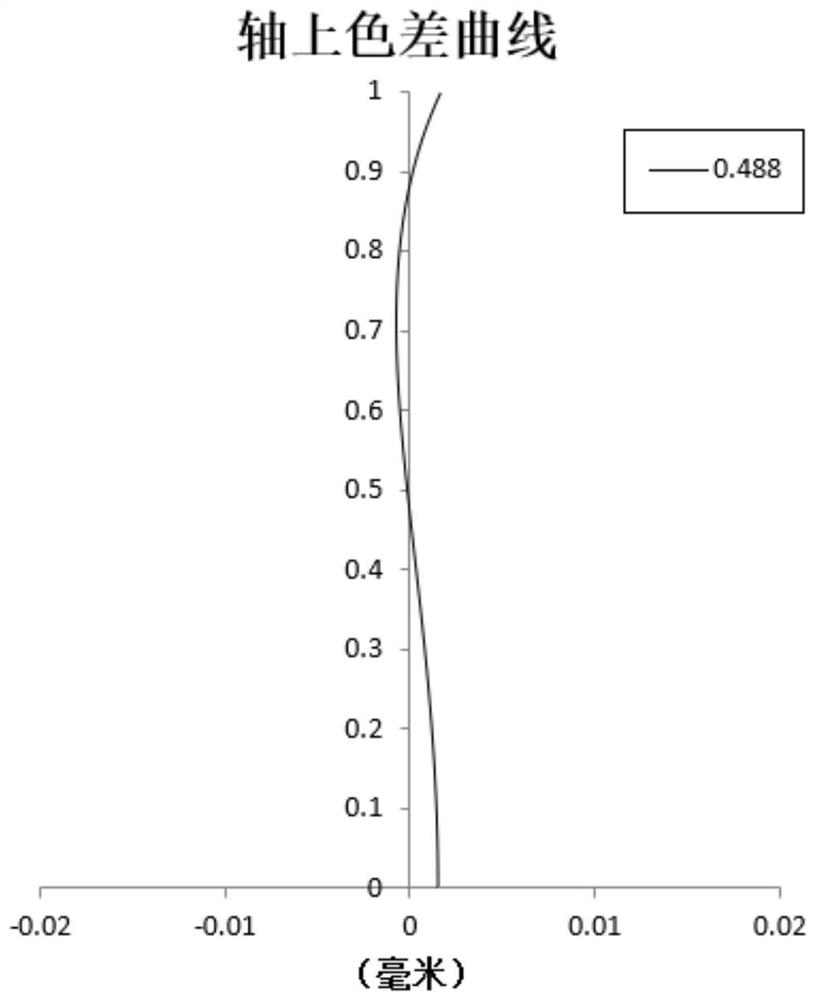
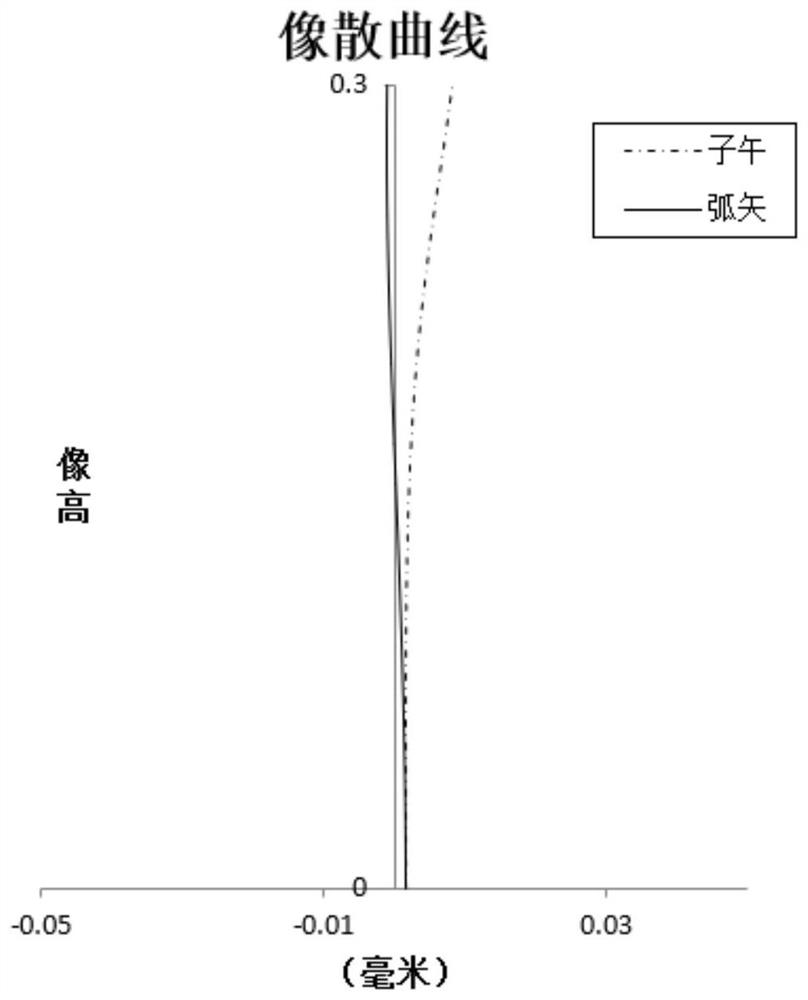
Owner:ZHEJIANG LAB +1
Preparation method and application of MXene-based inorganic particle/PVDF-based polymer composite diaphragm
ActiveCN114865226AImprove performanceInhibit growthMaterial nanotechnologyLi-accumulatorsPolymer scienceSpinning
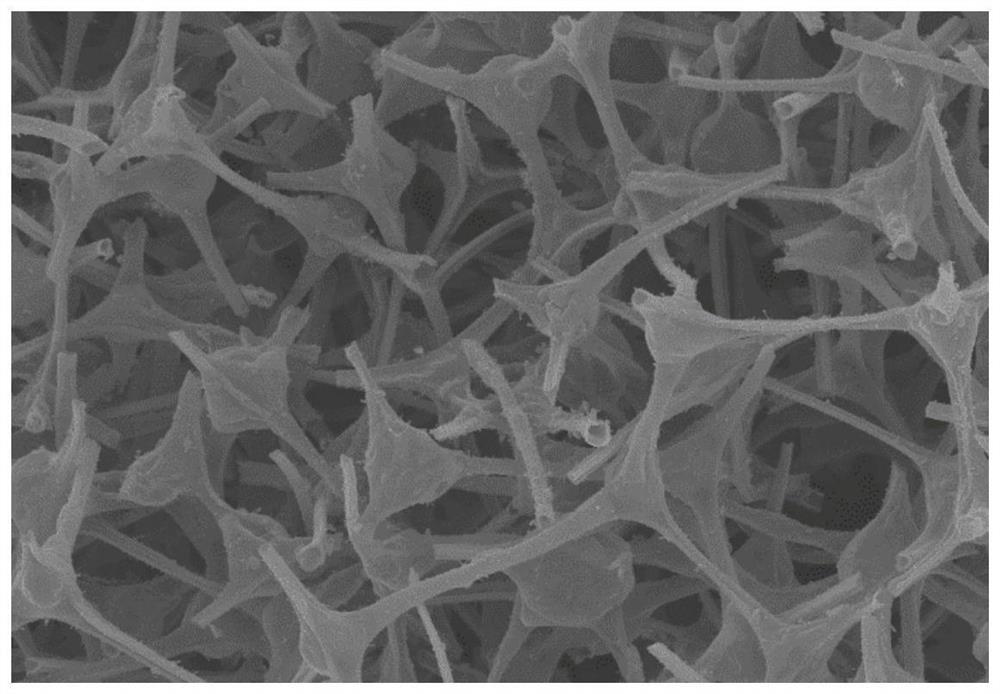
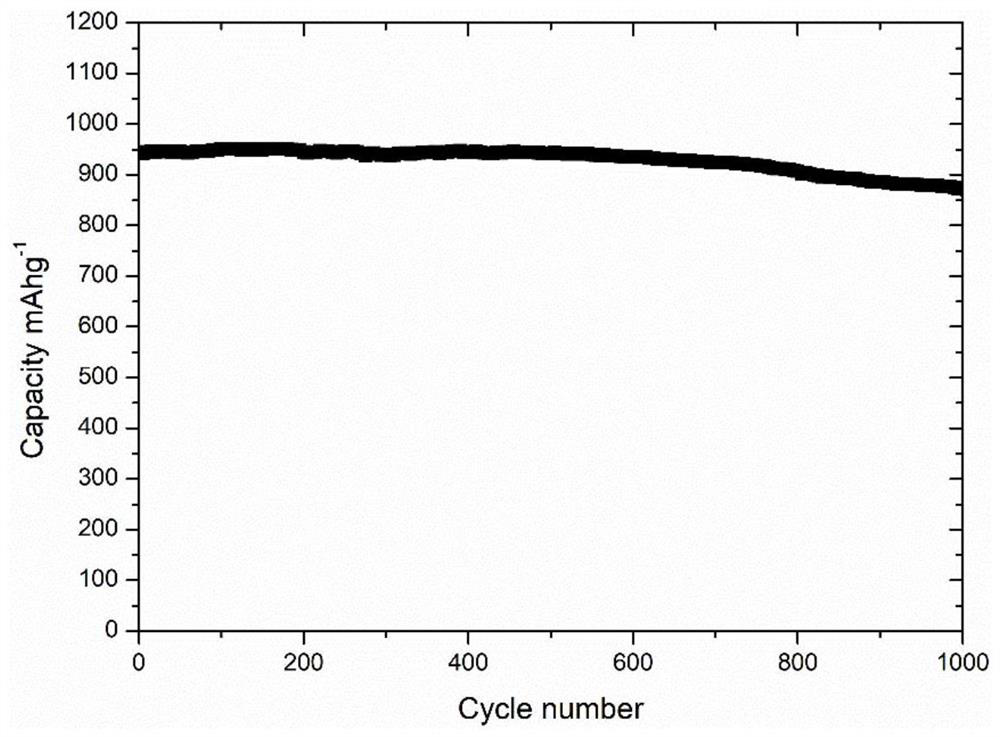
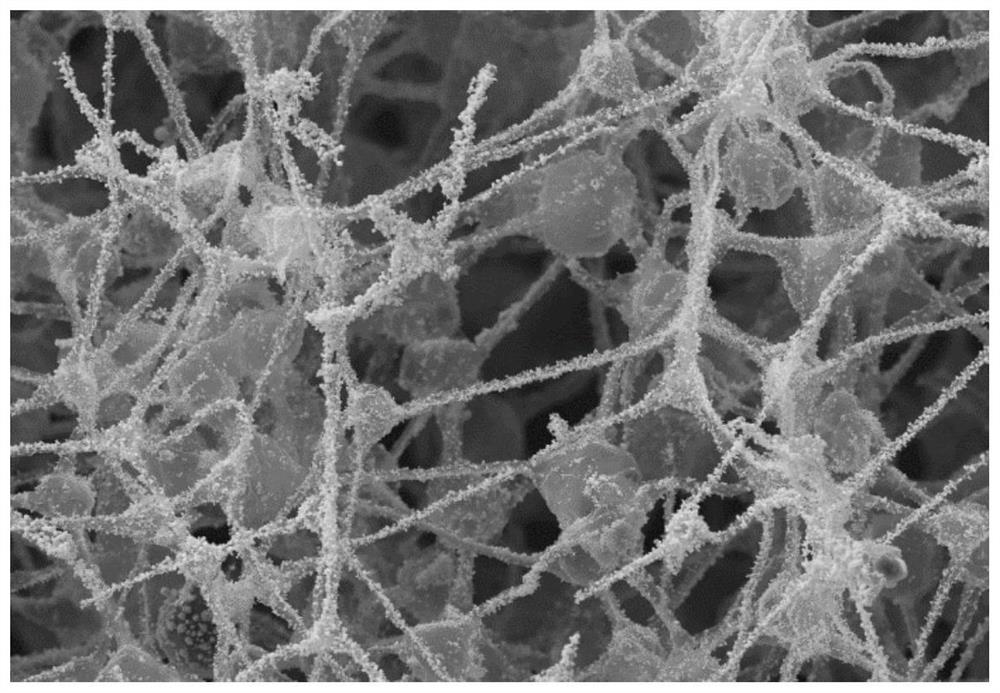
The invention discloses a preparation method of an MXene-based inorganic particle / PVDF (Polyvinylidene Fluoride)-based polymer composite diaphragm and application of the diaphragm, and relates to a polymer-inorganic composite diaphragm and application. The invention aims to solve the problems of shuttle effect of lithium polysulfide and lithium dendrites. The preparation method comprises the following steps: dissolving a polyvinylidene fluoride-styrene sulfonic acid copolymer in a nitrogen methyl pyrrolidone solution, stirring and adding a certain amount of inorganic matters to obtain a spinning solution; injecting the spinning solution into electrostatic spinning equipment for spinning, and then drying to obtain a polymer composite diaphragm with the thickness of 30-120 microns; an organic-inorganic composite membrane is constructed by utilizing an electrostatic spinning technology, so that the comprehensive performance of the Li-S battery is improved. The space steric hindrance effect of a PVDF-based polymer diaphragm frame and the high-active oxygen vacancy synergistic inhibition shuttle effect of inorganic particles are utilized, and meanwhile, the two-dimensional nanosheet structure of the inorganic particles is utilized to shield large-size pores existing in an electrostatic spinning membrane, so that the mechanical strength of the diaphragm is improved, and the growth of negative electrode lithium dendrites is prevented.
Owner:宁波民光新材料有限公司
A kind of production method of glass fiber SMC yarn
The invention discloses a production method of glass fiber SMC yarn, which comprises the following steps: 1) preparation of an impregnating agent; 2) dosing; 3) melting in a kiln; 4) bushing; 5) coating with the impregnating agent; 6) drawing; 7) drying; 8) roving winding; 9) inspection and storage. According to the method disclosed by the invention, by adopting the complete-performance glass component and the special impregnating agent, the need of the drawing operation is met in the drawing technology while the processability of a later unwinding process is also guaranteed, thus the glass fiber SMC yarn has good acid resistance and water resistance, relatively high strength and good electric properties and mechanical properties.
Owner:JIANGSU ZHONGYA NEW MATERIAL